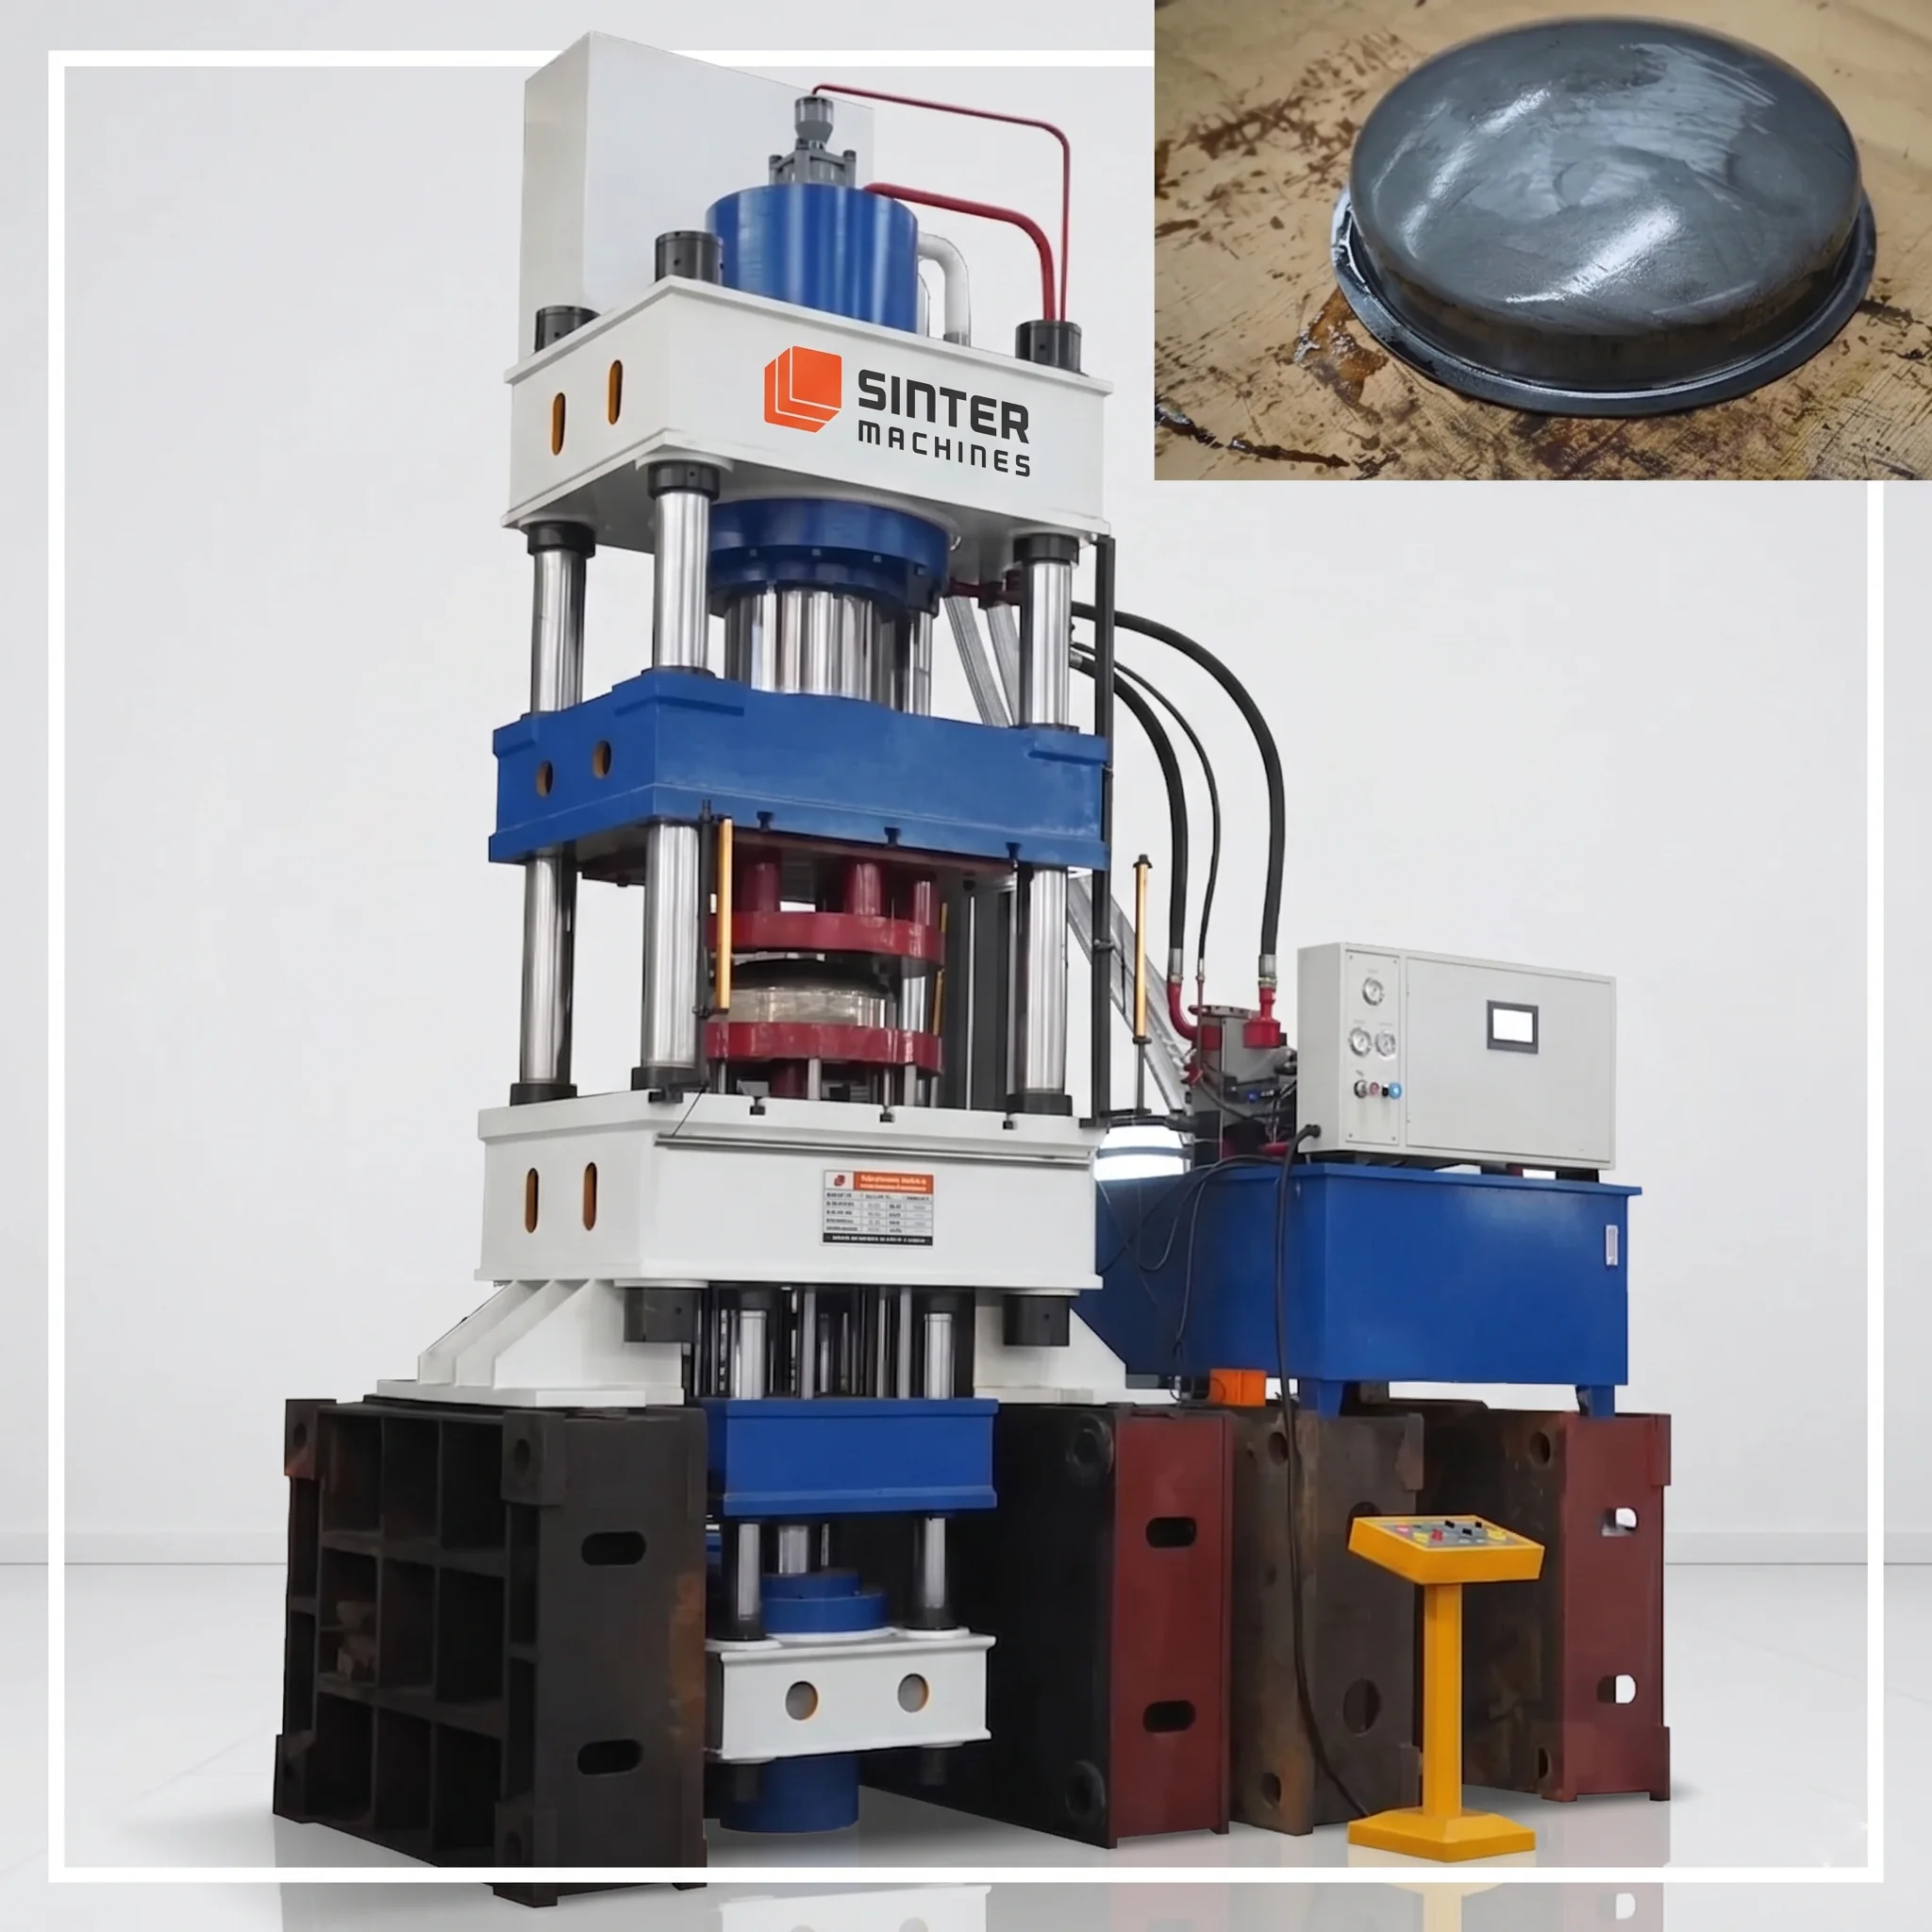
01 — Press System
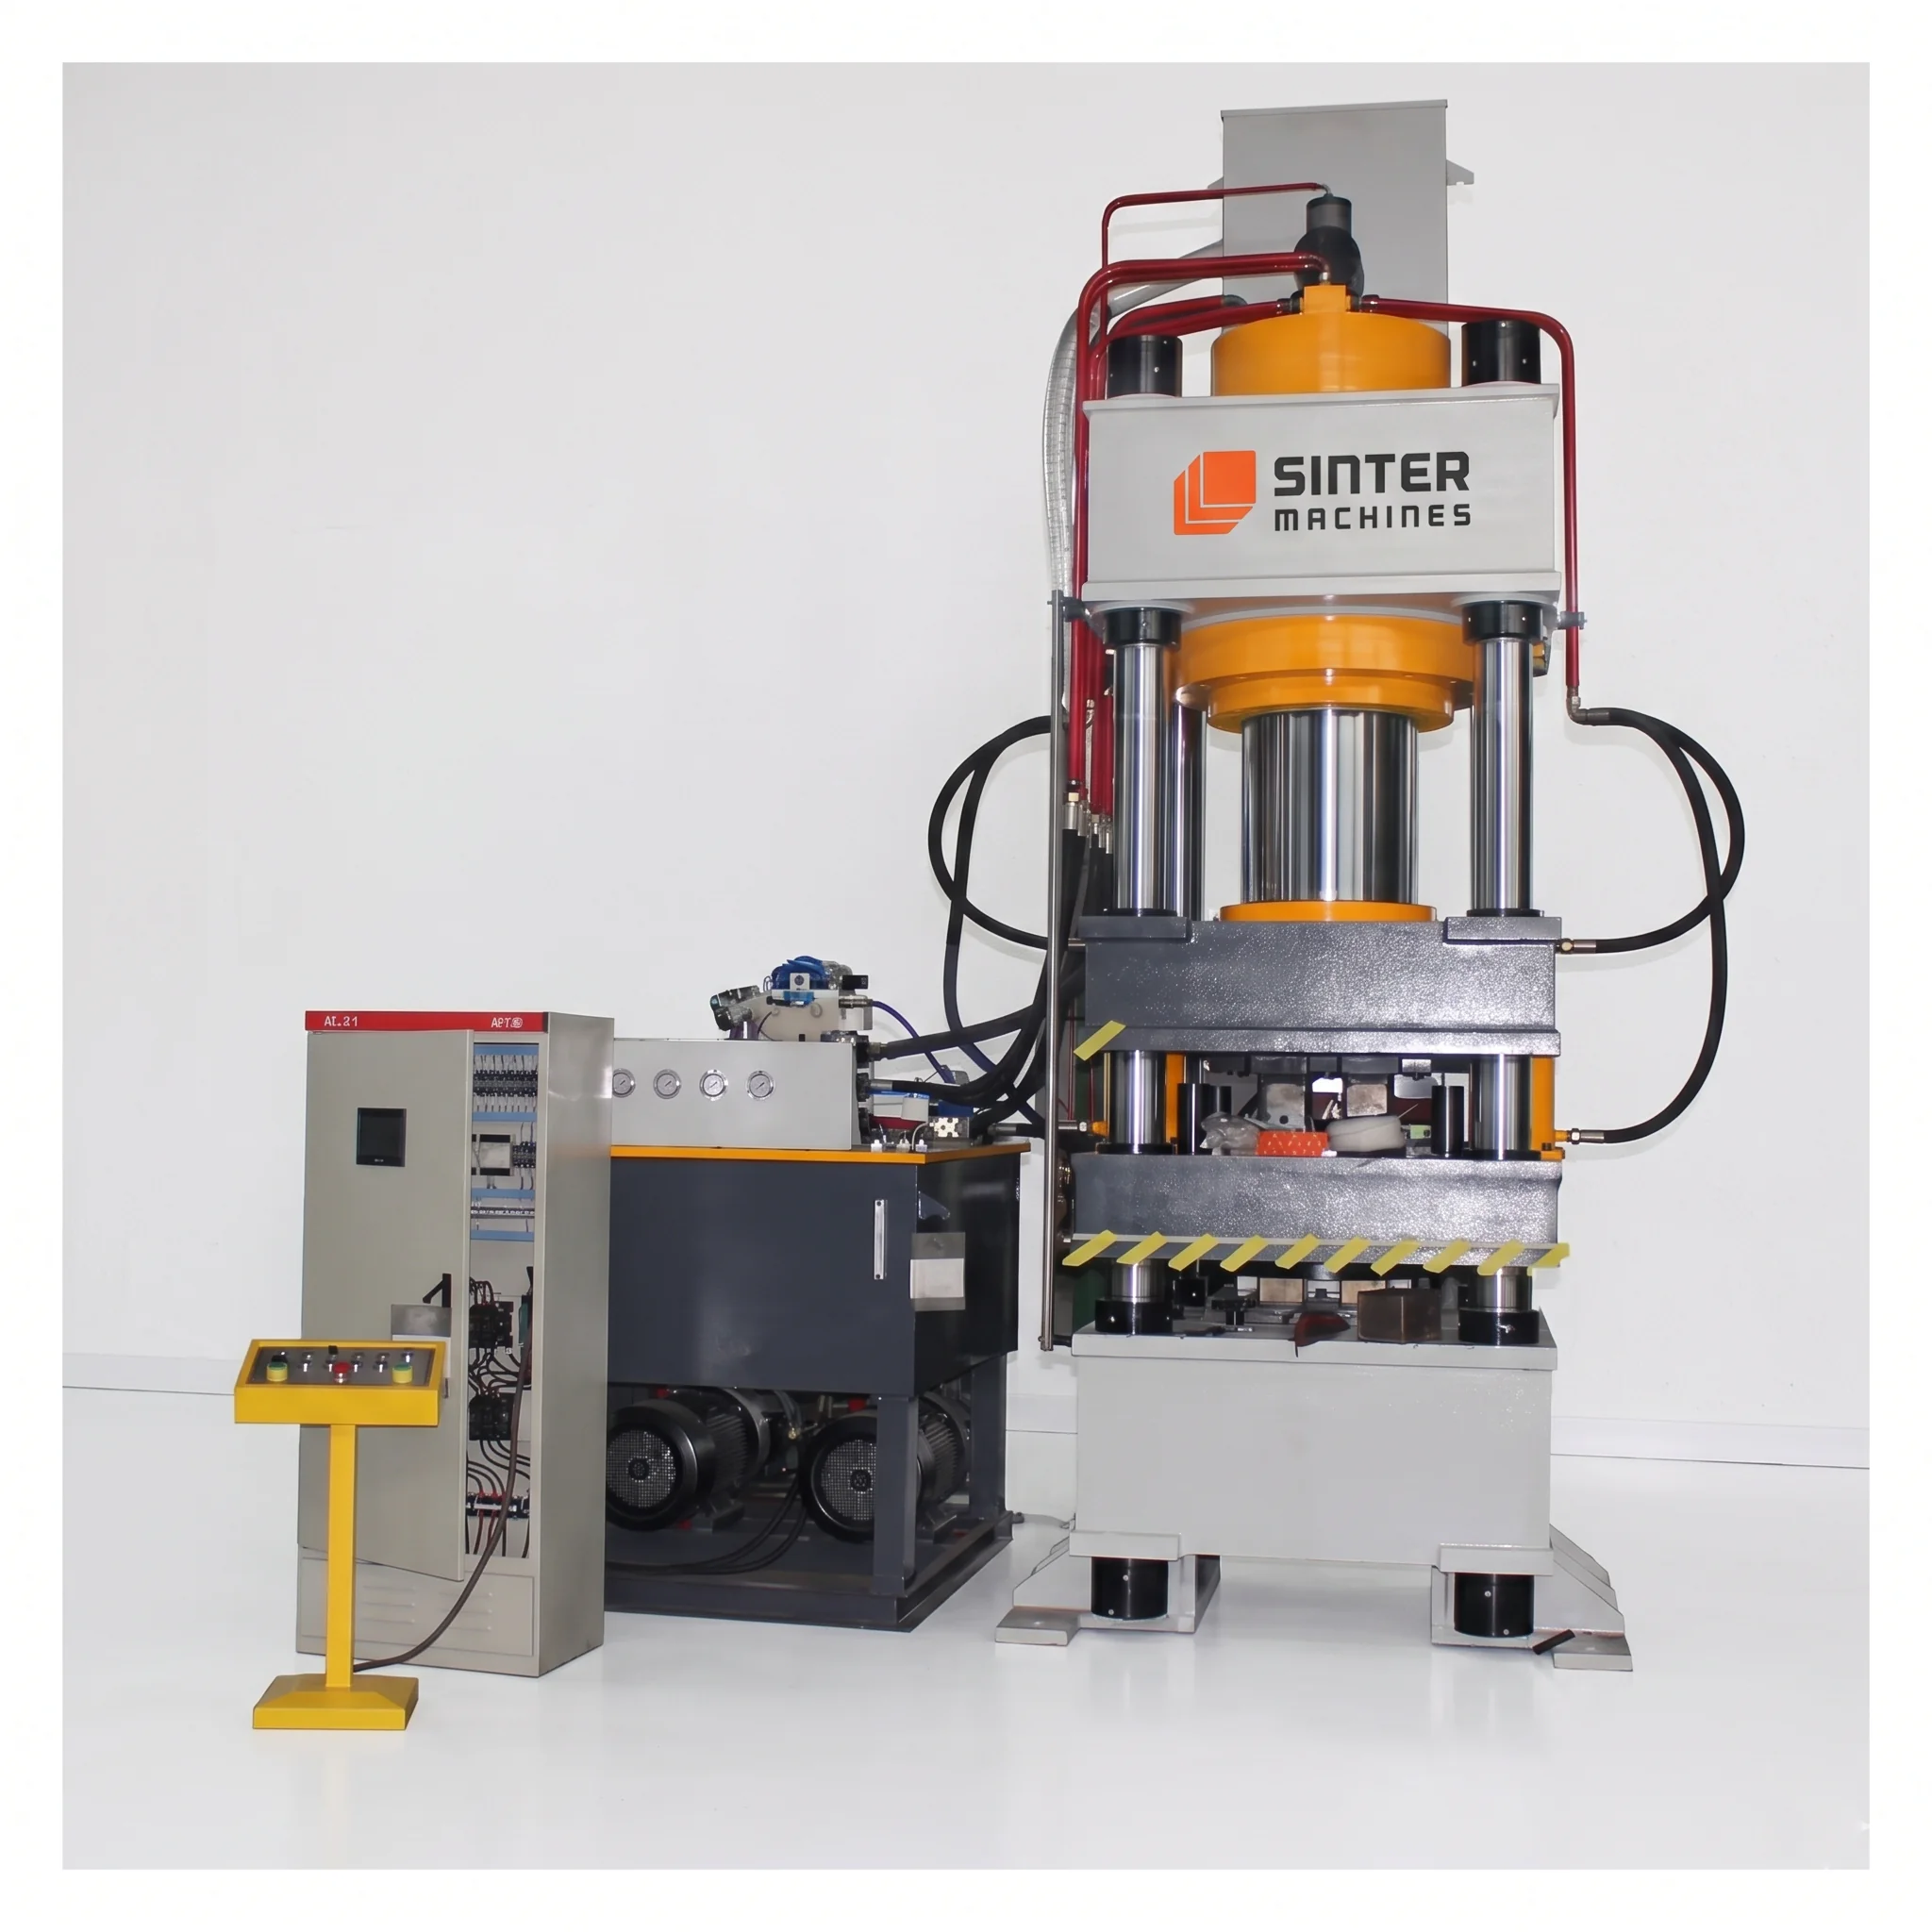
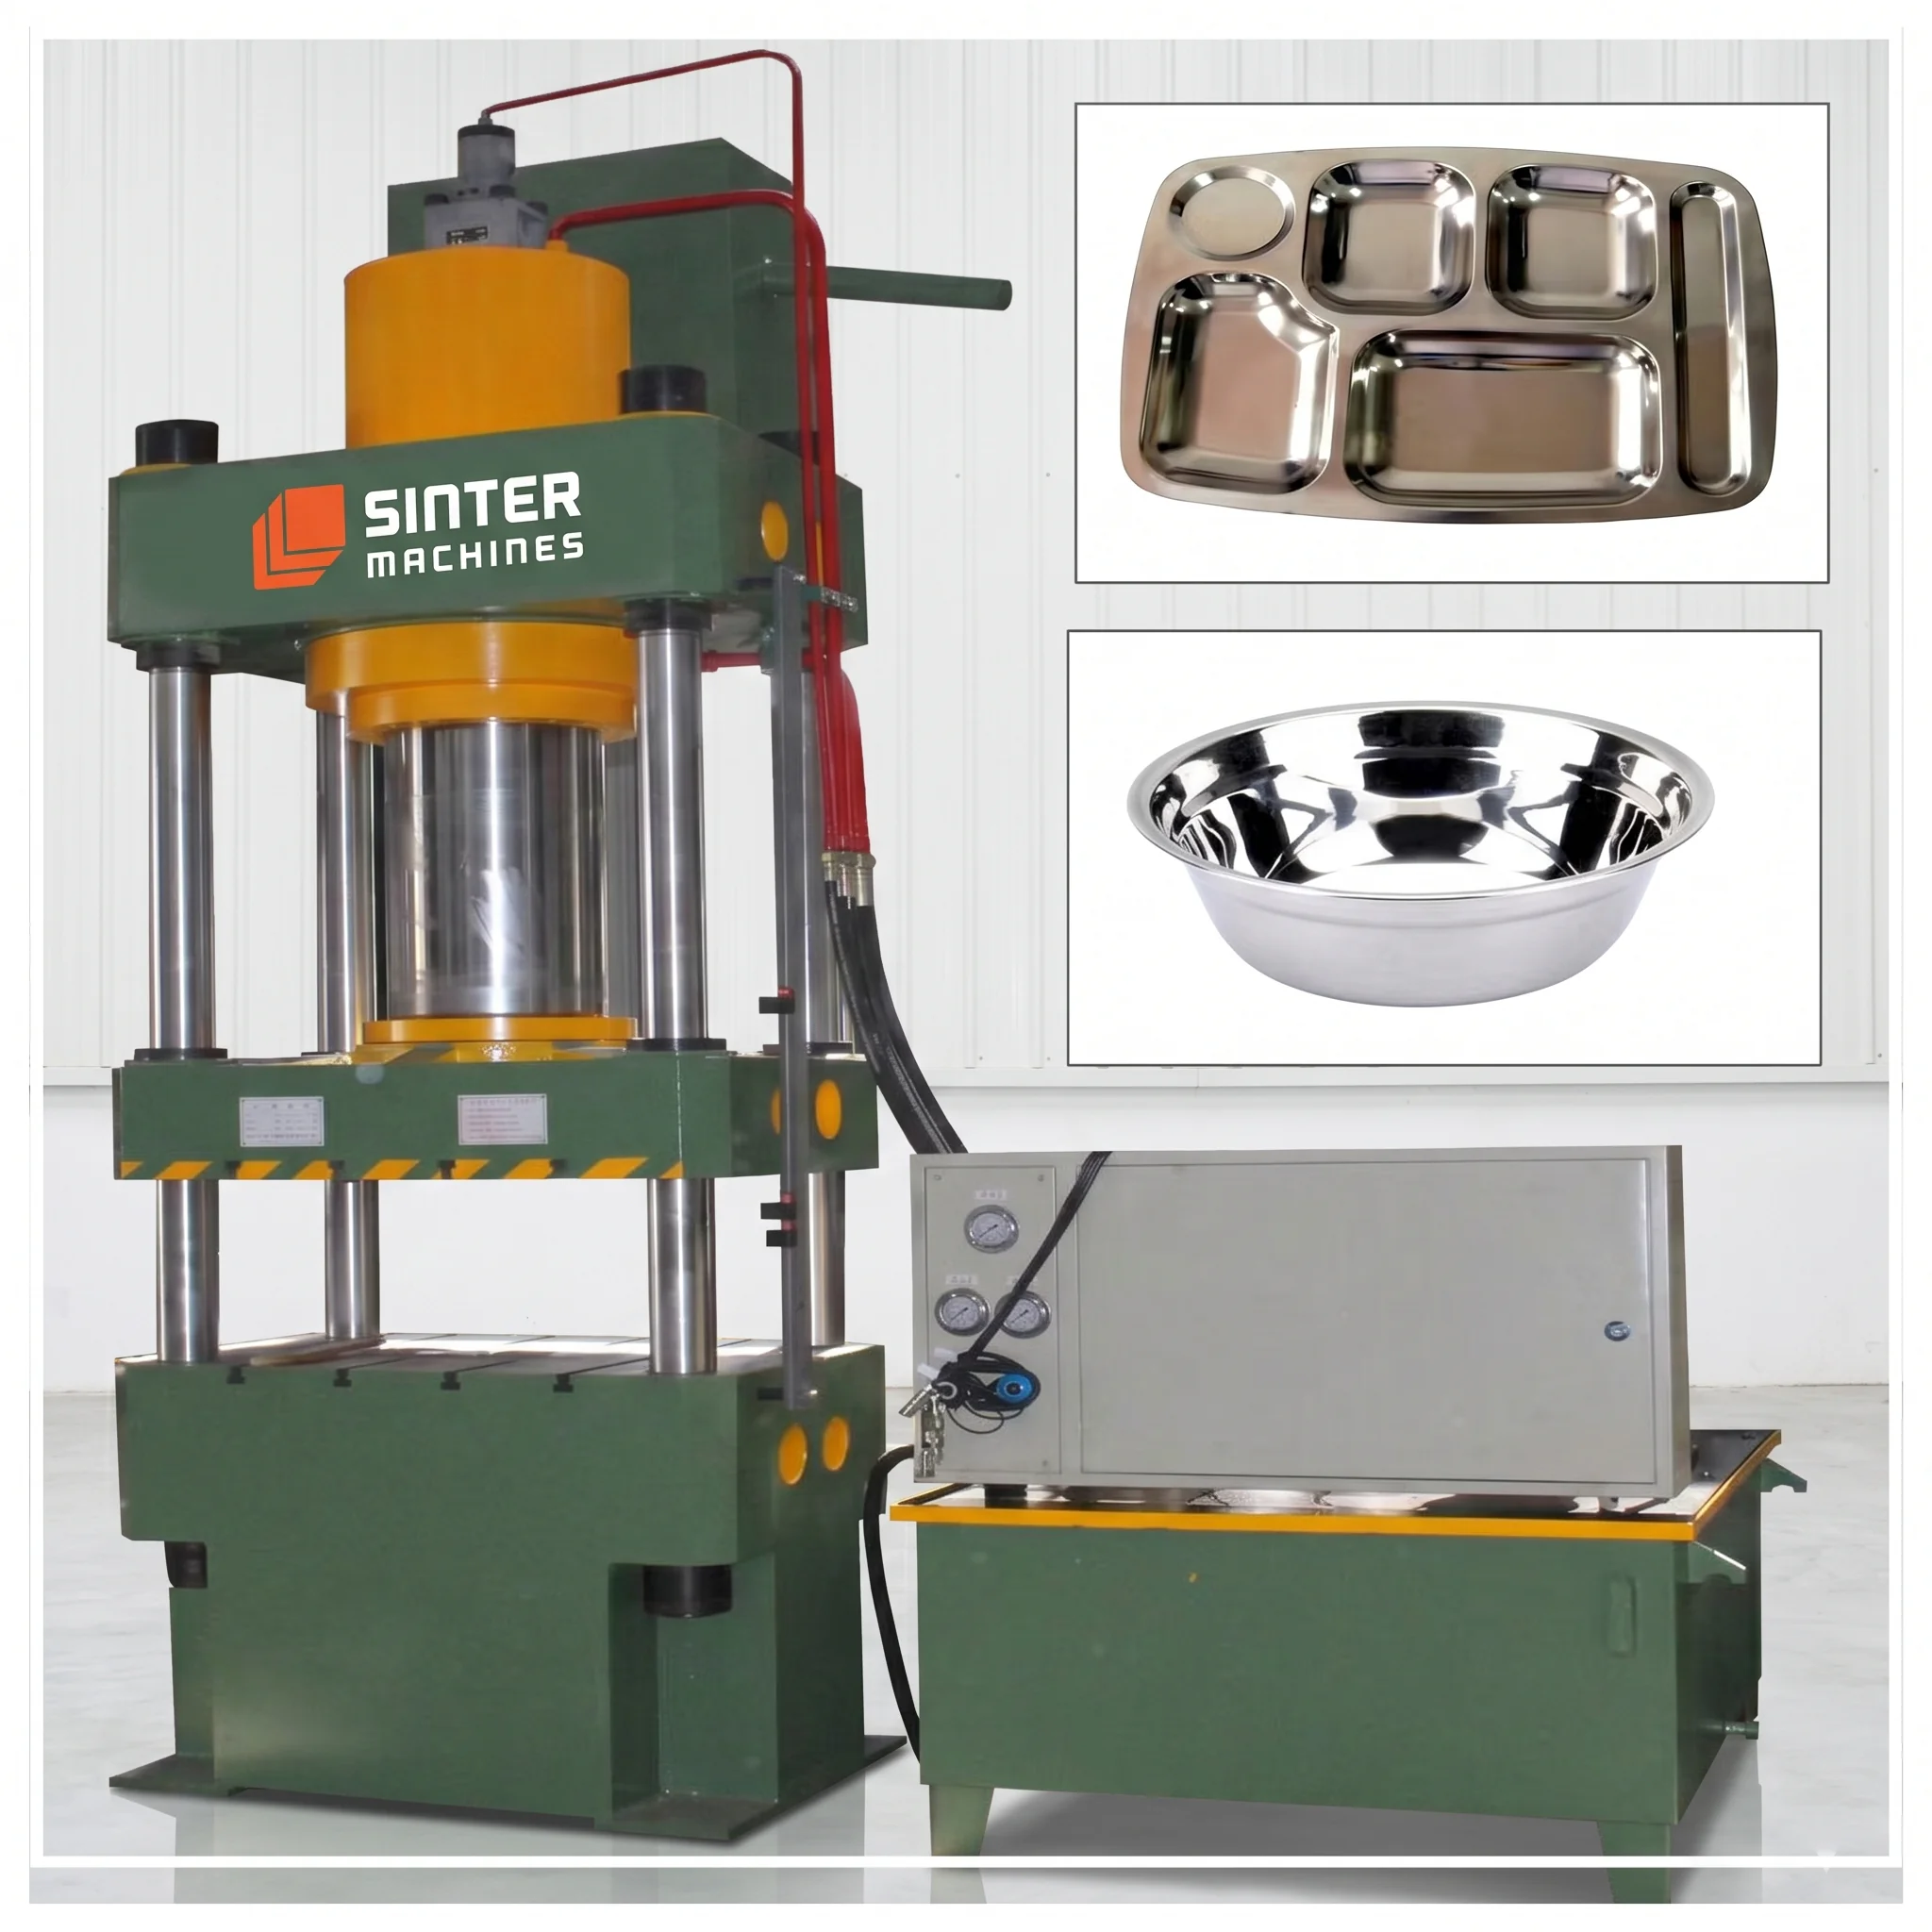
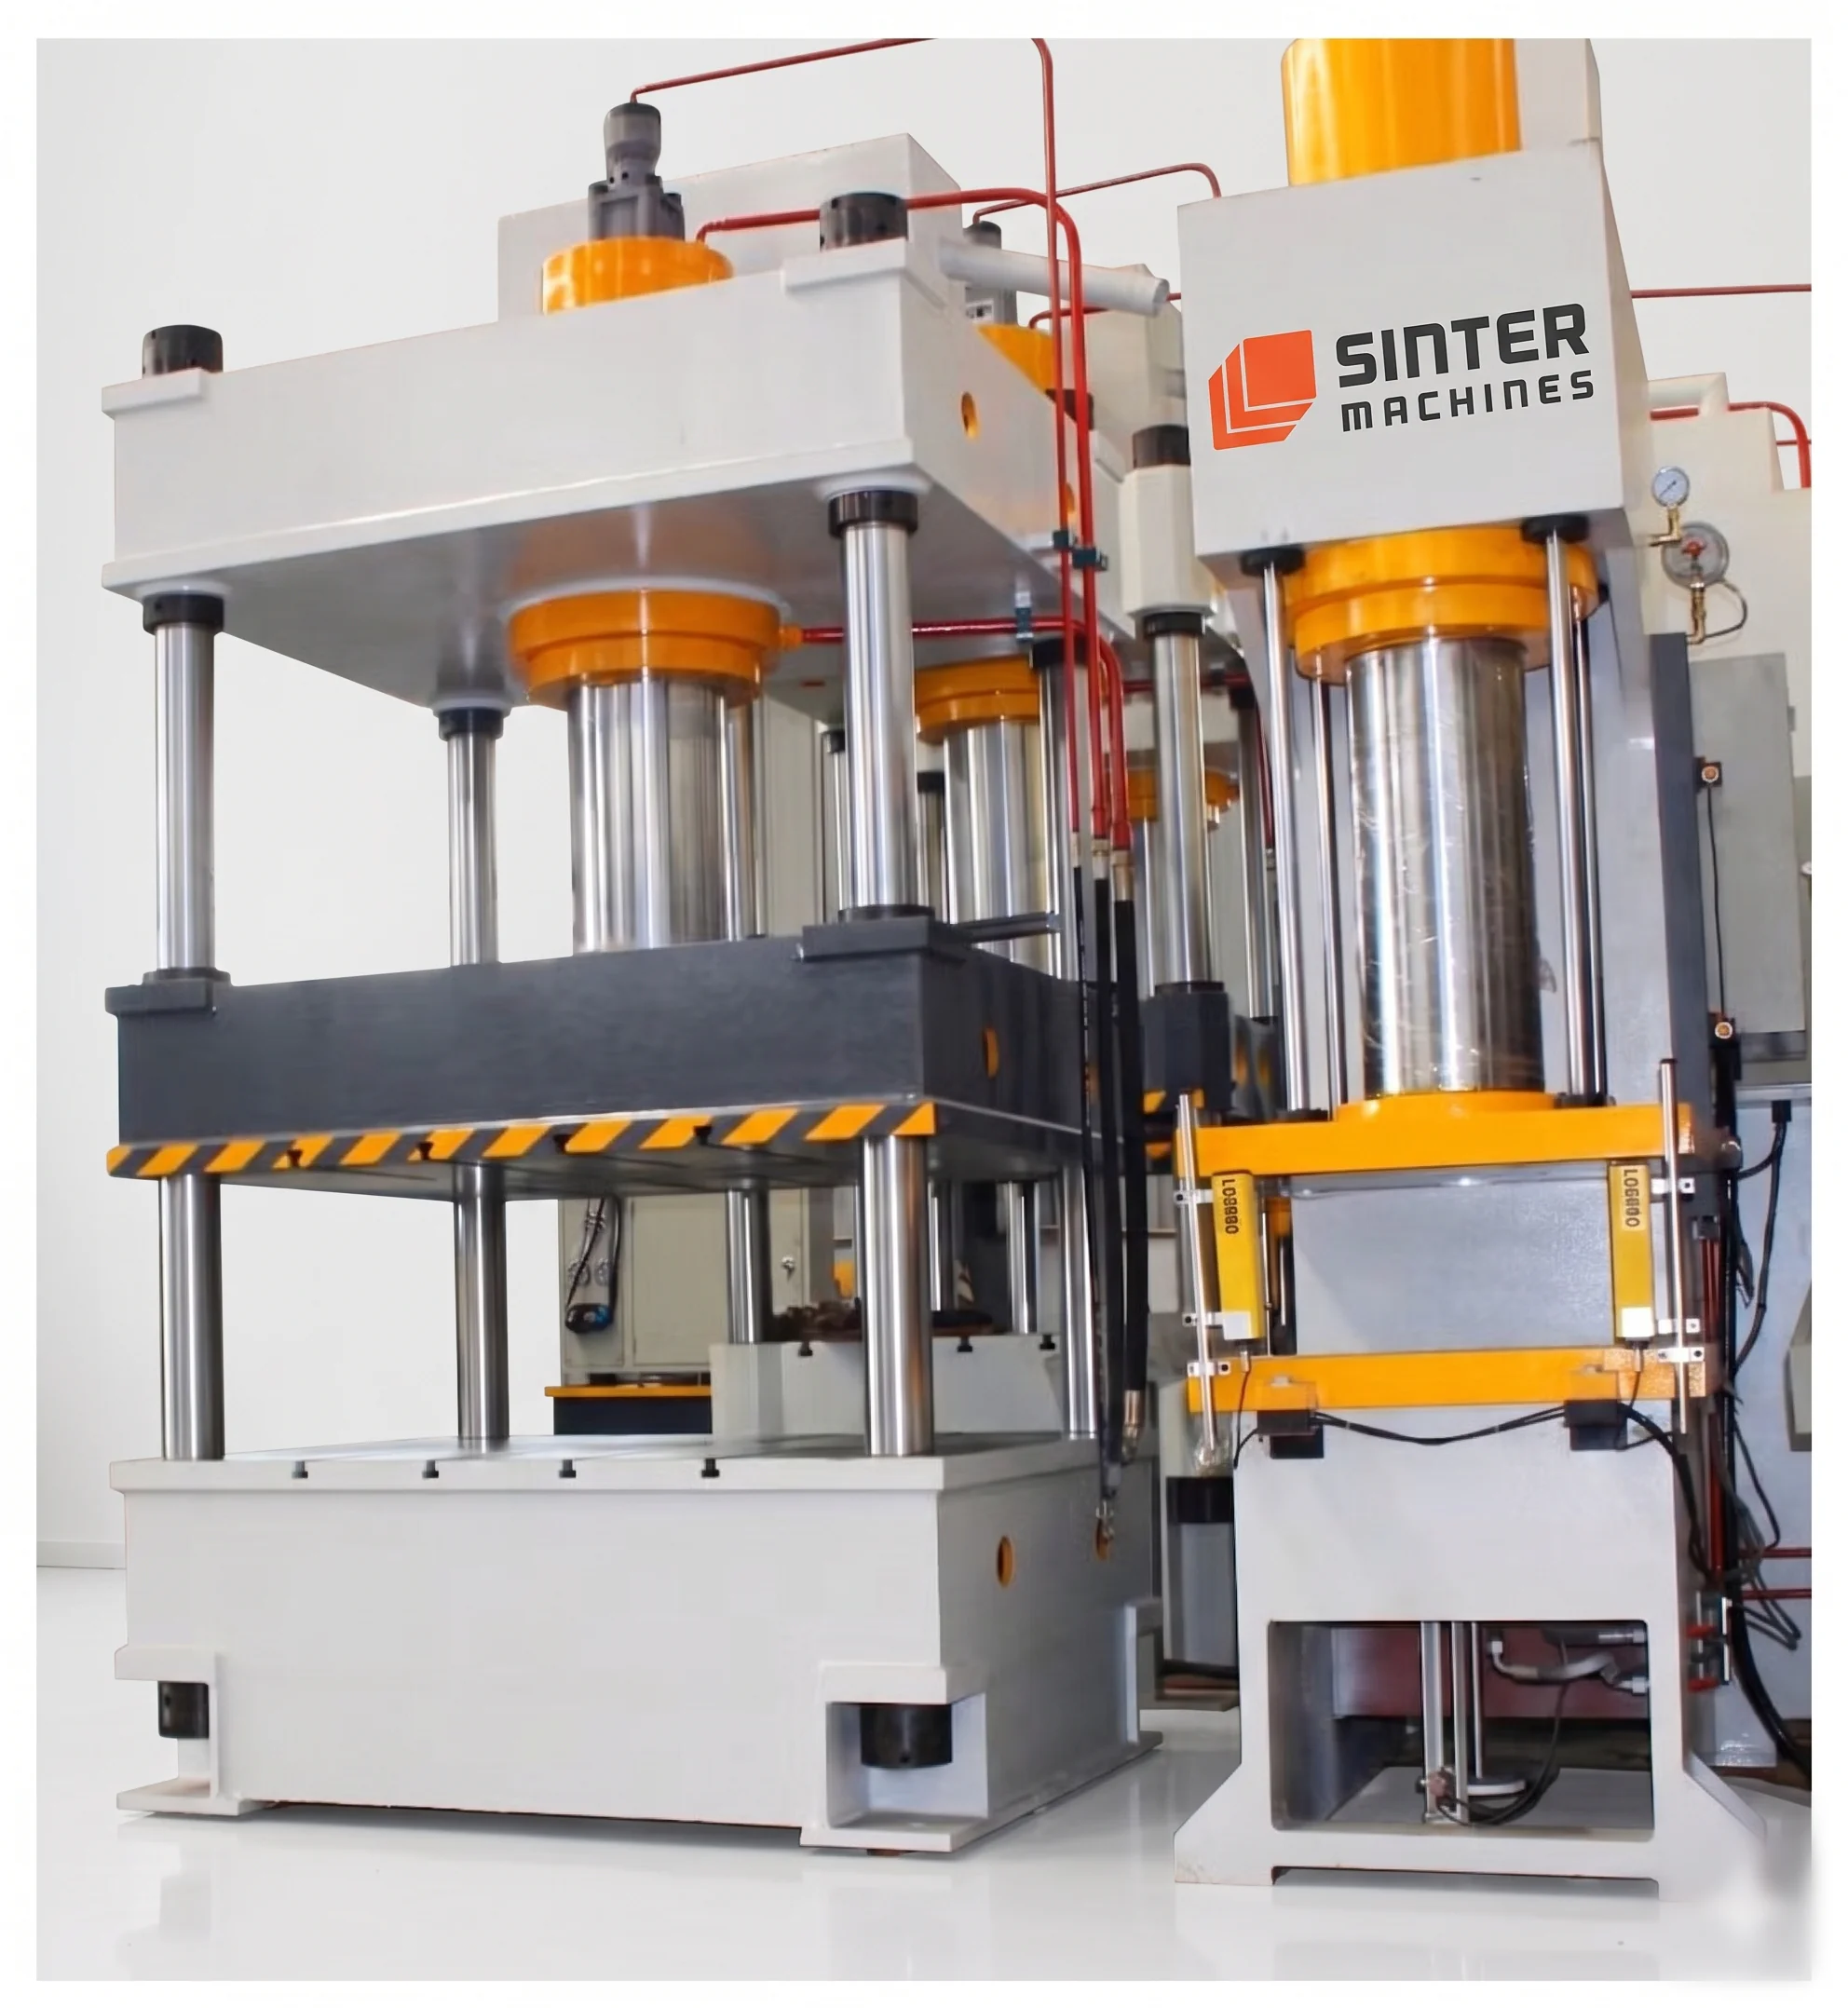
1250 Ton Four Pillar Hydraulic Press Machine
The 1250-ton four-pillar hydraulic press is the core machine for manufacturing deep-drawn seamless gas cylinders, delivering extreme force with precise control for safe, defect-free production. It is engineered to ensure compliance-ready pressure-vessel manufacturing while maintaining a long service life in heavy, demanding industrial environments.
Use Case
Deep-drawn seamless gas cylinders are safety-critical pressure vessels forged from thick steel blanks that must strictly adhere to international standards like ISO, EN, DOT, and ASME. This press is essential for executing the primary deep drawing (cup forming), re-drawing, and bottom shaping stages required to produce these high-strength containers.
- Core Applications: Primary deep drawing (cup forming), multi-stage re-drawing (elongation), and bottom shaping/doming (preform stage) for pressure vessels.
- Material: Heavy-duty, thick steel blanks and high-strength structural steels capable of withstanding extreme internal pressures.
- Typical Products Formed: Large-diameter, high-pressure seamless gas cylinders utilized across industrial, medical, and commercial sectors.
- Key Functions: Applies immense, accurately controlled pressing force over a long stroke to ensure smooth material flow and prevent thinning, wrinkling, or tearing during the draw.
- Why 1250-Ton Hydraulic Press?: It provides the necessary tonnage and structural rigidity required when working with large-diameter, thick-walled high-strength steels that demand a long drawing stroke and mandatorily low defect rates.
02 — Technical Specifications
Complete Technical Data
The SM 1250 HP is an ultra-heavy-duty 1250-ton hydraulic press engineered specifically for the demanding deep-drawing process of high-pressure seamless gas cylinders. It integrates massive pressing force with precision stroke control to ensure uniform wall thickness and defect-free elongation of thick steel blanks.
Capacity
- Maximum Main Pressing Force: 1250 Tons (12500 kN)
- Die Cushion / Ejector Force: 300 - 400 Tons (Critical for stripping and holding heavy preforms)
Structural Design
- Ultra-rigid, heavily reinforced welded steel plate construction, ultrasonically tested for structural integrity
- Thermally stress-relieved to withstand continuous extreme high-tonnage fatigue without deflection
Frame Type
- Heavy-duty 4-Pillar (Column) configuration
- Features extra-long precision bronze or self-lubricating guides to handle the long-stroke requirements of cylinder drawing
Hydraulic System
- High-flow, servo-hydraulic or advanced proportional logic valve manifold system
- Equipped with a high-capacity continuous oil cooling and offline micro-filtration system for heavy industrial cycling
Main Ram Stroke: 1500 mm to 2000 mm (Extended stroke necessary for deep elongation of gas cylinders, adjustable via linear transducers)
Working Hydraulic Pressure: Maximum Operating Pressure: 250 - 280 Bar (25 - 28 MPa)
Daylight Gap: Maximum Open Height (Bolster plate to ram): 2500 mm to 3000 mm (Accommodates tall tooling and final cylinder length)
Approach Speed: Rapid descent speed for cycle optimization: ~200 - 250 mm/sec
Pressing / Drawing Speed: Highly controlled, variable drawing speed: 8 - 15 mm/sec (Optimized to prevent tearing in thick-walled high-strength steel)
Return Speed: Fast retract speed: ~180 - 200 mm/sec
Bed / Platen Size Platen
- Dimensions: ~1500 mm x 1500 mm (Designed specifically for deep draw die configurations)
- Precision machined with standard T-slots for secure, heavy die clamping
Columns
- Solid forged steel (EN-8/EN-9 or equivalent), hard-chrome plated and precision ground
- Massive diameter: ~350 mm to 400 mm to resist lateral forces during deep drawing
Working Envelope
- Front Opening: ~1600 mm for robust material handling and overhead crane access
- Side Opening: ~1600 mm for maintenance and automated extraction systems
Control System
- Advanced Industrial PLC (e.g., Siemens or Allen-Bradley)
- Large HMI Touch Panel for precise stroke profiling, pressure setting recipes, and real-time diagnostics
Main Motor Power: 120 kW to 150 kW (Multiple high-efficiency IE3 induction motors driving dual or triple pump groups)
Valves & Hydraulics
- Premium proportional directional and pressure control valves (e.g., Rexroth, Parker)
- Integrated pre-fill valves for rapid ram gravity descent
Automation
- Fully integrated interfaces for robotic blank feeding, transfer systems, and automated cylinder extraction
- Centralized automatic lubrication system for continuous 24/7 operations
Safety Features
- Heavy-duty front and rear photoelectric light curtains
- Mechanical ram safety locking mechanism (anti-fall blocks) for safe die maintenance
- Dual-palm, anti-tiedown operation buttons and multiple strategically placed Emergency Stop buttons
SM 1250 HP — Model Specifications
- Nominal Force: 12500 KN
- Maximum Hydraulic Pressure: 25 MPa
- Max Opening Height of the Slider: 1500 mm
- Max Stroke of the Slider: 900 mm
- Effective Bed Size: 1600 × 1600 mm
- Slider Down Speed: 180 mm/s
- Slider Pressing Speed: 6–15 mm/s
- Slider Return Speed: 200 mm/s
- Ejector Cylinder Nominal Force: 600 KN
- Stroke of the Ejection Cylinder: 300 mm
03 — Die / Mold System
Precision Deep Drawing Seamless Gas Cylinders Die Mold Engineering
Precision deep drawing die molds are engineered to manage extreme localized pressures and friction, seamlessly transforming thick-walled steel blanks into high-strength gas cylinders. These robust tool sets prioritize thermal stability and precise material flow to prevent wrinkling, tearing, or wall thinning during the intense forming process.
Technical Specifications (Tooling)
Die Type
- Progressive multi-stage deep drawing and ironing (re-drawing) dies.
- Specialized configurations for initial cupping, intermediate elongation, and final bottom preform doming.
Die Materials
- Punch & Die Matrix: High-grade, vacuum-hardened cold-work or hot-work tool steels (e.g., SKD11, D2, H13) for extreme wear resistance.
- Inserts: Replaceable tungsten carbide rings utilized in high-friction ironing zones to maximize tooling longevity.
- Blank Holder: Forged alloy steel treated with specialized surface hardening to withstand high clamping forces.
Tool Configuration & Construction
- Modular, cassette-style architecture enabling rapid replacement of high-wear inserts without dismantling the entire tool set.
- Integrated internal cooling channels designed to continuously dissipate the immense frictional heat generated during thick-wall drawing.
Key Tooling Features
- Mathematically optimized die entry radii and punch profiles to guarantee uniform material flow and prevent galling.
- Heavy-duty mechanical or hydraulic stripper mechanisms engineered for the safe, jam-free extraction of the formed cylinder from the punch.
Alignment Accuracy
- Precision-ground guide pillars and self-lubricating bronze bushings ensuring micro-level concentricity between the punch and the matrix.
- Extremely tight radial clearance tolerances (maintained within ±0.05 mm to ±0.1 mm) to ensure uniform global wall thickness on the finished vessel.
Materials Formed
- Heavy-gauge carbon steels, manganese steels, and high-strength chromium-molybdenum alloy plates (e.g., 34CrMo4 or 37Mn).
- Engineered to accommodate starting blank thicknesses typically ranging from 4 mm to 15 mm.
Surface Finish
- Working surfaces of punches and die rings are ultra-polished to a mirror finish to minimize drawing resistance.
- Friction zones are treated with advanced PVD coatings (e.g., TiN, TiCN) or hard-chrome plating to drastically reduce friction and ensure a scratch-free finish.
Tool Life
- Tungsten Carbide Inserts: Typically endure 250,000 to 500,000 production cycles before requiring replacement or major redressing.
- Tool Steel Components (PVD Coated): Generally yield 100,000 to 200,000 cycles, depending on blank thickness and material grade, when supported by routine polishing maintenance.
Precision Deep Drawing Seamless Gas Cylinders Die Mold
04 — Product Application
Where Deep Drawing Seamless Gas Cylinders Are Used
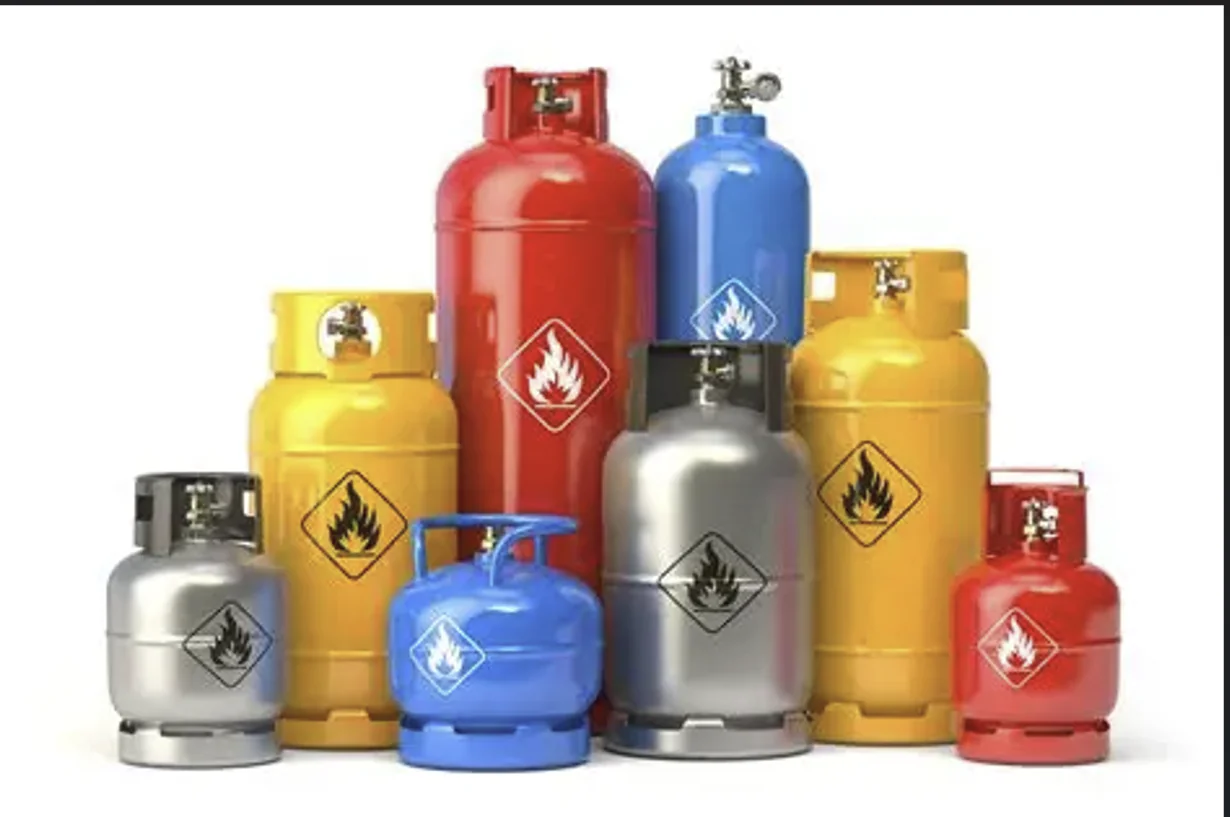
Deep-drawn seamless gas cylinders are critical for the safe storage and transport of high-pressure gases under extreme conditions. Their robust, weld-free construction makes them indispensable across various high-stakes global industries.
Industry Applications
Industrial Manufacturing & Welding
These cylinders store shielding and cutting gases like oxygen, argon, and acetylene required for heavy metal fabrication. Their durable, seamless design withstands the harsh physical environments and rough handling of industrial facilities.
Medical & Healthcare Facilities
They are essential for supplying life-saving medical oxygen, nitrous oxide, and breathable air mixtures in hospitals and emergency vehicles. The defect-free, smooth interior prevents contamination and ensures strict adherence to medical safety standards.
Automotive & Alternative Energy
Seamless cylinders are widely utilized as onboard storage vessels for Compressed Natural Gas (CNG) and hydrogen fuel cell vehicles. Their high-strength steel walls safely contain extreme pressures while maximizing the vehicle's fuel capacity and overall safety.
Firefighting & SCBA Equipment
They serve as the primary high-pressure air tanks for Self-Contained Breathing Apparatus (SCBA) gear used by first responders. The structural integrity of the seamless draw guarantees reliable air delivery in life-threatening, high-temperature rescue situations.
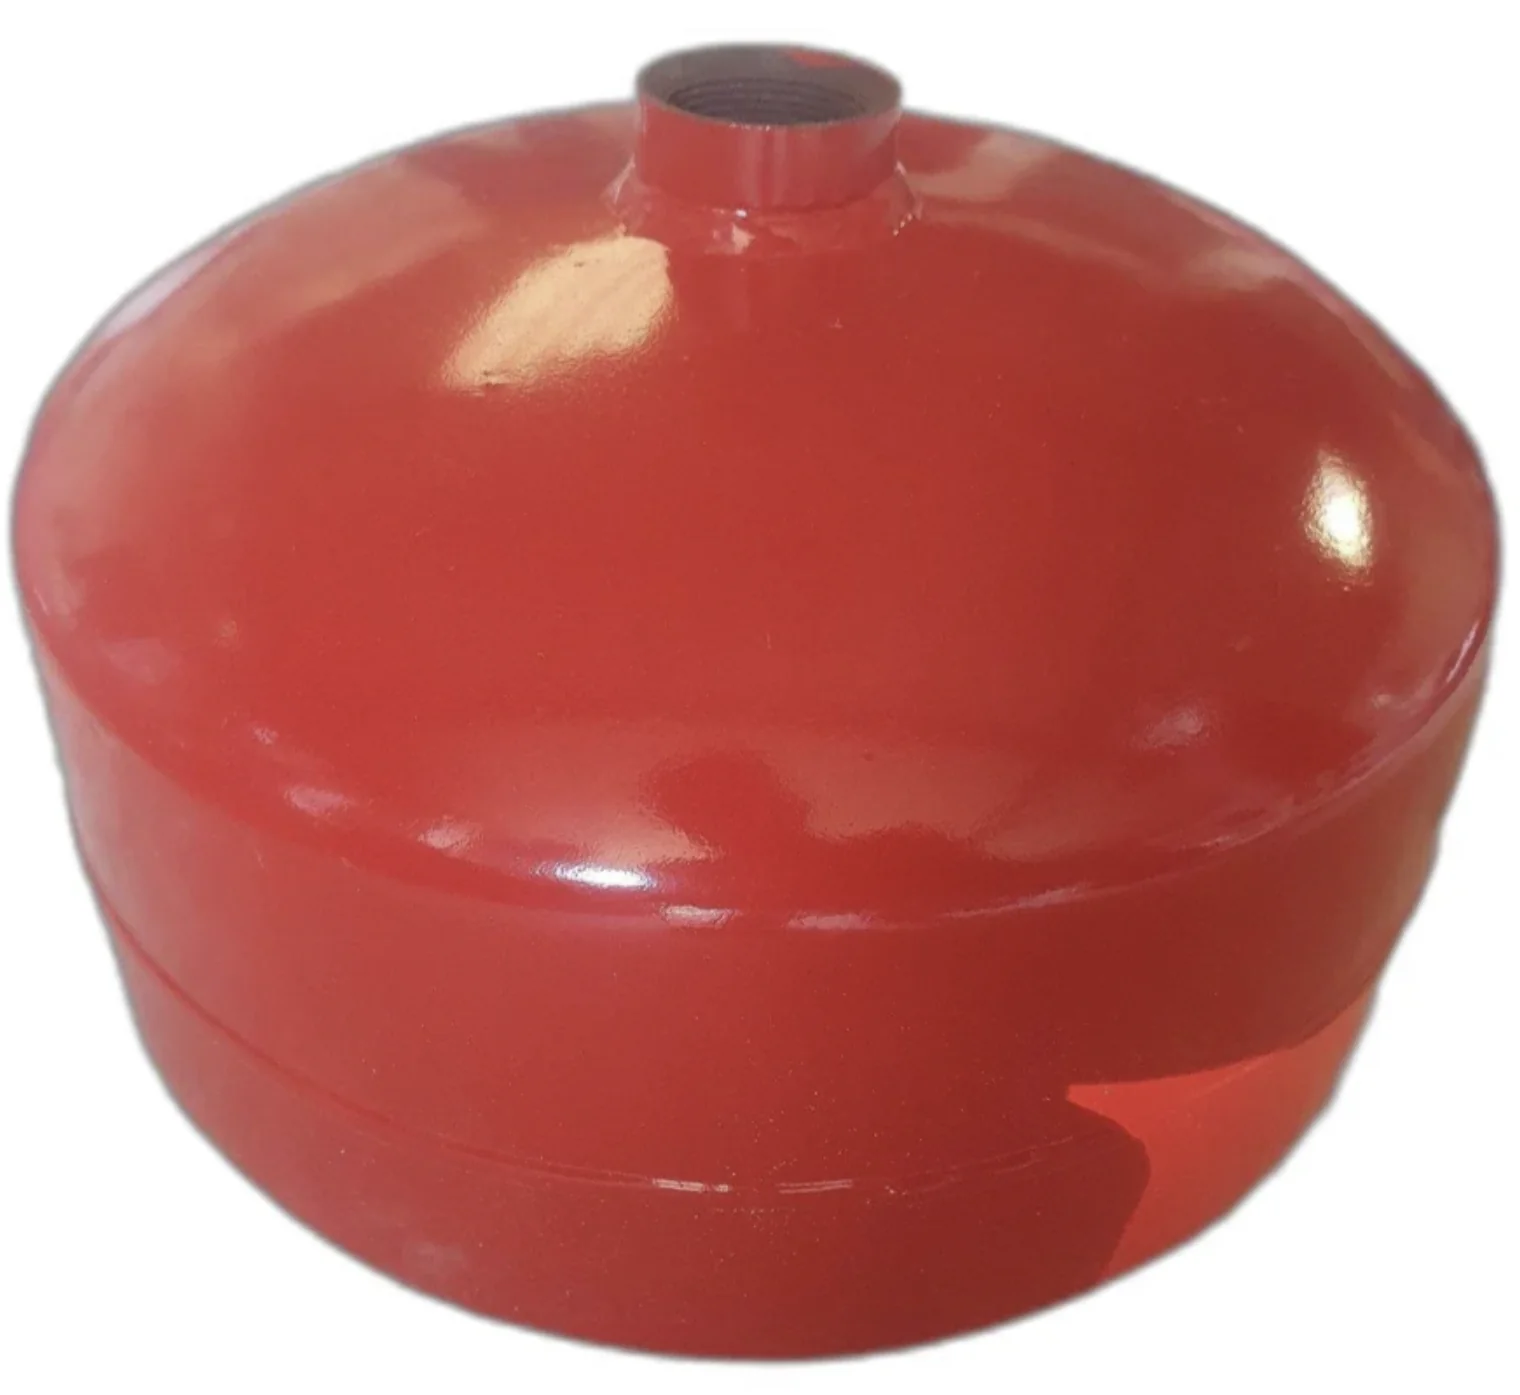
Finished Product Gallery
05 — Key Advantages
Why Choose the 1250-Ton Sinter Hydraulic Press
The 1250-ton hydraulic press delivers the immense tonnage and precise stroke control required to flawlessly draw thick steel blanks into high-pressure cylinders. Its advanced engineering ensures structural integrity, minimal material failure, and full compliance with strict global pressure vessel standards.
High-Tonnage Deforming Capability
Provides a massive 1250 tons of continuous force required to deep-draw thick-walled high-strength alloy steels. This extreme power ensures heavy steel blanks flow smoothly into shape without causing structural tearing.
Advanced Proportional Stroke Control
Features high-precision closed-loop hydraulic control that micro-adjusts ram speed and pressure profiles during the draw cycle. This precision prevents localized wall thinning and guarantees perfectly uniform thickness throughout the entire cylinder body.
Heavy-Duty Four-Pillar Rigidity
The robust four-pillar design offers exceptional resistance to heavy eccentric loads and minimizes frame deflection under peak tonnage. This superior structural stability maintains perfect concentric alignment between the punch and die for flawless cylinder geometry.
High Production Throughput via Automation
Engineered with fast approach and return speeds combined with seamless integration for robotic material handling lines. This significantly shortens individual cycle times, maximizing output capacity while maintaining hands-free operational safety.
Strict Quality Control and Safety Compliance
Equipped with advanced dual-palm controls, optical light curtains, and real-time HMI pressure monitoring systems. This guarantees compliance with rigid international pressure vessel regulations while providing a highly secure environment for operators.
Optimized Tooling Lifespan
Delivers ultra-smooth hydraulic transitions and controlled pressure buildup that significantly reduces friction and thermal stress on expensive die components. This drastically minimizes tooling wear, resulting in fewer maintenance shutdowns and lower overall operational costs.