01 — Press System
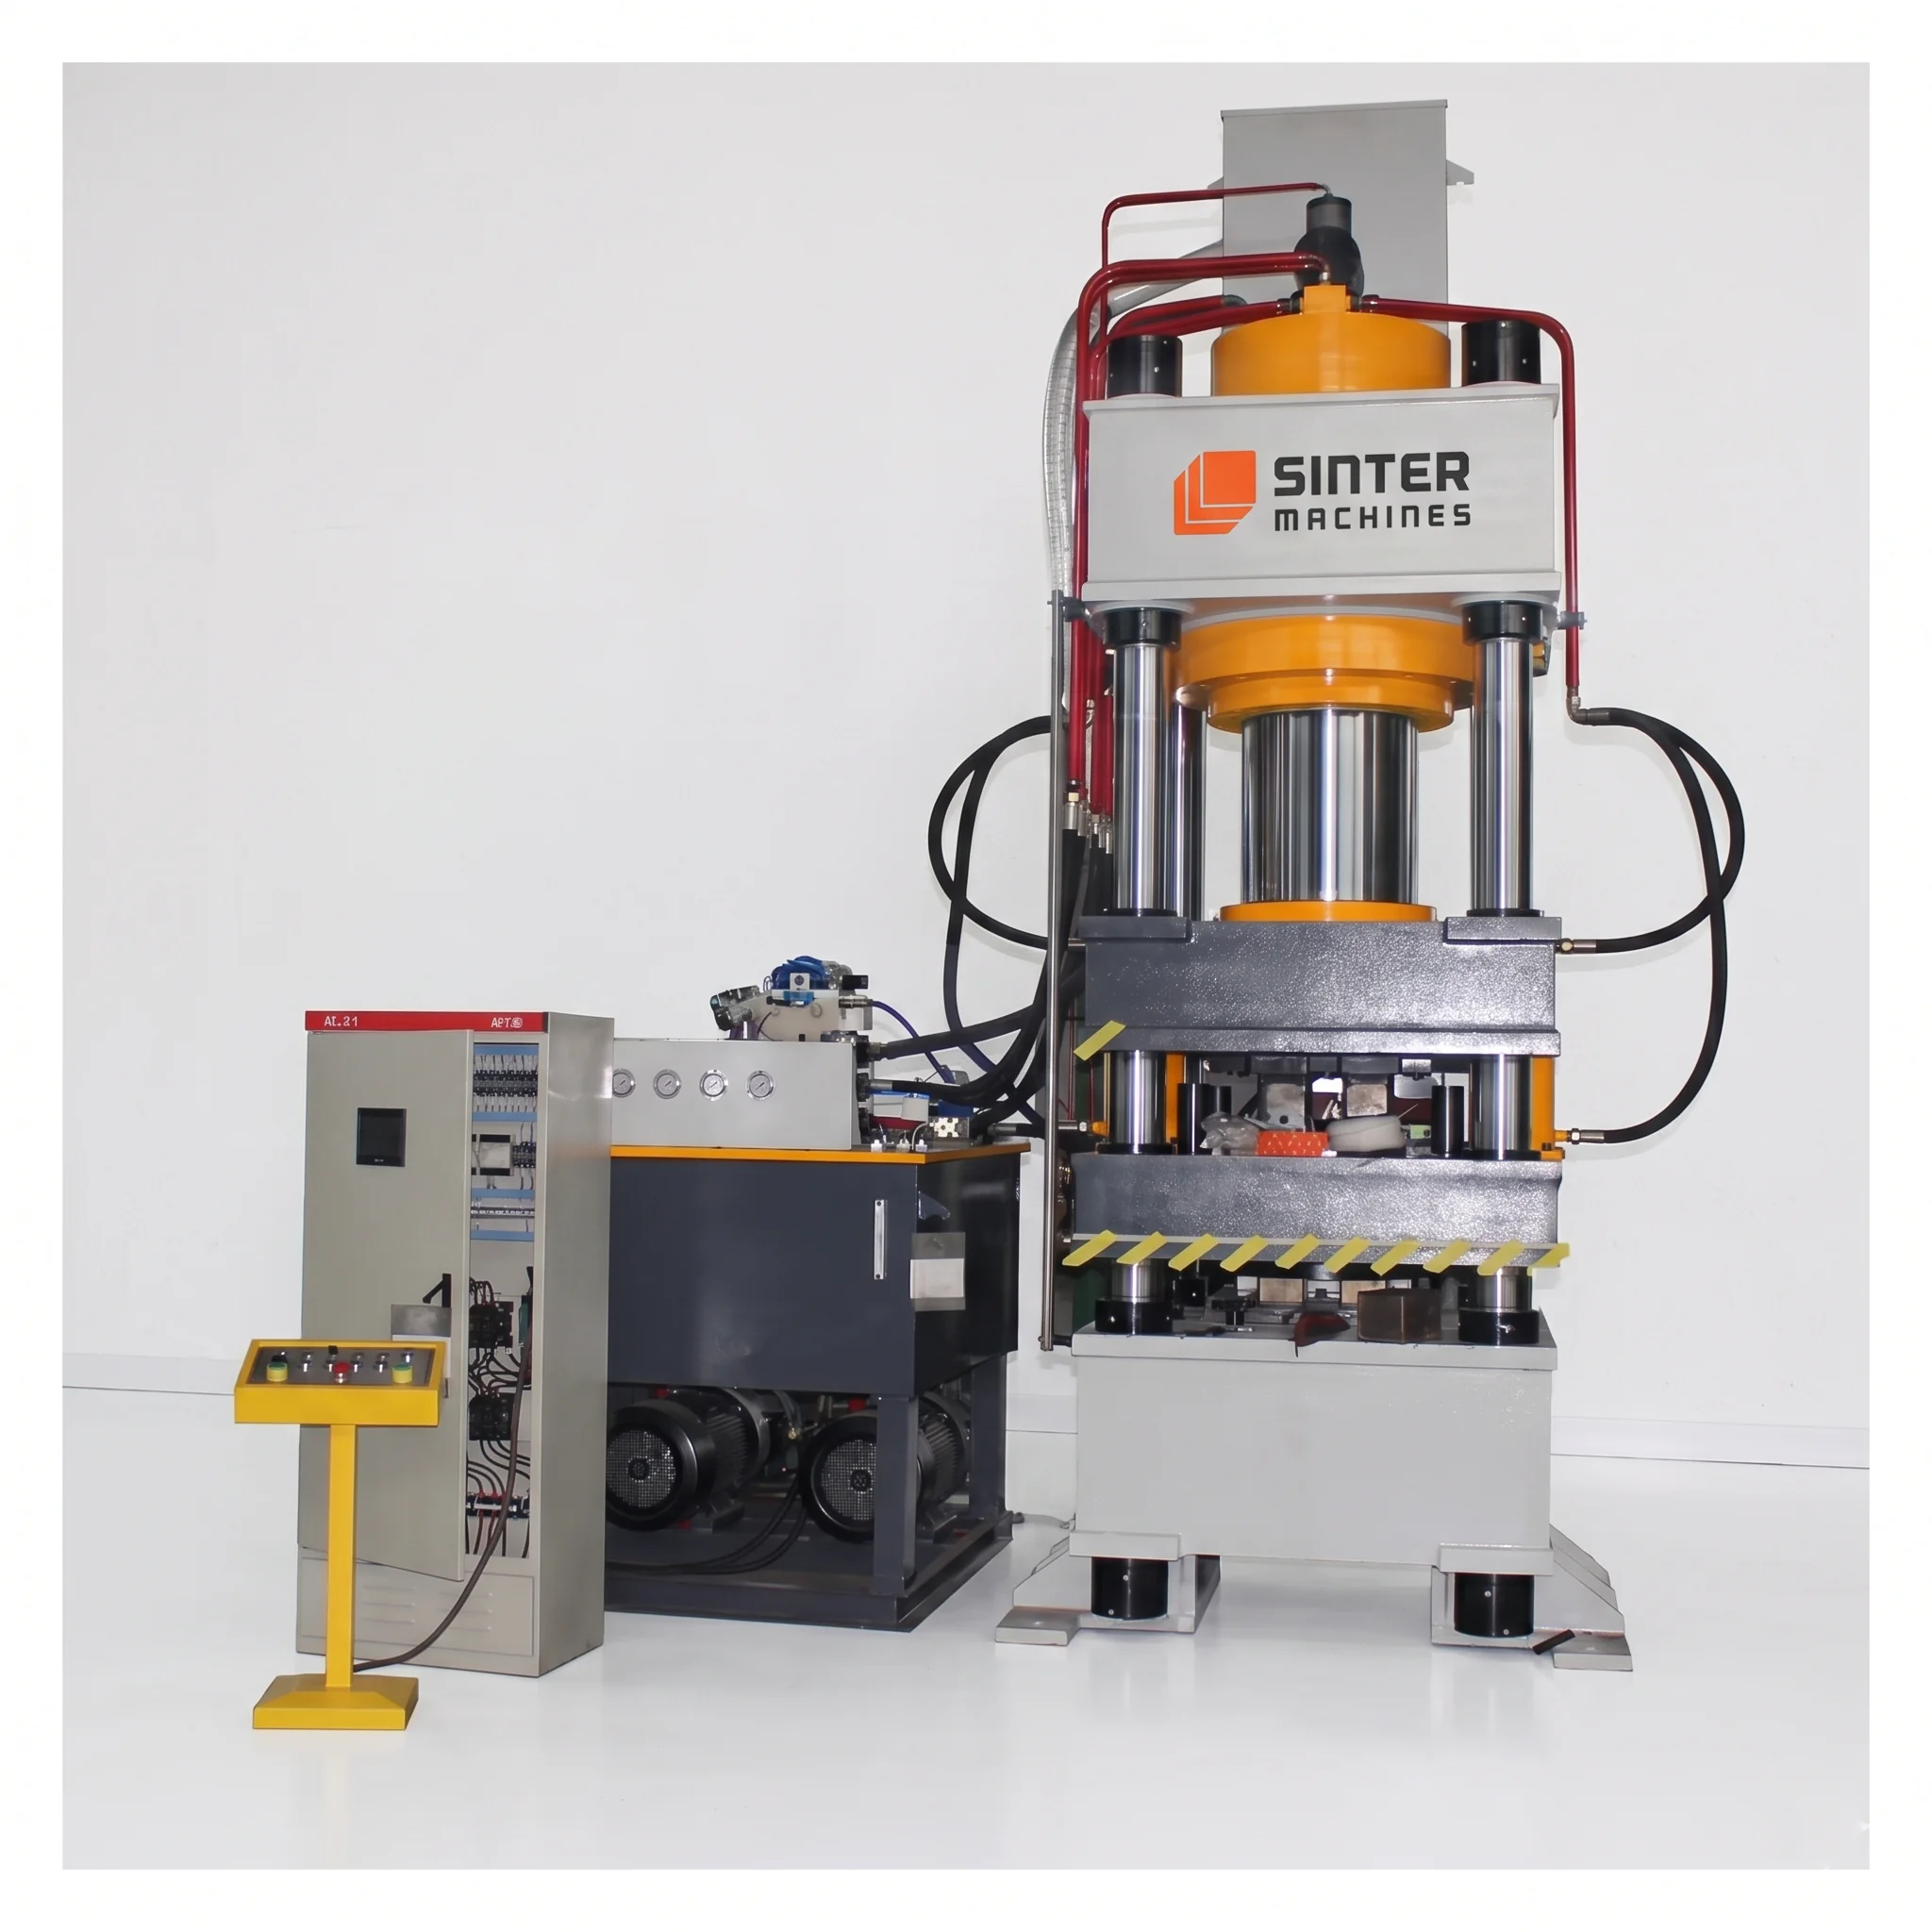
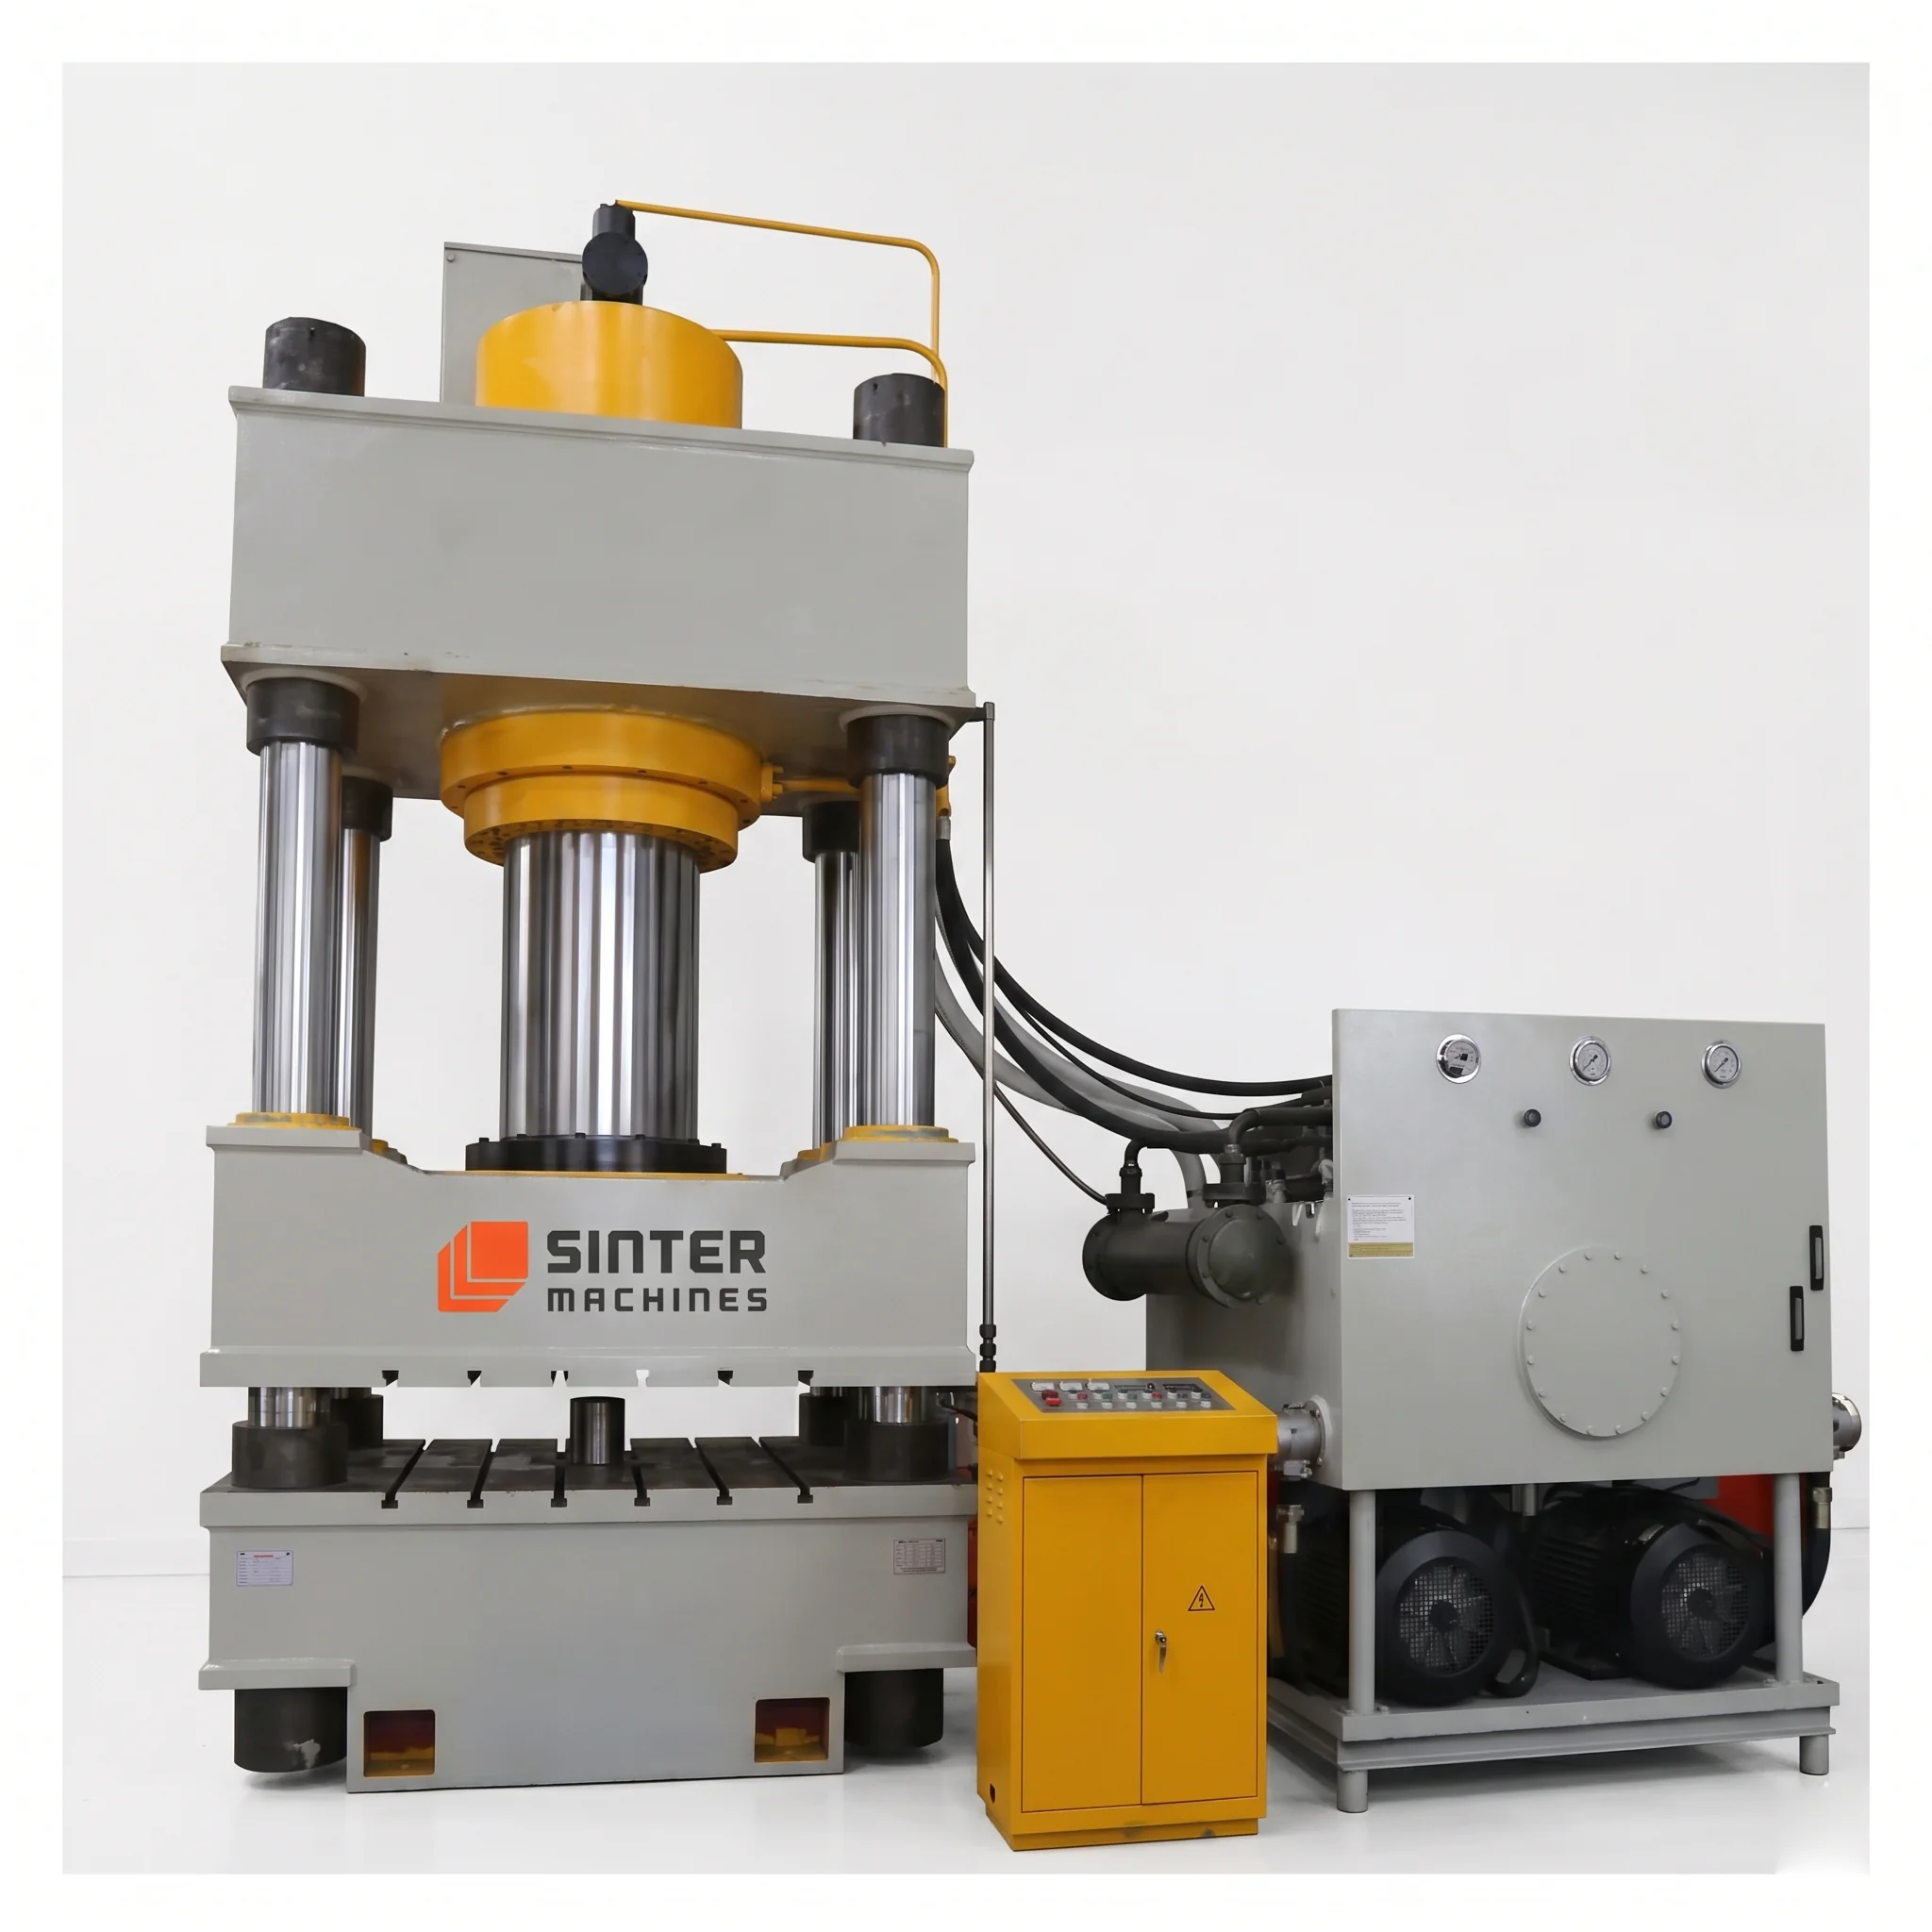
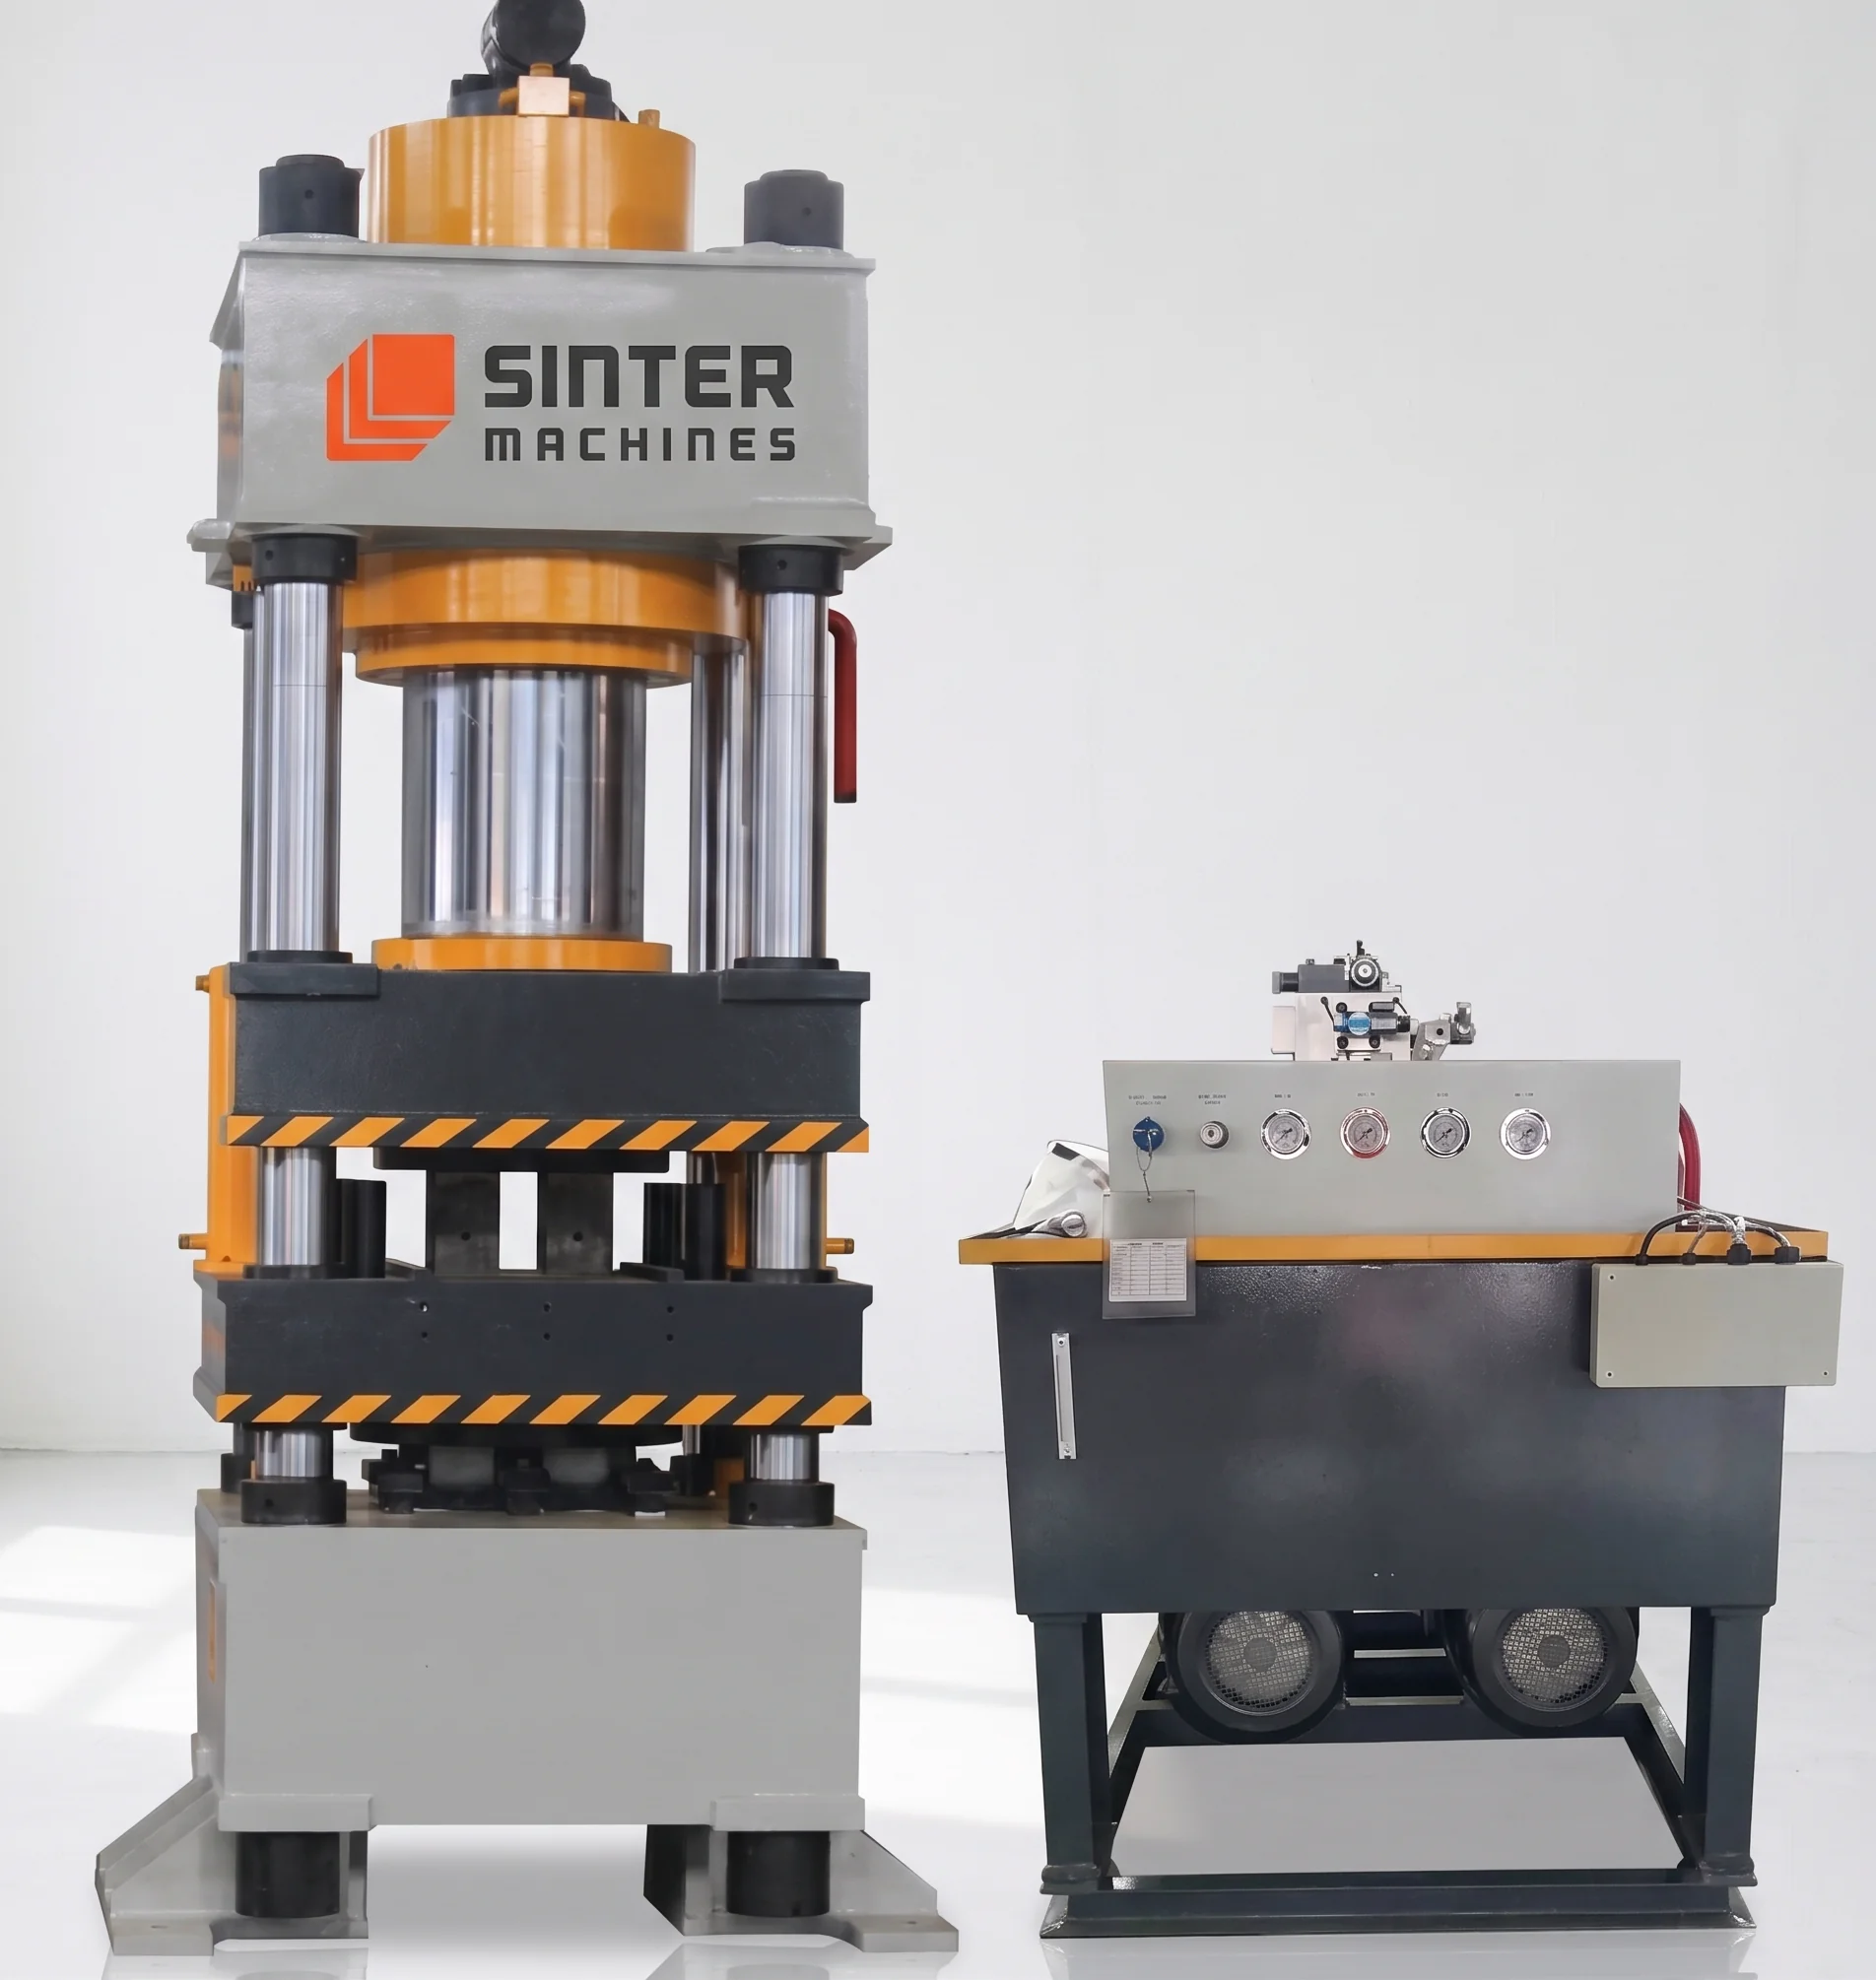
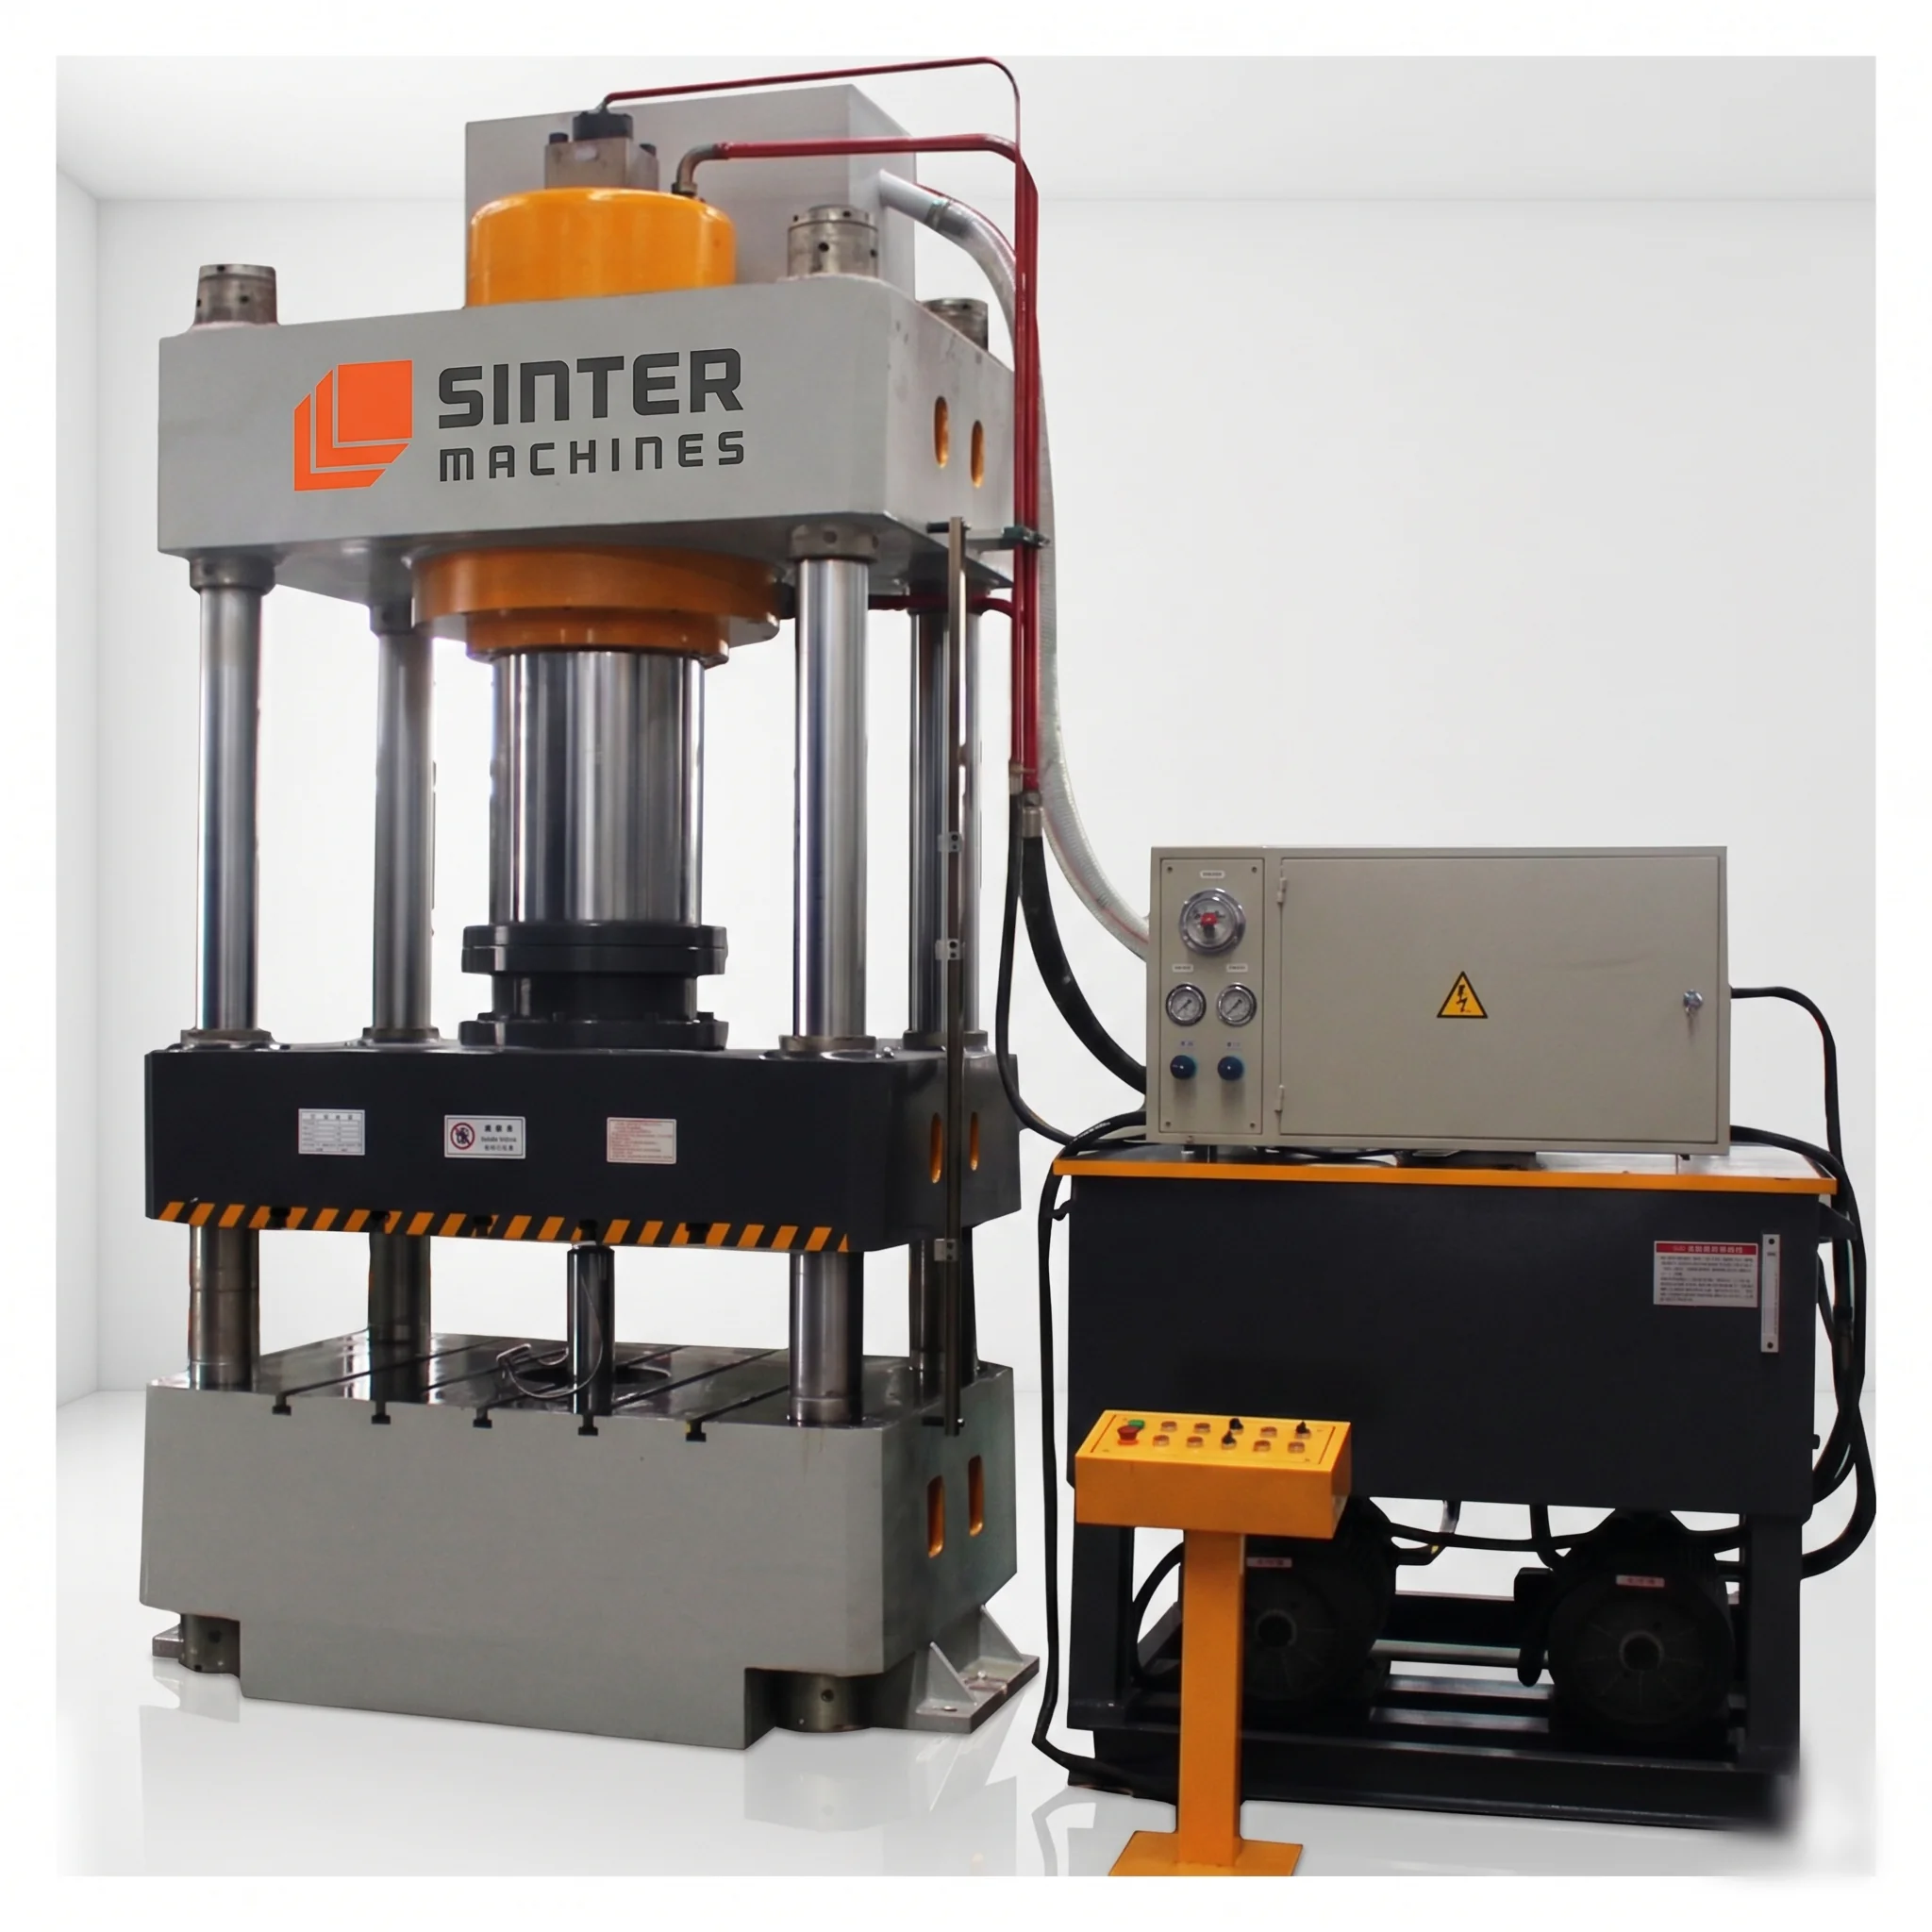
1250T Four Column Hydraulic Press Machine
The 1250-ton four-pillar hydraulic press is a robust, high-precision industrial forming system engineered to manufacture heavy-duty machinery components. This versatile layout incorporates heavy-engineering best practices to deliver long-term tooling stability under high-volume manufacturing conditions.
Use Case
Heavy industrial rollers and hydraulic tooling require uniform material density and flawless grain flow to withstand continuous surface abrasion and extreme mechanical stress. This press system provides the steady, high-capacity tonnage and parallel guiding necessary to shape large, dense alloy steel billets without introducing structural flaws.
Core Applications
- Closed-die and semi-closed-die hot forging of thick-section industrial cylinder and roller blanks
- Industrial upsetting, blocker forming, and preliminary mass redistribution of large steel billets
- High-tonnage precision flattening, sizing, and pre-form preparation of dense tool steel stocks
Material
- Medium-carbon structural steels, high-carbon wear-resistant steels, and chrome-manganese alloys
- Premium hot-work and cold-work tool steels along with specialized high-strength structural grades
- Heat-treated alloy steel formulations engineered to withstand continuous metal-on-metal contact friction
Typical Products Processed
- Heavy-duty industrial conveyor rollers, steel mill backup rolls, and guide rollers
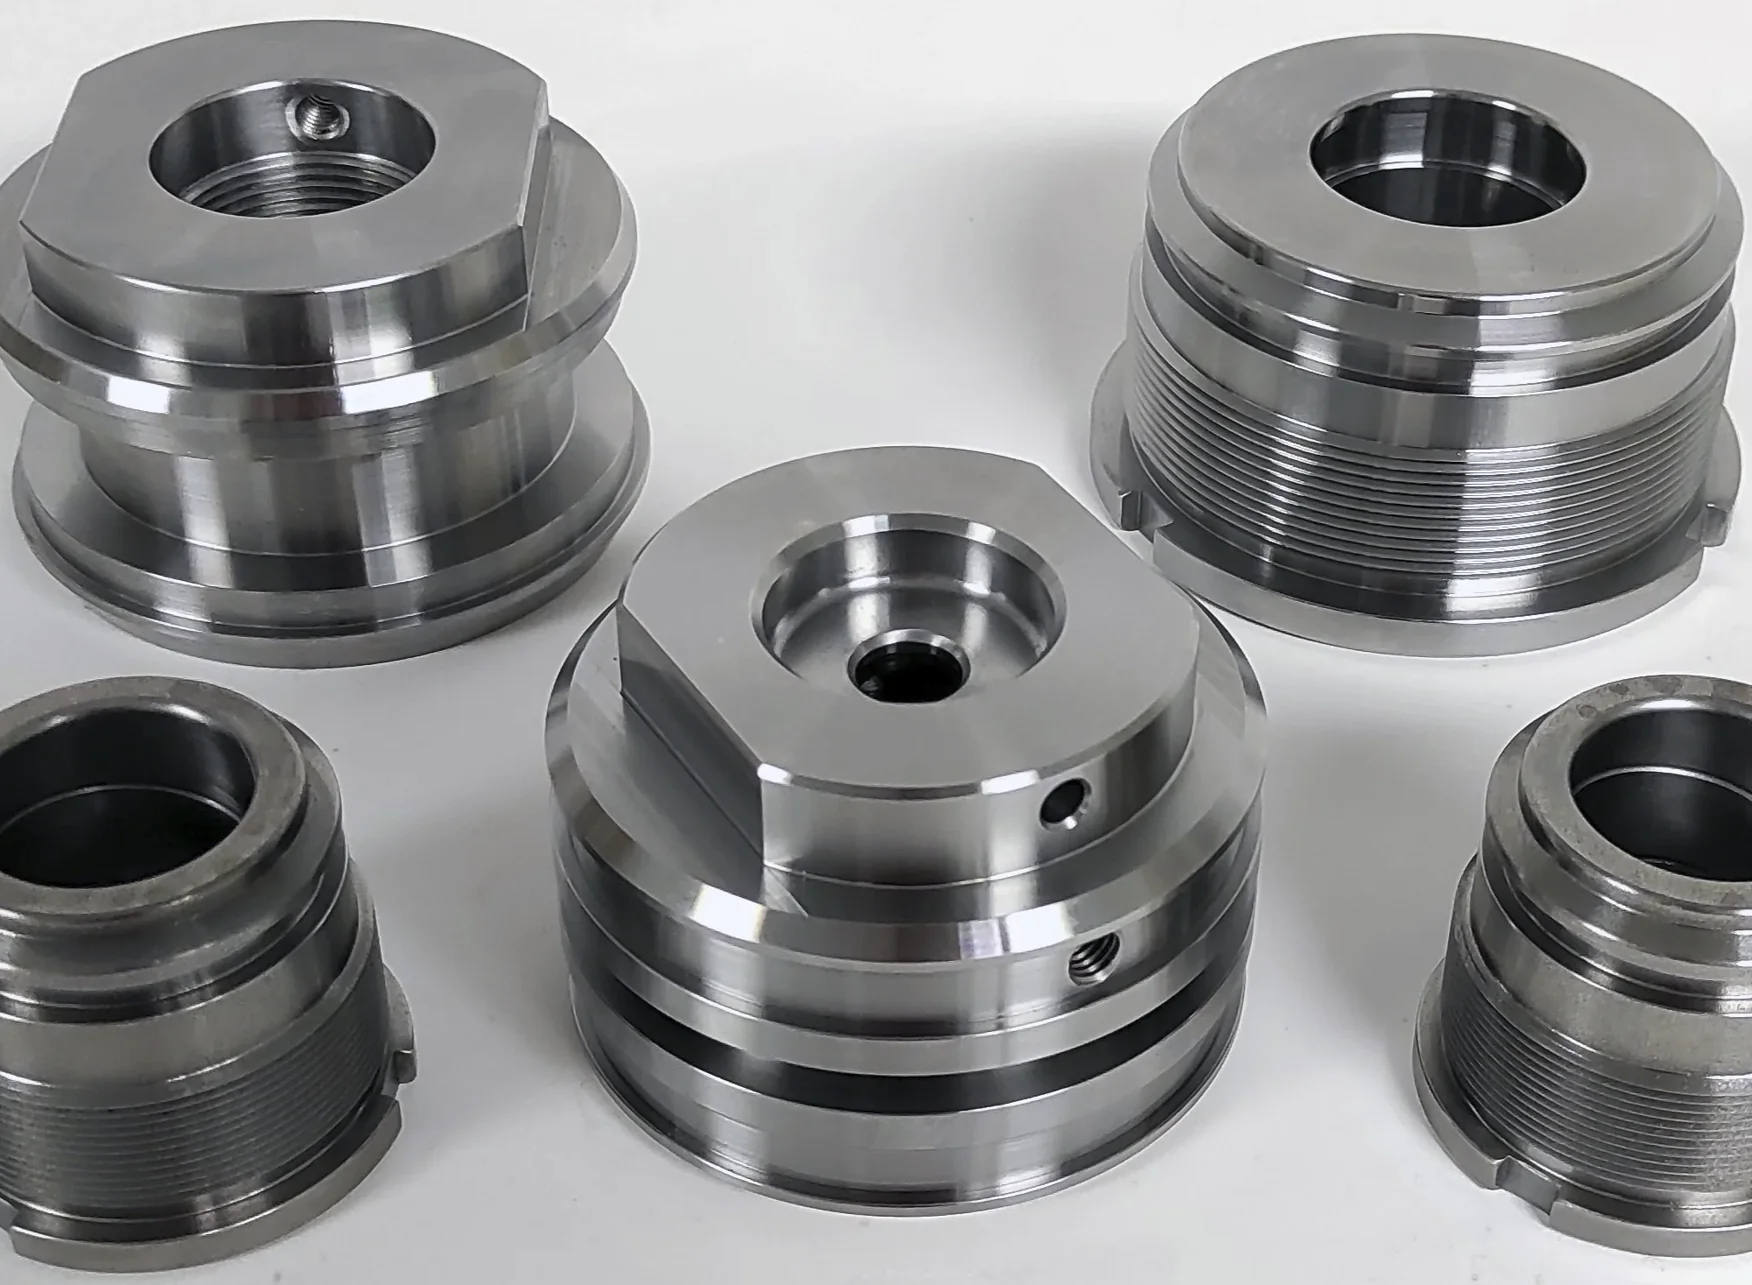
- Large-scale hydraulic cylinder end caps, high-pressure pistons, and heavy valve blocks
- Forging die holder blocks, structural press platen inserts, and robust industrial shear blades
Key Functions
- Dynamic velocity profiling to manage plastic deformation speed and prevent internal structural shearing
- Integrated high-torque bottom ejector circuit for rapid, automated extraction of heavy forged blanks
- Real-time electronic stroke monitoring to ensure identical volumetric displacement across production cycles
Why 1250 Ton Hydraulic Press?
- Supplies the massive compressive force required to thoroughly consolidate the core of thick, large-diameter steel bars
- Four-pillar guiding architecture effortlessly absorbs off-center shock loads, protecting large molding dies from premature cracking
02 — Technical Specifications
SM 1250 HP – HYDRAULIC PRESS MACHINE COMPLETE TECHNICAL DATA
The SM 1250 HP hydraulic press delivers powerful compression capacity and strict structural alignment required for forming heavy industrial rollers. Its high-volume hydraulic layout and rugged column guidance ensure uniform density across thick sections and excellent volumetric part consistency.
Capacity
- Maximum continuous hot forging compression force capacity of 12500 kN
- Dedicated heavy duty bottom ejector stripping force capacity of 1000 kN
Structural Design
- High fatigue resistant pre stressed four column configuration built for high volume production
- Finite element analysis structural simulation frame designed to absorb intense thermal shocks
Frame Type
- Precision aligned solid induction hardened pillar frame guide structure
- Stress relieved heavy welded steel plate bolster and upper moving slide assembly
Hydraulic System
- High output variable displacement axial piston pump fluid power assembly
- Multi stage high capacity offline oil filtration loop with integrated oil coolers
Main Ram Stroke
- Maximum vertical slide forming travel distance capability of 850 mm
- Electronic stroke length limitation positioning resolution accurate within 0.05 mm
Working Hydraulic Pressure
- Maximum continuous operating main hydraulic system fluid pressure of 315 bar
- Peak shock safety valve pressure relief calibration threshold limit of 350 bar
Daylight Gap
- Maximum open vertical daylight window working clearance of 1450 mm
- Minimum closed shut die height tool workspace space of 600 mm
Approach Speed
- Accelerated downward advance slide rapid travel speed of 260 mm/Sec
- Controlled high temperature tool engagement deceleration velocity of 15 mm/Sec
Pressing / Drawing Speed
- Dynamic high pressure hot forging compression speed of 8 to 35 mm/Sec
- Maximum resistance continuous metal displacement squeezing velocity of 40 mm/Sec
Return Speed
- High speed upward ram extraction retraction travel speed of 230 mm/Sec
- Ultra fast automated hydraulic pre return system decompression cycle timing
Bed / Platen Size Platen
- Total clear bolster bed width left to right of 1500 mm
- Total clear bolster bed depth front to back of 1300 mm
Columns
- Ultra high tensile forged alloy steel pillar diameter of 300 mm
- Heavy duty heat resistant bronze guide bushings with automatic grease lubrication
Working Envelope
- Total horizontal internal clear workspace area of 1500 by 1300 mm
- Maximum permissible upper die tool assembly mass weight of 11000 kg
Control System
- Industrial programmable logic controller linked with a graphical touchscreen station
- Dual redundant non contact linear transducer position tracking systems accurate within 0.02 mm
Main Motor Power
- High efficiency primary hydraulic pump electric drive motor power of 132 kW
- Dedicated auxiliary cooling and continuous oil filtration motor power of 18 kW
Valves & Hydraulics
- High dynamic response proportional servo flow control cartridge manifold block
- Integrated fast acting overhead gravity pre fill oil valve unit assembly
Automation
- Digital interface connection ports for synchronized industrial robotic billet handling manipulators
- High temperature hydraulic quick action die clamping system connecting lines
Safety Features
- Heat shielded front and rear dual channel infrared light curtain barriers
- Automated heavy duty dual fail safe mechanical anti drop ram safety locking blocks
SM 1250 HP — Model Specifications
- Nominal Force: 12500 KN
- Maximum Hydraulic Pressure: 25 MPa
- Max Opening Height of the Slider: 1500 mm
- Max Stroke of the Slider: 900 mm
- Effective Bed Size: 1600 × 1600 mm
- Slider Down Speed: 180 mm/s
- Slider Pressing Speed: 6–15 mm/s
- Slider Return Speed: 200 mm/s
- Ejector Cylinder Nominal Force: 600 KN
- Stroke of the Ejection Cylinder: 300 mm
03 — Die / Mold System
Precision Hot Forging Heavy Duty Industrial Rollers Die Mold Engineering
This precision tooling system integrates high-durability open and closed-die configurations designed to withstand extreme thermal loading during heavy-section roller formation. The reinforced structure actively resists high-impact splitting pressures to secure tight geometric shapes under continuous industrial production.
Technical Specifications (Tooling)
Die Type
- Heavy duty progressive closed die hot forming tool set featuring optimized blocker and cylindrical finisher profiles
- High impact precision industrial tooling layout engineered for high stress machinery wear components
Die Materials
- Premium hot work steel matrix formulation containing high chromium and vanadium elements for thermal stability
- Advanced cobalt base impact resistant cladding alloys deposited over critical high friction radius zones
Tool Configuration & Construction
- Modular split block insert container system engineered to absorb extreme lateral metal flow pressures
- Heavy duty pre stressed die holder block assembly optimized for rapid mechanical crane loading procedures
Key Tooling Features
- Dual acting high pressure mechanical ejector pins for clean and immediate component stripping sequences
- Internal deep cooling lines designed to regulate core die temperatures and prevent heat checking defects
Alignment Accuracy
- Upper and lower die half mismatch mismatch deviation kept strictly under a limit of 0.200 mm
- Precision guide column geometric concentricity variation restricted within a tolerance of 0.030 mm
Process Materials
- Medium carbon structural steels high carbon wear resistant alloys and chrome manganese steel bars
- Premium heavy engineering structural forging metals matching international industrial machine component standards
Surface Finish
- Active molding cavity internal profiles precision ground and polished down to Ra 0.80 microns
- Thermally stable gas nitrided wear protective surface layer applied to a depth of 0.300 mm
Tool Life
- Expected production span of 8000 cycles before requiring mandatory cavity reconditioning procedures
- Total structural tooling lifespan capacity reaching 60000 production cycles before complete replacement
Precision Hot Forging Heavy Duty Industrial Rollers Die Mold
04 — Product Application
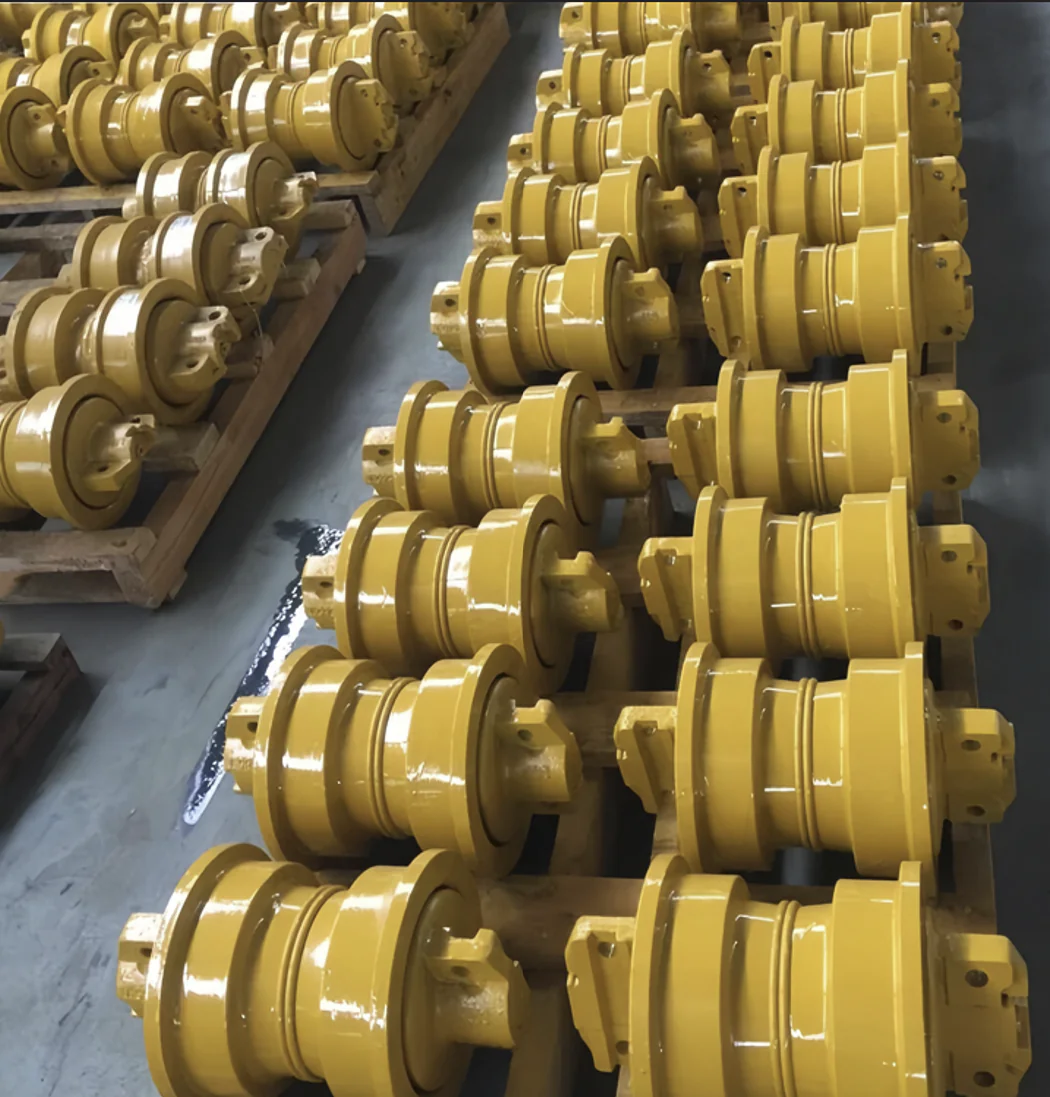
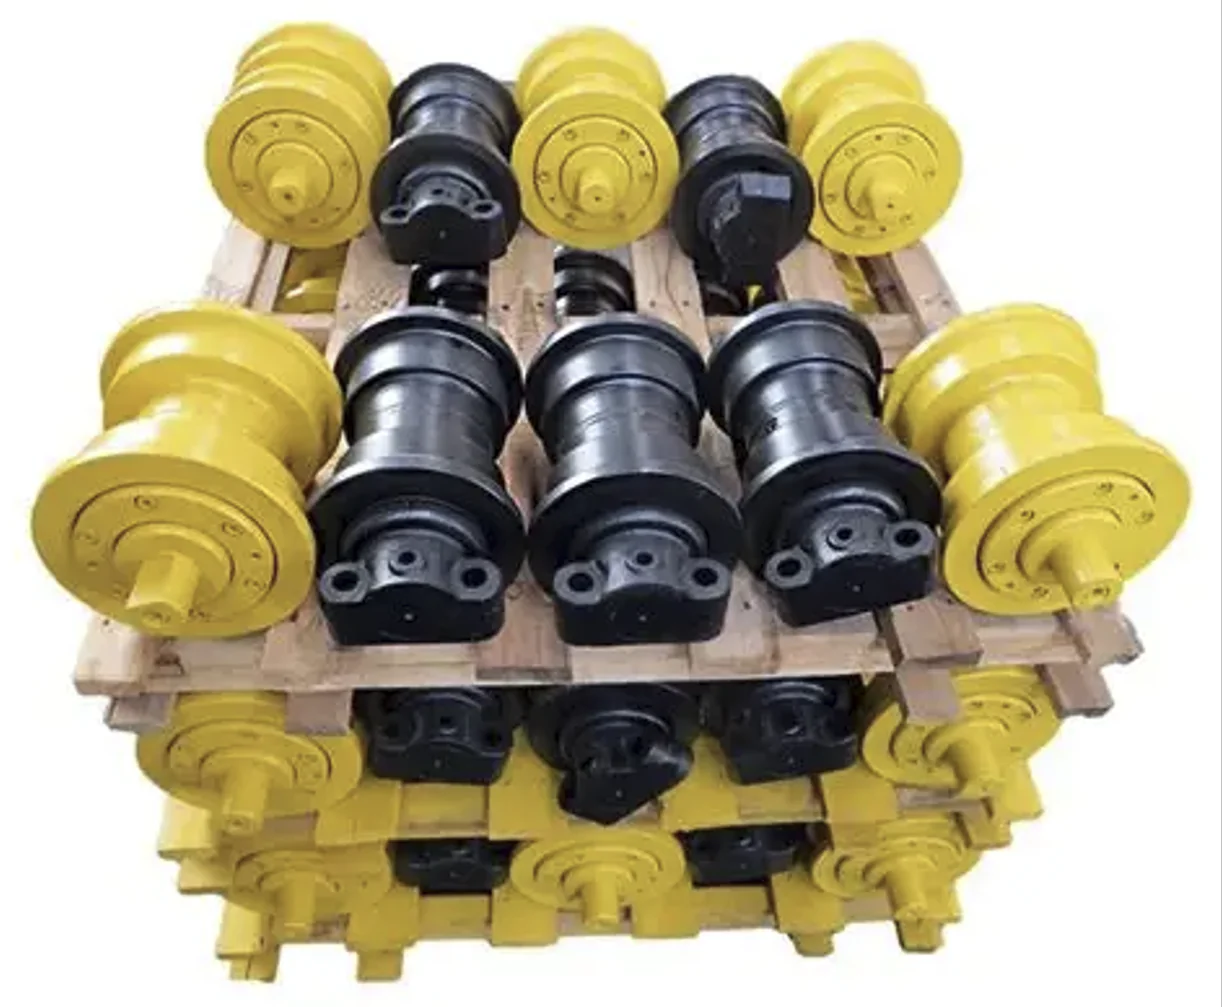
Where Precision Hot Forging Heavy Duty Industrial Rollers Are Used
Precision hot forged heavy-duty industrial rollers provide the high-strength cylindrical foundations required to support immense structural weights and continuous material handling. These dense, wear-resistant forgings are engineered to operate reliably under relentless surface friction, severe crushing forces, and debris-heavy industrial environments.
Industry Applications
These rugged industrial forgings are critical across the global steel manufacturing, heavy open-pit mining, bulk materials logistics, and infrastructural engineering sectors. Their high surface hardness, uniform internal density, and precise near-net geometries allow plant operators to achieve high machine uptime, lower hourly maintenance costs, and extend overall equipment lifespans.
Steel Rolling Mills and Metal Processing Facilities
Forged backup rolls, work rolls, and heavy guide rollers run continuously within hot and cold steel strip reduction mills. Their deep microstructural consolidation prevents surface spalling and structural breakdown under the immense, crushing roll-bite forces needed to flatten sheet metals.
Heavy Mining, Excavation, and Earthmoving Equipment
Robust track rollers, idler assemblies, and load-bearing carrier rollers form the primary undercarriage systems of massive tracked excavators and bulldozers. The directional grain flow developed during forging eliminates internal flaws, ensuring these rollers can support hundreds of tons of machinery traversing jagged, unpaved rock terrains.
Industrial Conveyors and Bulk Material Handling Infrastructure
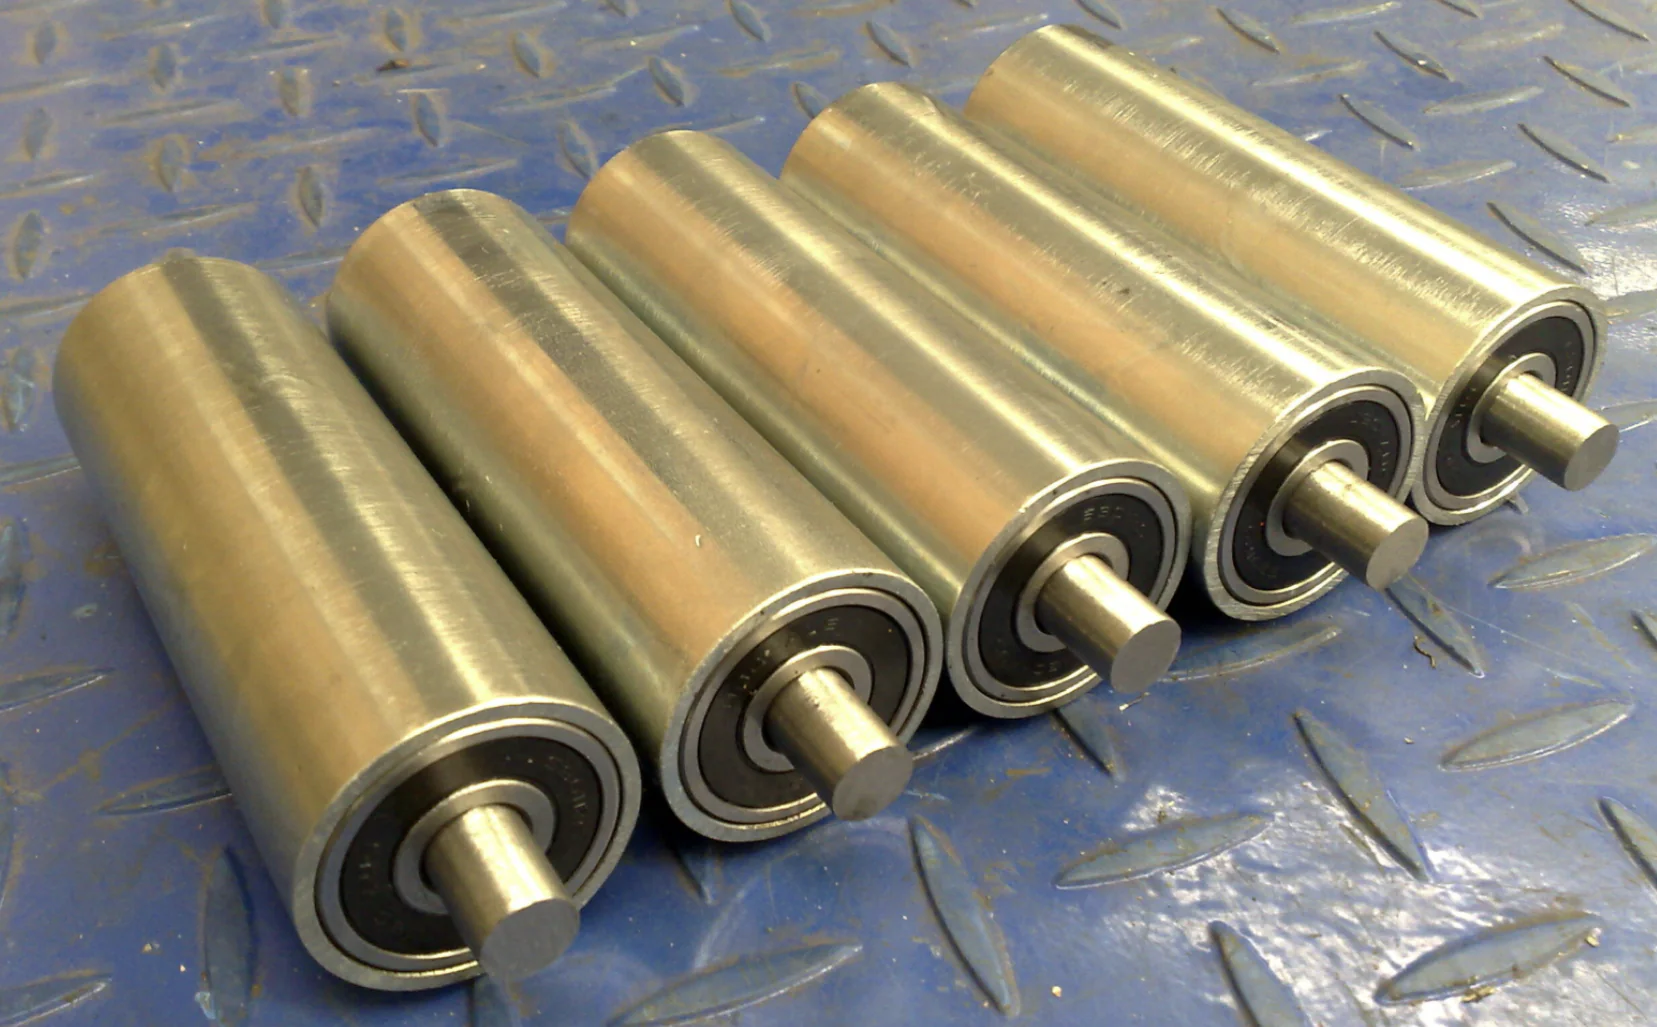
High-capacity conveyor pulley shafts and heavy-duty drive rollers move thousands of tons of raw ore, coal, and crushed aggregates daily. The exceptional structural integrity prevents abrupt fatigue cracking under constant belt tension, securing non-stop logistical operations across ports, mines, and shipping terminals.
Heavy Infrastructure, Marine Docking, and Construction Machinery
Massive cylindrical roller bearings, crane track wheels, and heavy bridge expansion rollers facilitate controlled structural displacement and heavy load movement. The dense metal matrix provides high flattening resistance, allowing these components to carry extreme, static structural dead-weights without developing surface flat spots.
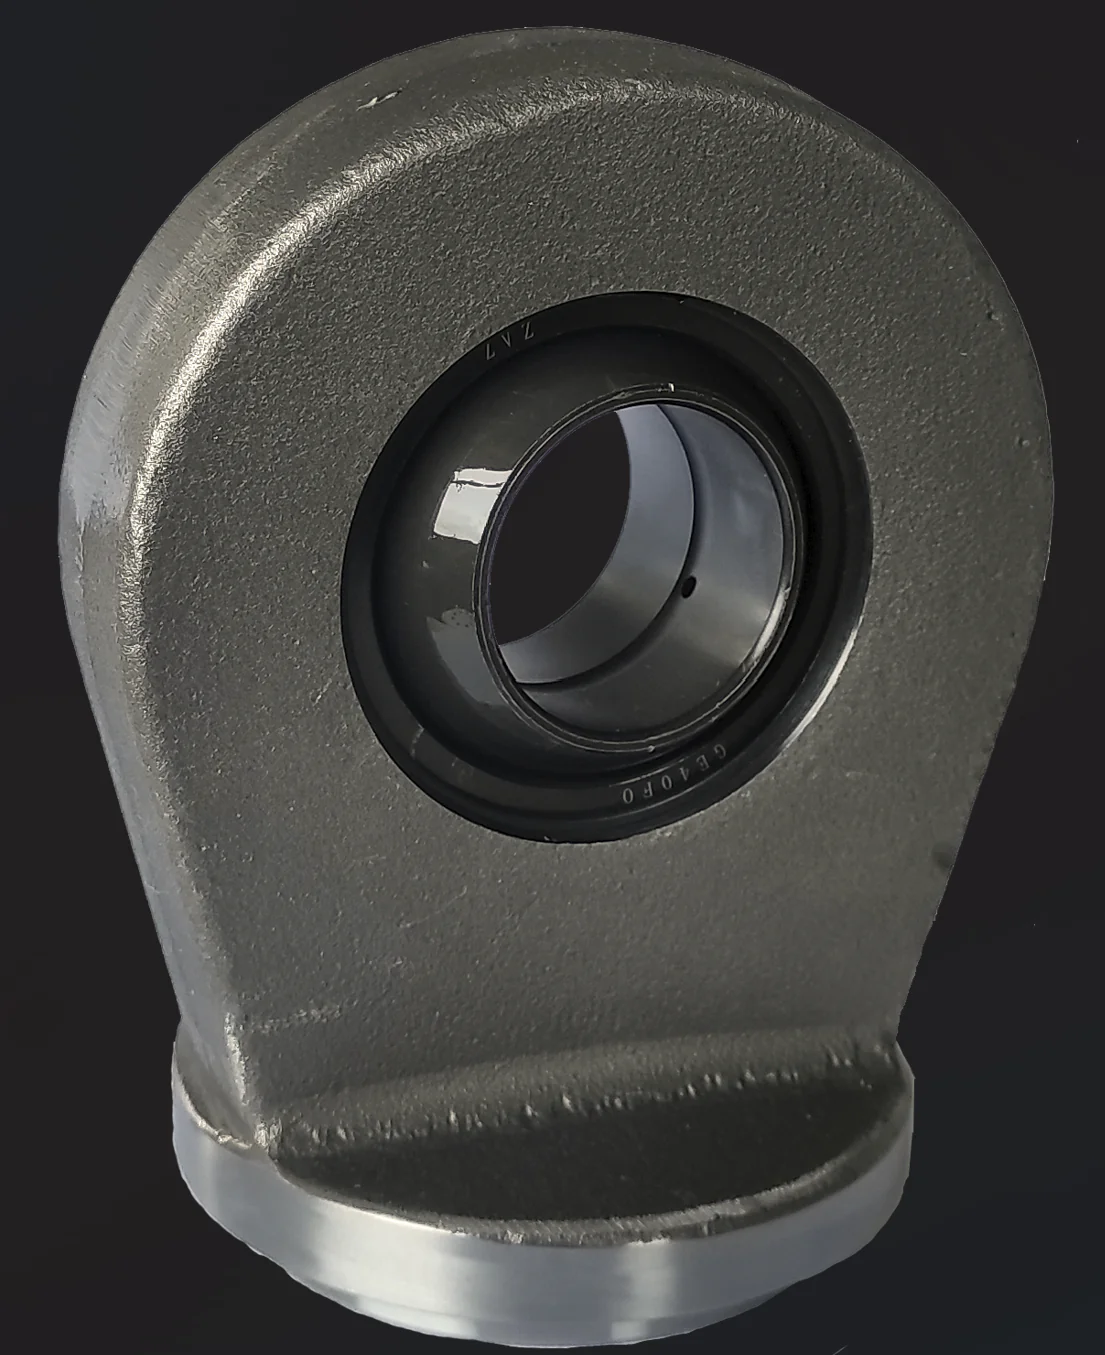
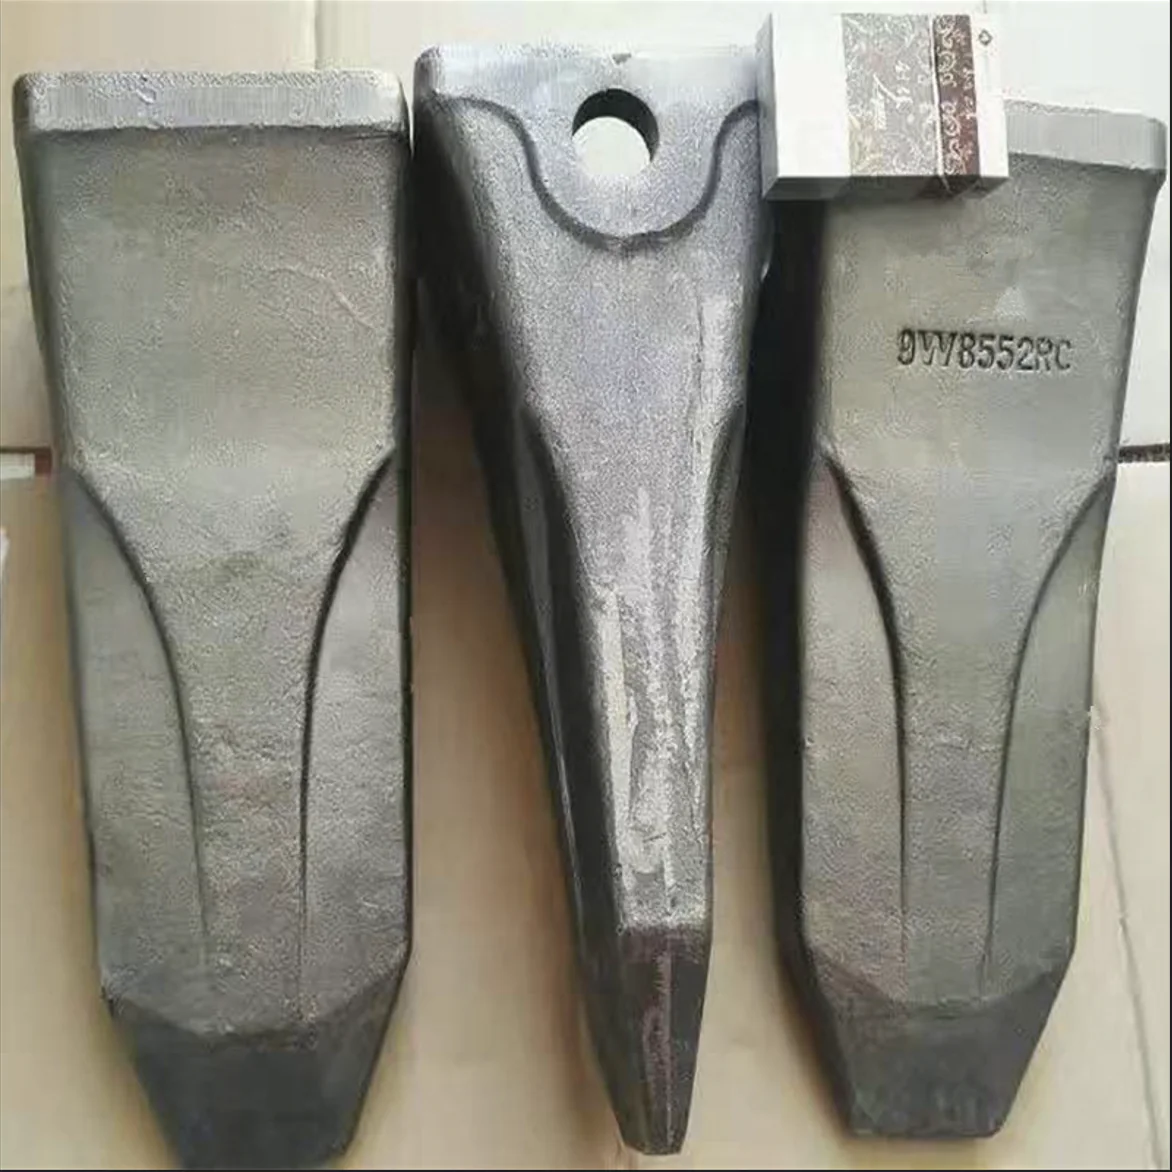
Finished Product Gallery
05 — Key Advantages
Why Choose the 1250-Ton Sinter Hydraulic Press
The 1250-Ton Sinter Hydraulic Press provides the uniform load distribution and deep pressure penetration required to thoroughly consolidate thick-section steel rollers. Its rigid guiding framework, customizable pressing profiles, and high-efficiency fluid power systems deliver consistent structural density, low machining allowances, and rapid commercial processing cycles.
Technical & Commercial Benefits
High Core Compression Tonnage for Deep Center Consolidation
The robust hydraulic system delivers steady force to compress the deep internal structures of heavy, large-diameter steel billets. Thoroughly closing internal voids and eliminating core porosity prevents mechanical failure under intense industrial load cycles.
Rigid Four-Pillar Structure Restricting Lateral Slide Deviation
The heavy pre-stressed column guidance framework easily counteracts asymmetric forces during complex multi-stage blocker and finisher forging steps. Maintaining strict platen parallelism protects large molding dies from premature chipping and uneven cavity wear patterns.
Multi-Stage Programmable Pressing and Squeezing Speed Profiling
Proportional cartridge valves regulate plastic metal displacement down to specific millimeters per second throughout the active compression stroke. Controlled metal movement allows alloy steels to fill deep cylindrical cavities evenly without developing structural folds.
Integrated High-Tonnage Bottom Hydraulic Ejector Stripping Assembly
A dedicated high-pressure knockout mechanism applies immediate, uniform upward stripping forces to lift dense, heavy forgings out of tight cavities. Rapid mechanical extraction minimizes direct heat transfer from glowing steel to the die steel, preventing thermal cracking.
Excellent Near-Net-Shape Accuracy Reducing CNC Machining Overhead
Dual redundant non-contact linear transducers control the final downward vertical slide travel distance within small fractions of a millimeter. Forging precise outer diameters straight from the press bed saves valuable alloy raw stock and cuts down expensive lathe machining hours.
Fast Decompression Technology Shortening Complete Return Travel Cycles
Specialized fast-acting pre-fill circuit valves bleed off peak hydraulic system pressures instantly to speed up the upper moving slide retraction. Accelerating these processing intervals raises total hourly roller production capacity while lowering net power consumption per unit.