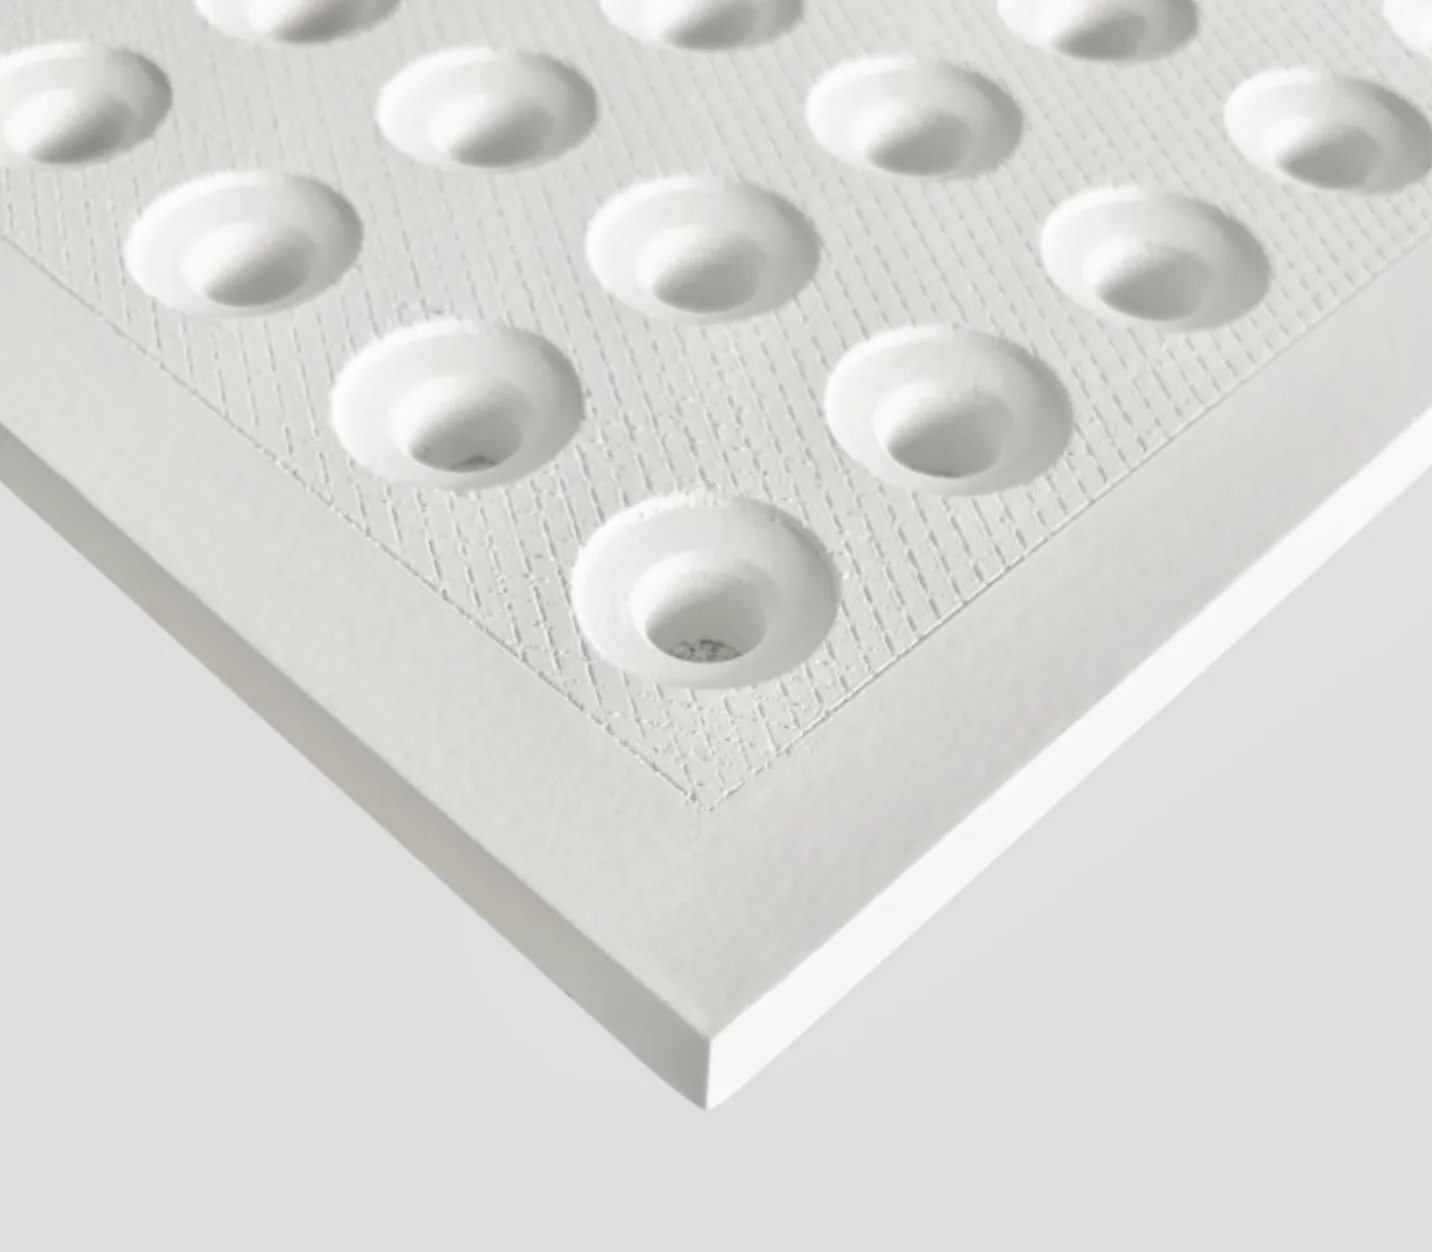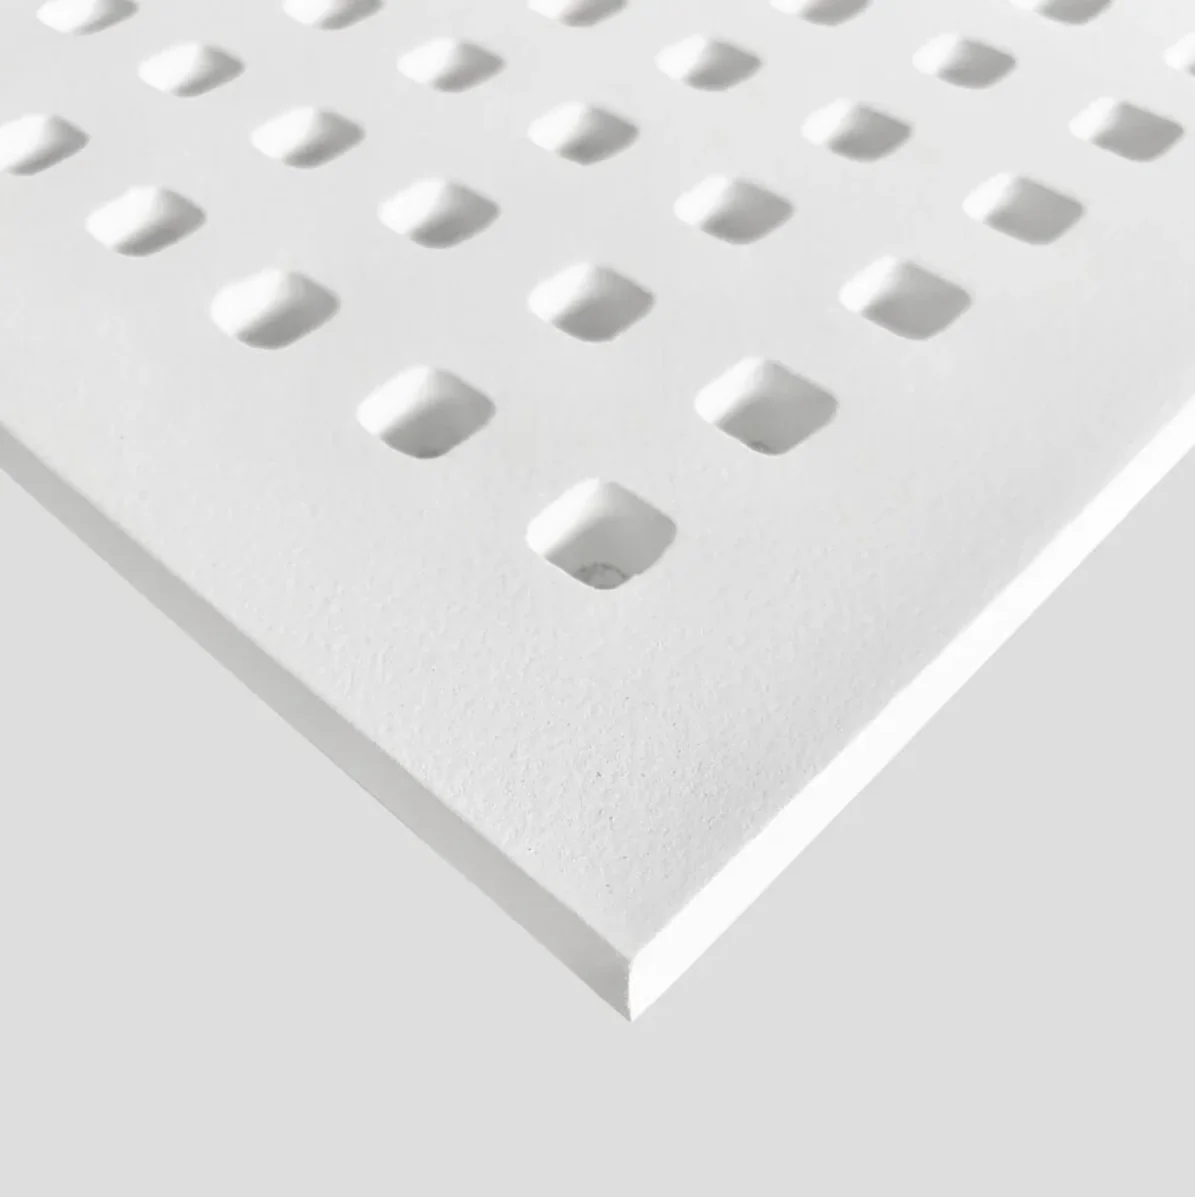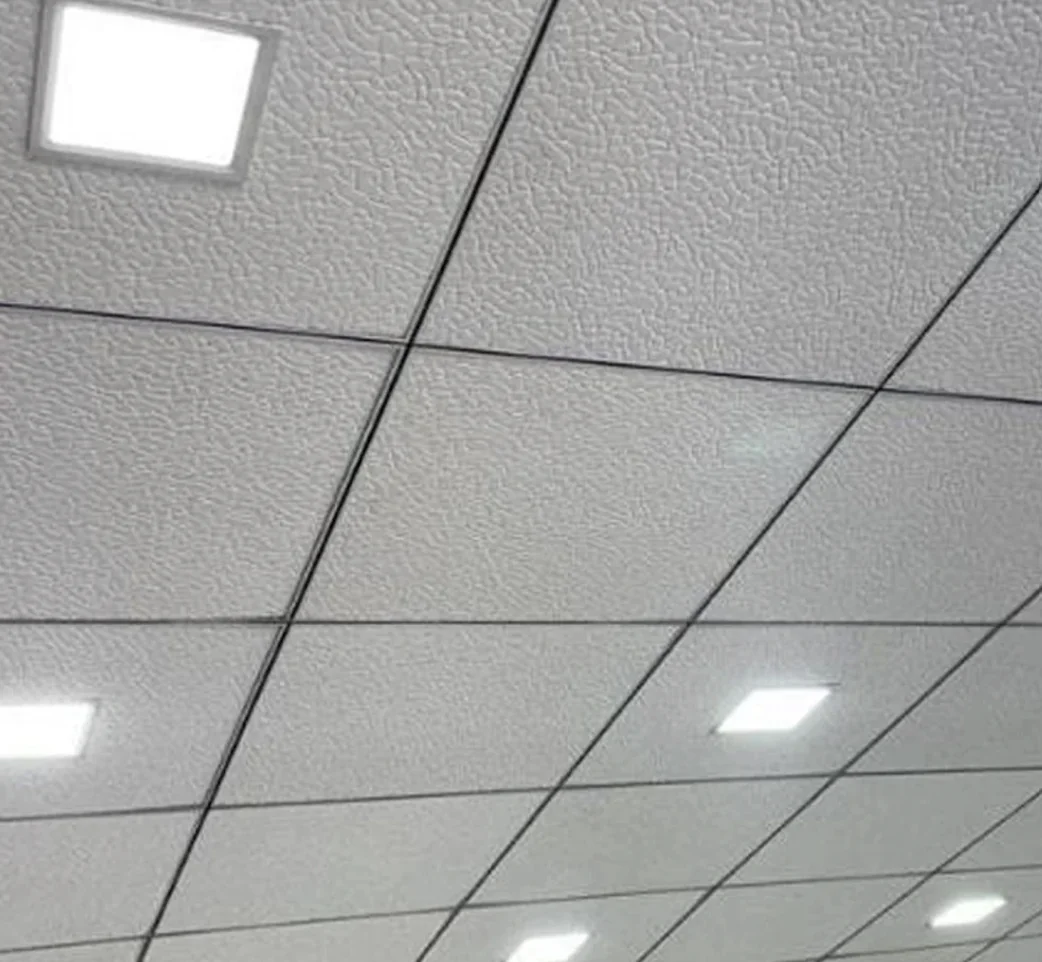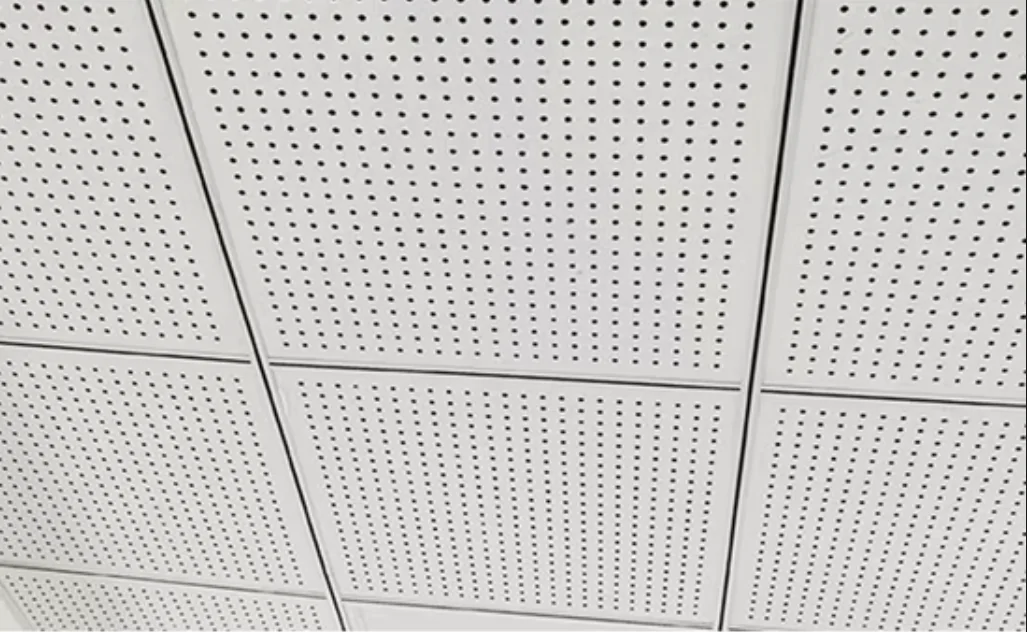
GRG Acoustic Wall & Ceiling Panels 4
GRG Acoustic Wall & Ceiling Panels · Hydraulic Press Machine

400 Ton Four Column Hydraulic Press for GRG Acoustic Wall & Ceiling Panels

400T Rated Capacity
100 mm/s Slider Down Speed
7–12 mm/s Slider Pressing Speed
100 mm/s Slider Return Speed

01 — Press System

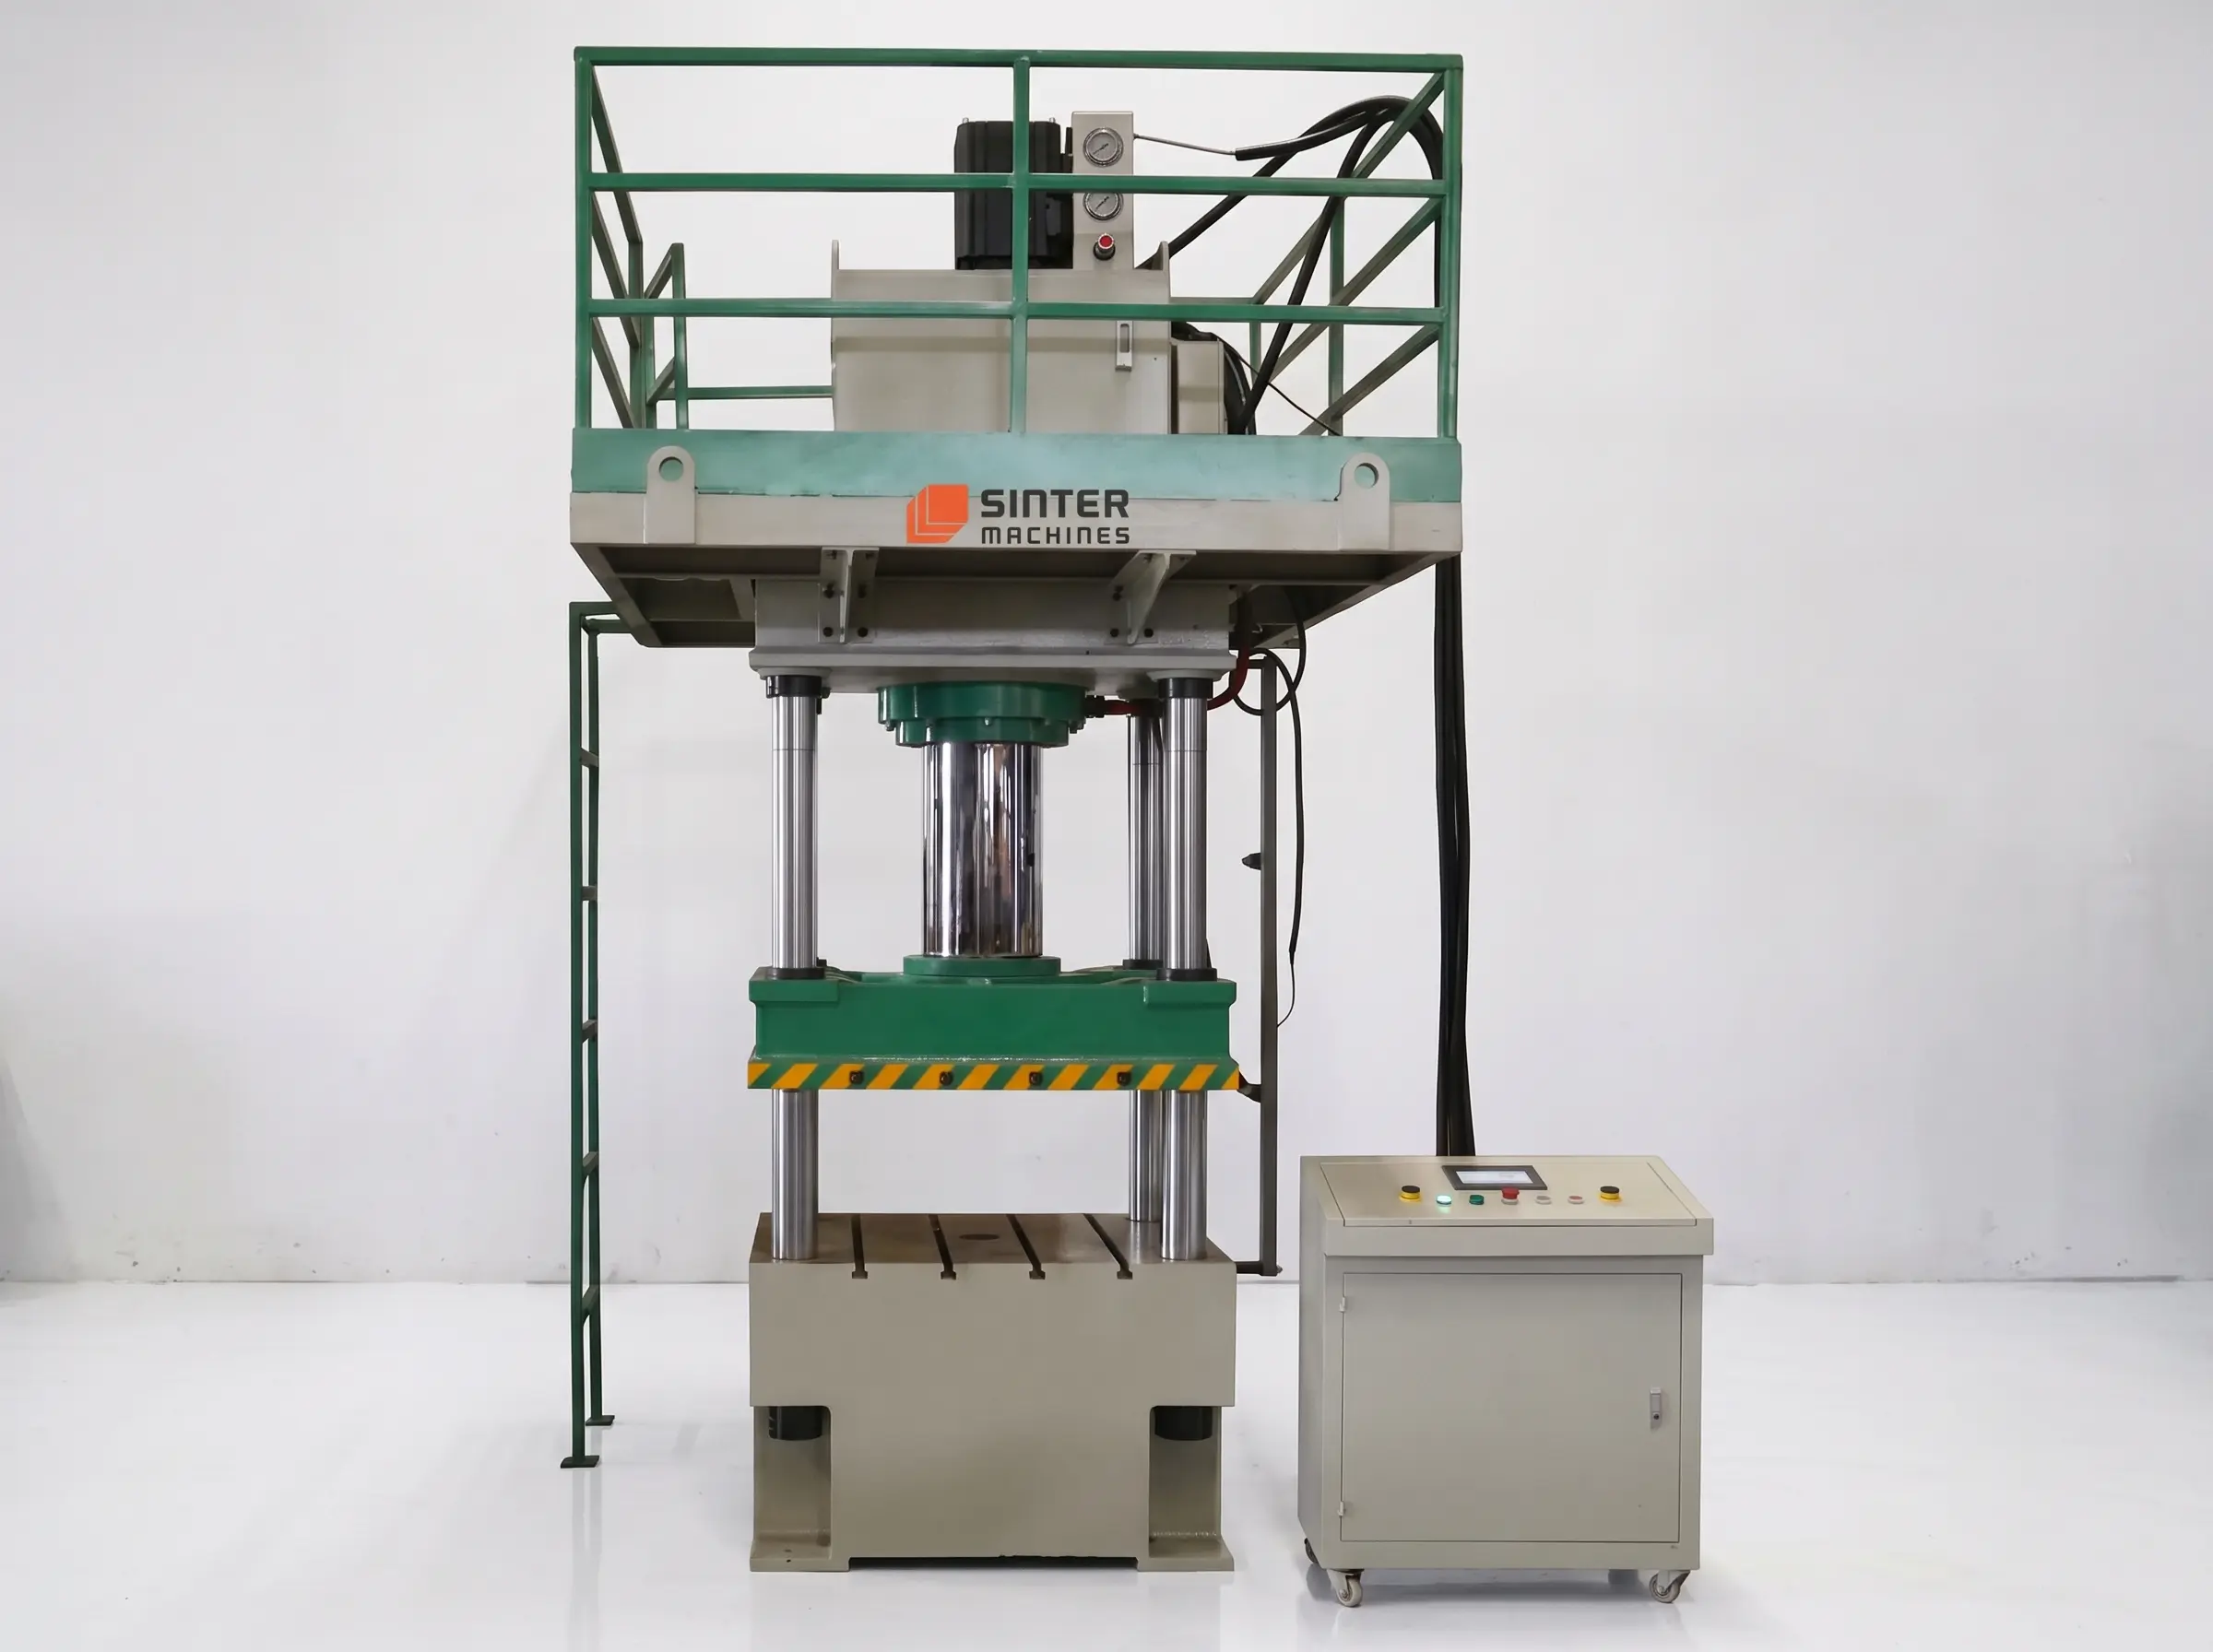
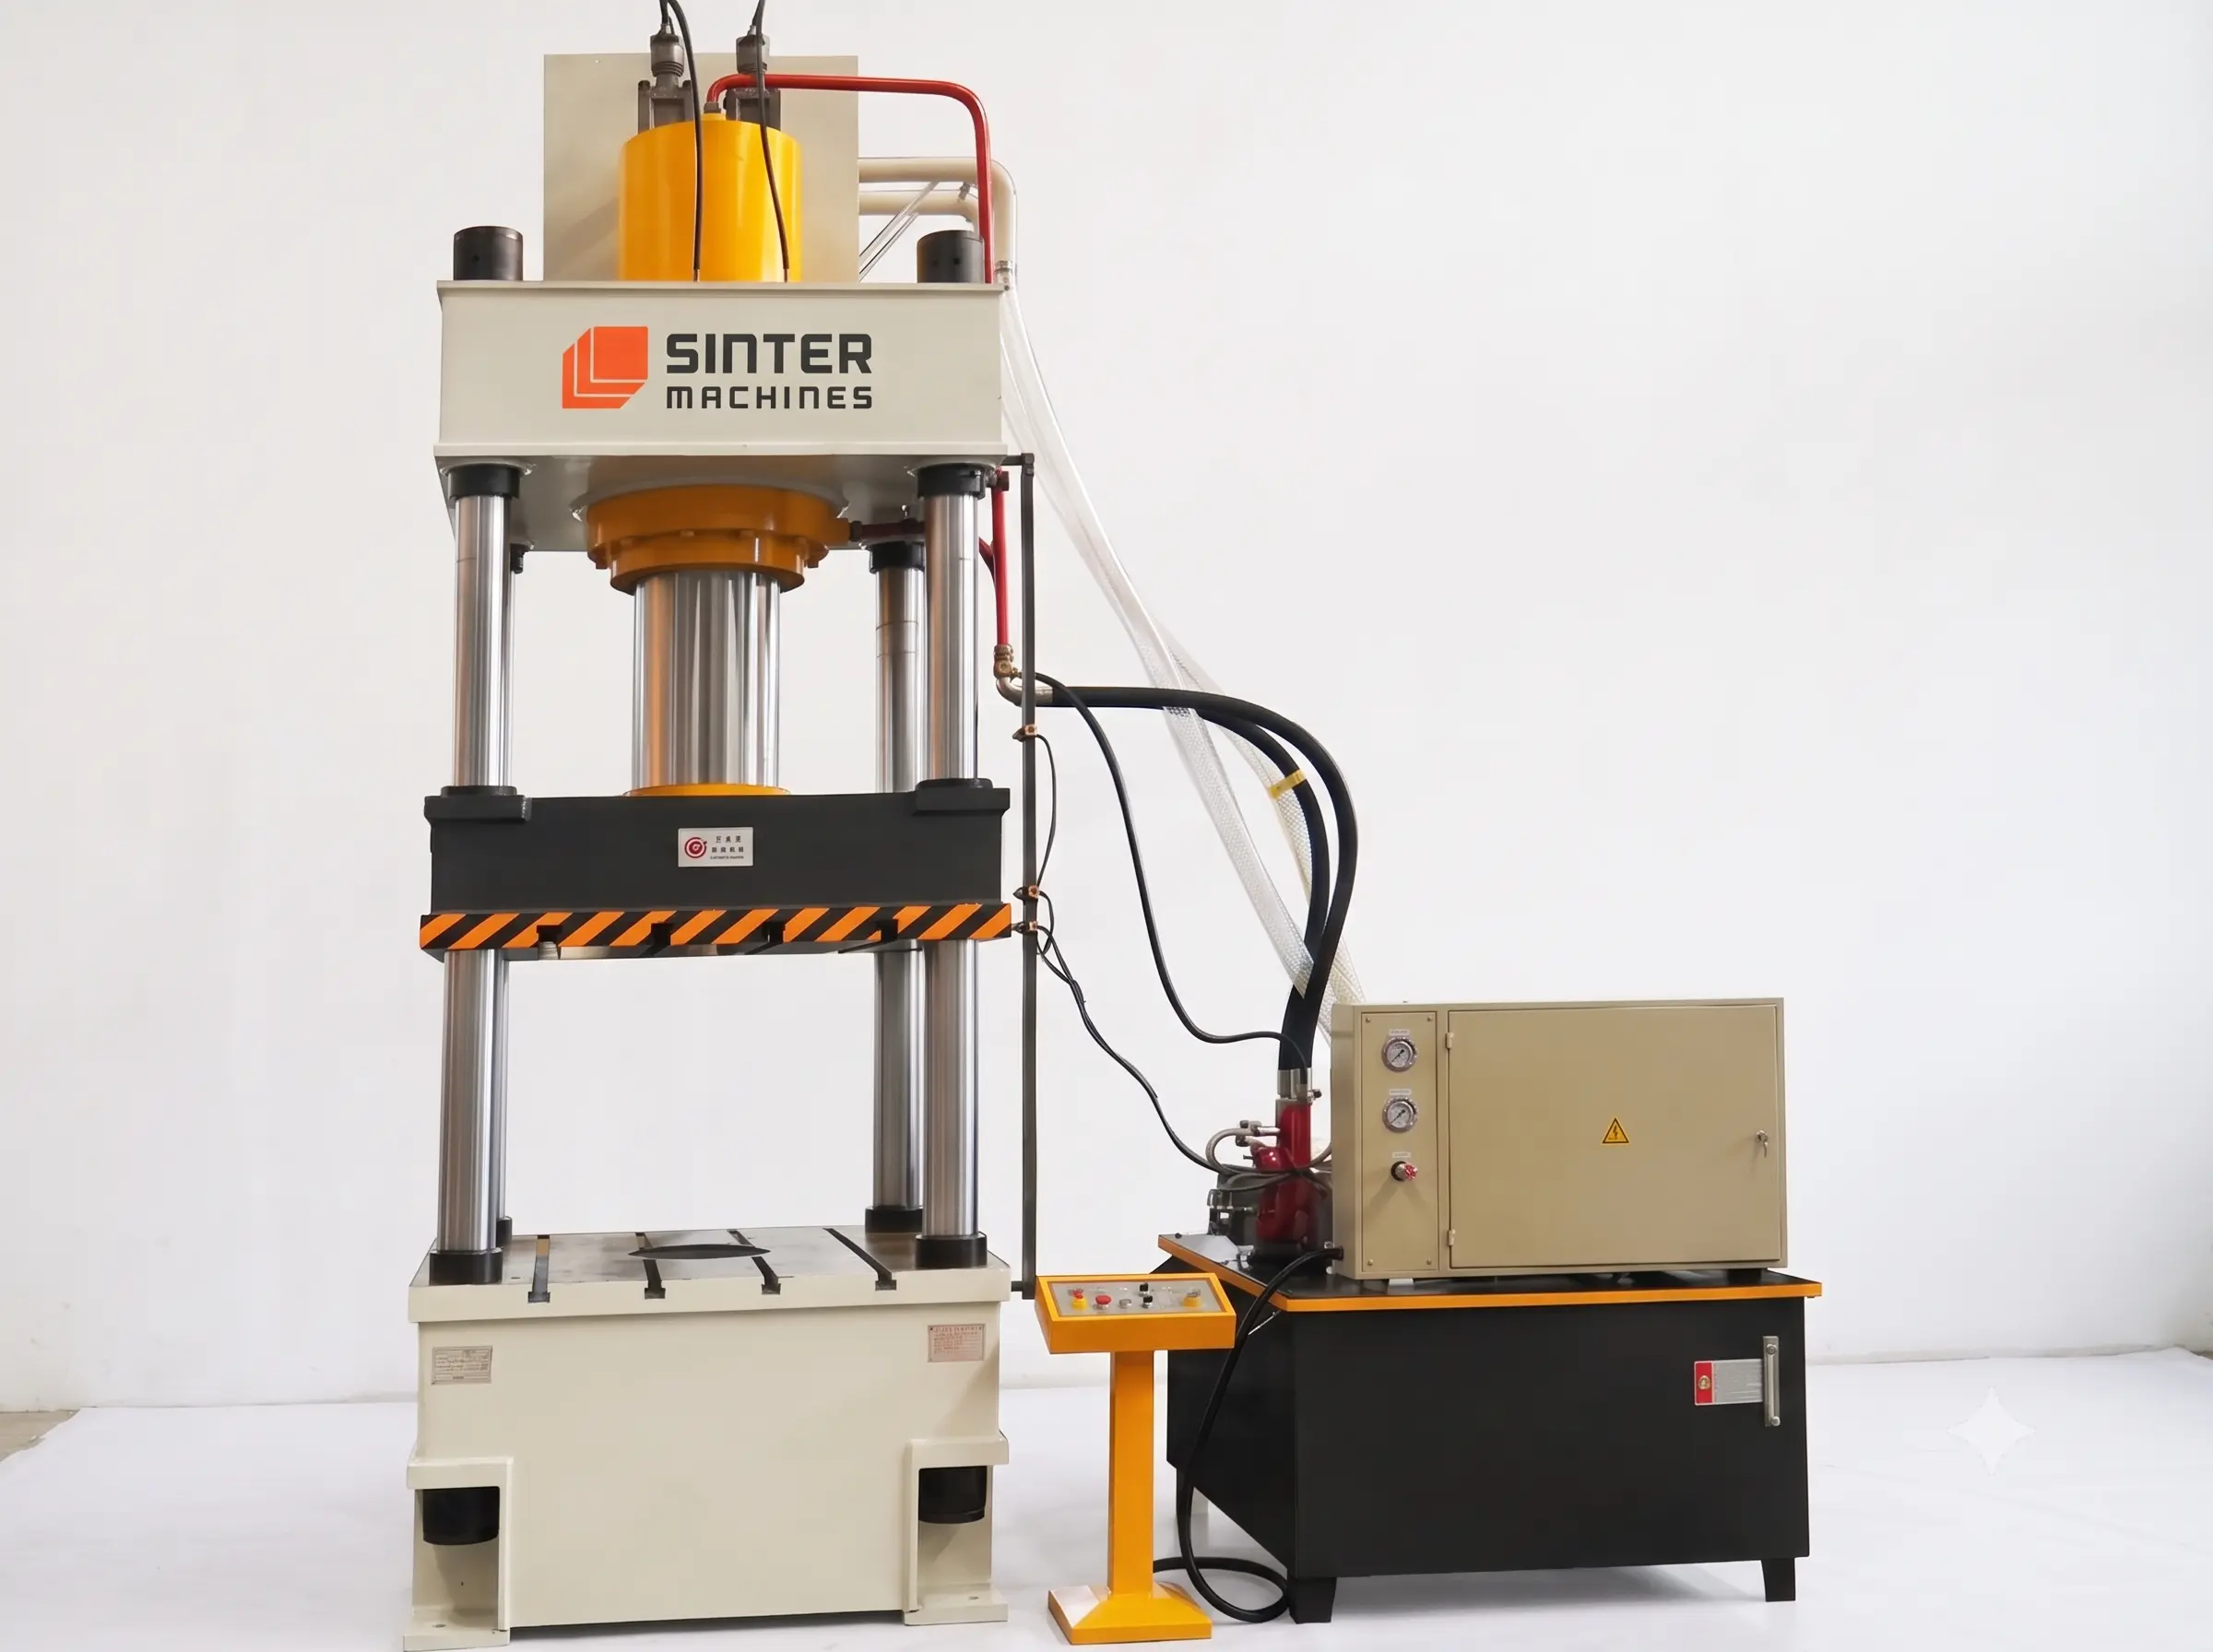
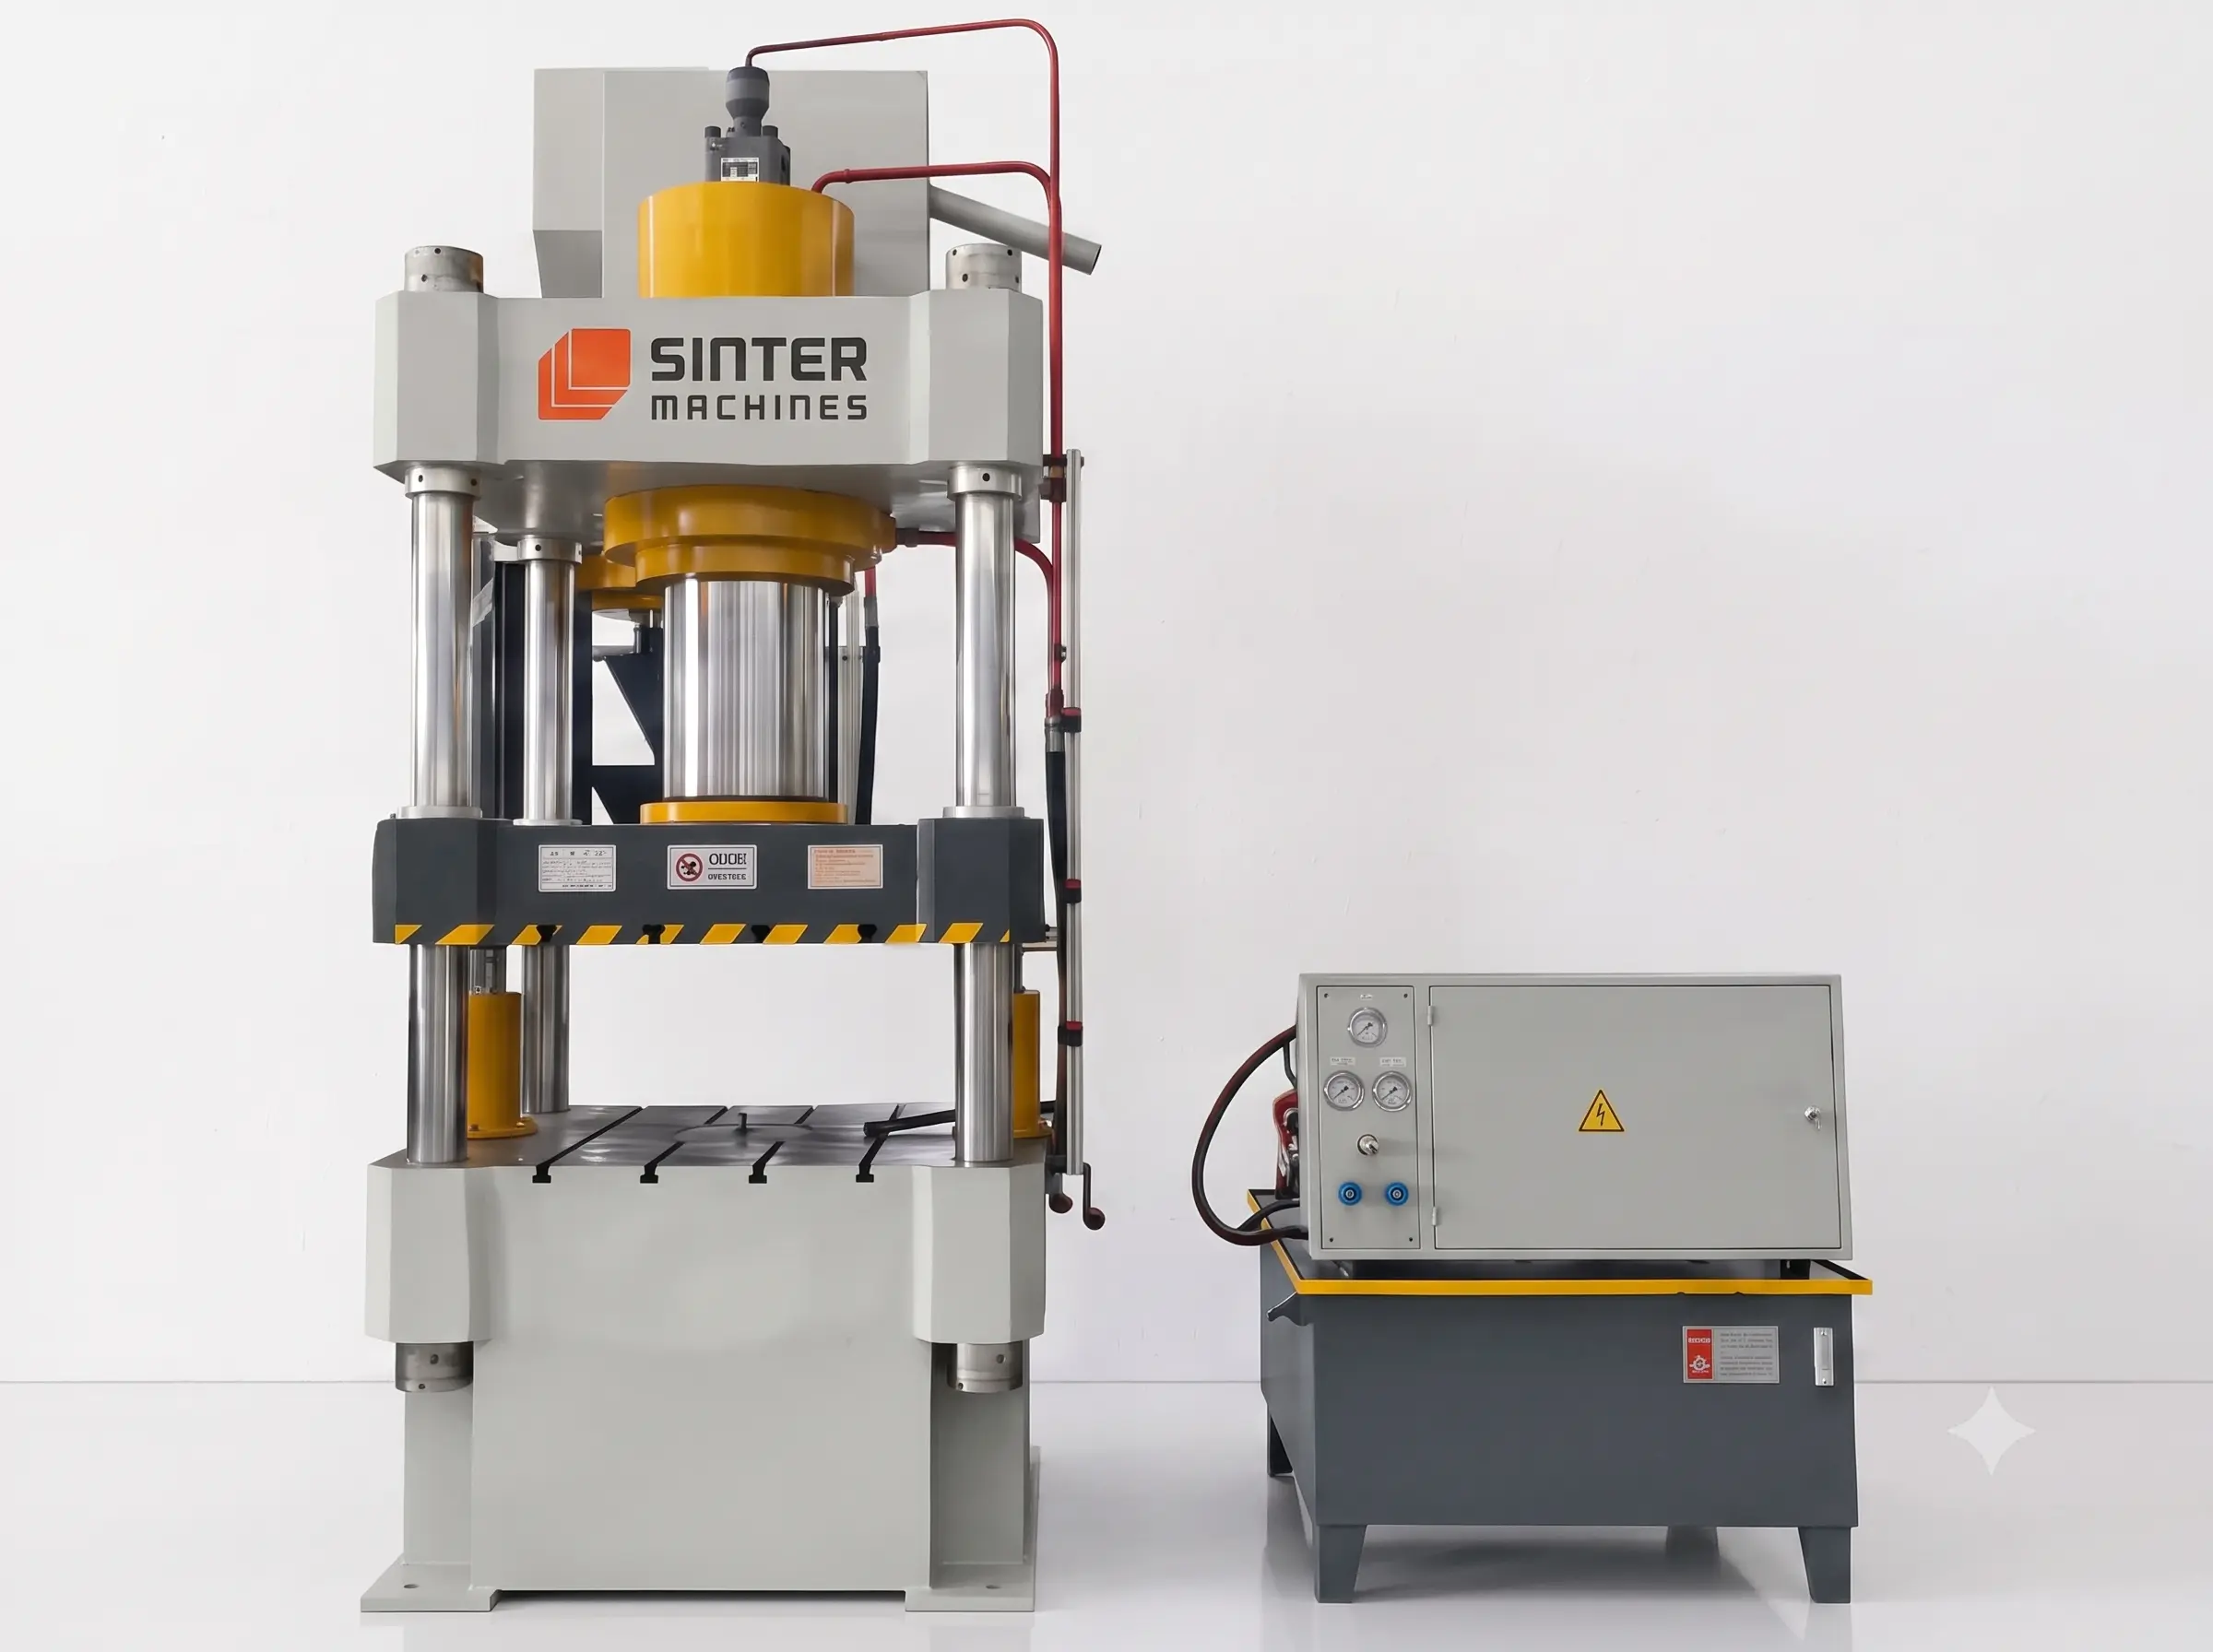
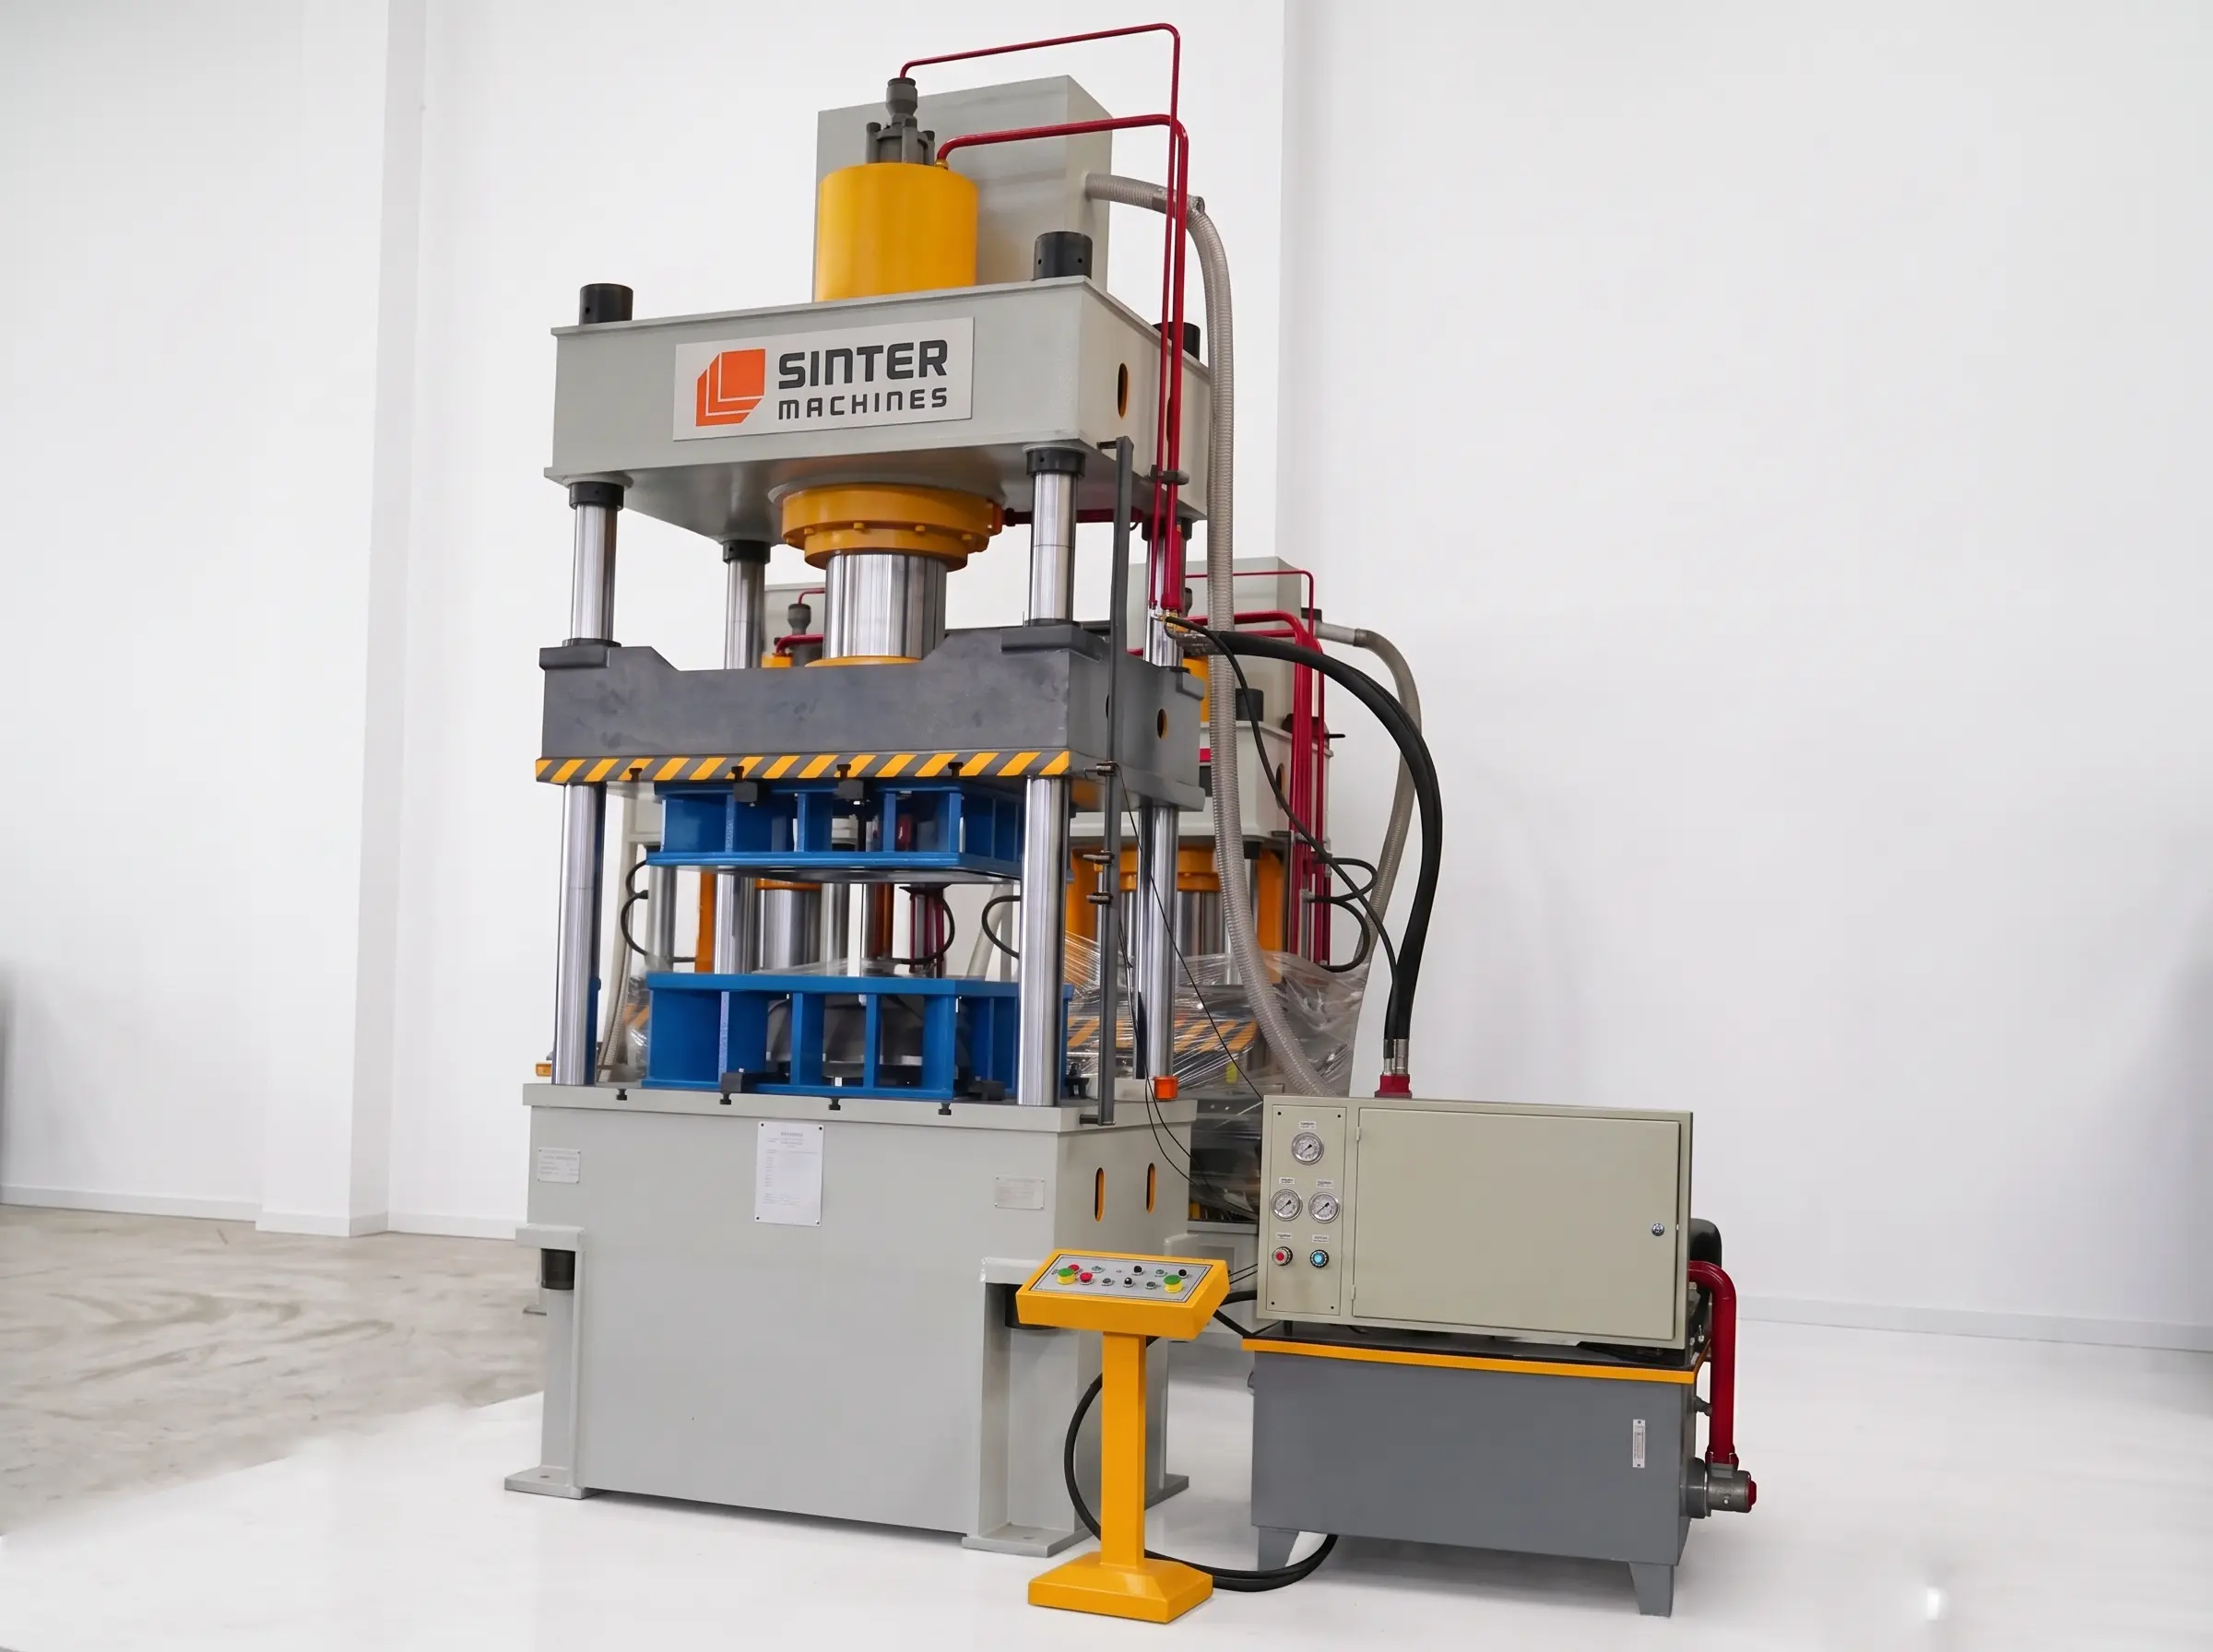
400 Ton Four Column Hydraulic Press Machine

The 400-ton four-pillar hydraulic press from Sinter Hydraulics India is an ideal system for GRG acoustic panel manufacturing, delivering high-quality sound-absorbing panels, excellent surface and dimensional precision, stable acoustic performance across batches, and scalable production for commercial and architectural projects. Built with a rigid pre-stressed four-column frame and programmable pressure ramping, it ensures dense, defect-free gypsum-fiber composite compaction without micro-cracking delicate patterns.

Use Case

The 400-ton four-pillar hydraulic press is designed for precision molding and compaction of GRG acoustic panels, which are widely used in acoustic ceilings, sound-absorbing wall panels, and perforated decorative panels for noise control. Processing high-strength gypsum slurry, glass fiber mats or chopped fibers, and acoustic-grade additives, the press compacts gypsum uniformly after slurry pouring and layering to boost density, ensure uniform thickness for consistent sound absorption, and produce sharp perforations with clean decorative edges.

Core Applications

  • High-density compression molding and compaction of perforated and textured GRG acoustic wall cladding and ceiling panels
  • Precision stamping of sound-absorbing architectural panels with integrated micro-perforations, slots, and 3D acoustic diffusers
  • Heavy-duty molding of large-format acoustic panels requiring uniform structural density, flat margins, and precise thickness control

Material

  • High-purity alpha gypsum slurry mixtures enhanced with water-reducing polymers, setting regulators, and acoustic binders
  • Woven alkali-resistant (AR) glass fiber mesh layers, E-glass fiber mats, and chopped glass strand reinforcement
  • Lightweight acoustic aggregates, fire-retardant mineral additives, and sound-damping viscoelastic polymer compounds

Typical Products Processed

  • Micro-perforated and slotted GRG acoustic wall panels equipped with rear sound-absorbing mineral wool or fleece backings
  • Large-format 1200 x 600 mm and custom architectural 3D acoustic wall cladding systems for auditoriums and concert halls
  • Sound-diffusing ceiling baffles, curved acoustic reflectors, and decorative noise-control panels for corporate auditoriums

Key Functions

  • Multi-stage hydraulic pressure compaction to thoroughly bleed out air voids and eliminate internal micro-porosity in the gypsum matrix
  • Controlled slow-closing slide motion to prevent glass fiber displacement, slurry distortion, or pin shearing during compaction
  • Precision dwell pressure control at bottom dead center to set structural density and ensure uniform thickness for stable acoustic performance
  • Automated hydraulic ejector pin actuation providing gentle, crack-free demolding of wet green-state acoustic panels with clean perforations

Why 400 Ton Hydraulic Press?

  • Generates 400 tons of uniform, controlled hydraulic force required to fully compact large-surface acoustic slurries without damaging fine perforation pins
  • Heavy four-column guide structure maintains exact platen parallelism, ensuring zero thickness variation across large panels for predictable acoustic attenuation

02 — Technical Specifications

SM 400 HP – HYDRAULIC PRESS MACHINE COMPLETE TECHNICAL DATA

The SM 400 HP heavy-duty hydraulic press delivers high-density compaction force and precise parallel platen guidance tailored for large-format GRG acoustic panel molding. Its rigid four-column architecture and multi-stage pressure ramping eliminate internal air voids, protect fine perforation pin matrices, and ensure absolute panel flatness.

Capacity

  • Maximum continuous compression molding force capacity of 4000 kN
  • Dedicated hydraulic bottom ejector force capacity of 800 kN

Structural Design

  • Heavy stress relieved four column guide structure engineered for precise parallel compression molding
  • FEA stress relieved heavy steel plate welded bolster and upper moving platen assembly

Frame Type

  • Precision aligned solid induction hardened pillar frame guide structure
  • Stress relieved heavy welded steel plate bolster and upper moving slide assembly

Hydraulic System

  • High output variable displacement axial piston pump fluid power assembly
  • Multi stage high capacity offline oil filtration loop with integrated oil coolers

Main Ram Stroke

  • Maximum vertical slide compression travel distance capability of 700 mm
  • Electronic stroke length limitation positioning resolution accurate within 0.005 mm

Working Hydraulic Pressure

  • Maximum continuous operating main hydraulic system fluid pressure of 220 bar
  • Peak shock safety valve pressure relief calibration threshold limit of 250 bar

Daylight Gap

  • Maximum open vertical daylight window working clearance of 1100 mm
  • Minimum closed shut die height tool workspace space of 250 mm

Approach Speed

  • Accelerated downward advance slide rapid travel speed of 200 mm/Sec
  • Controlled slurry mold engagement deceleration velocity of 10 mm/Sec

Pressing / Drawing Speed

  • Precision GRG acoustic slurry compaction molding speed of 3 to 10 mm/Sec
  • Maximum resistance continuous molding compression velocity of 12 mm/Sec

Return Speed

  • Smooth upward ram extraction retraction travel speed of 170 mm/Sec
  • Fast automated hydraulic decompression pre return system cycle timing

Bed / Platen Size Platen

  • Total clear bolster bed width left to right of 1600 mm
  • Total clear bolster bed depth front to back of 1300 mm

Columns

  • High tensile forged alloy steel pillar diameter of 200 mm
  • Heavy duty wear resistant bronze guide bushings with automatic grease lubrication

Working Envelope

  • Total horizontal internal clear workspace area of 1600 by 1300 mm
  • Maximum permissible upper compression mold assembly mass weight of 5500 kg

Control System

  • Industrial programmable logic controller linked with a graphical touchscreen station
  • Dual redundant non contact linear transducer position tracking systems accurate within 0.002 mm

Main Motor Power

  • High efficiency primary hydraulic pump electric drive motor power of 45 kW
  • Dedicated auxiliary cooling and continuous oil filtration motor power of 5 kW

Valves & Hydraulics

  • High dynamic response proportional pressure and flow control cartridge valve manifold block
  • Fast acting overhead gravity pre fill oil valve unit assembly

Automation

  • Digital interface connection ports for synchronized automatic mold tray transfer systems
  • Integrated multi point hydraulic pin ejectors and pneumatic mold release air blowers

Safety Features

  • Dual channel infrared light curtain barriers guarding operator workspace zones
  • Automated heavy duty dual fail safe mechanical anti drop ram safety locking blocks

SM 400 HP — Model Specifications

  • Nominal Force: 4000 KN
  • Maximum Hydraulic Pressure: 25 MPa
  • Max Opening Height of the Slider: 1250 mm
  • Max Stroke of the Slider: 800 mm
  • Effective Bed Size: 1260 × 1160 mm
  • Slider Down Speed: 100 mm/s
  • Slider Pressing Speed: 7–12 mm/s
  • Slider Return Speed: 100 mm/s
  • Ejector Cylinder Nominal Force: 400 KN
  • Stroke of the Ejection Cylinder: 300 mm
Production Case Study

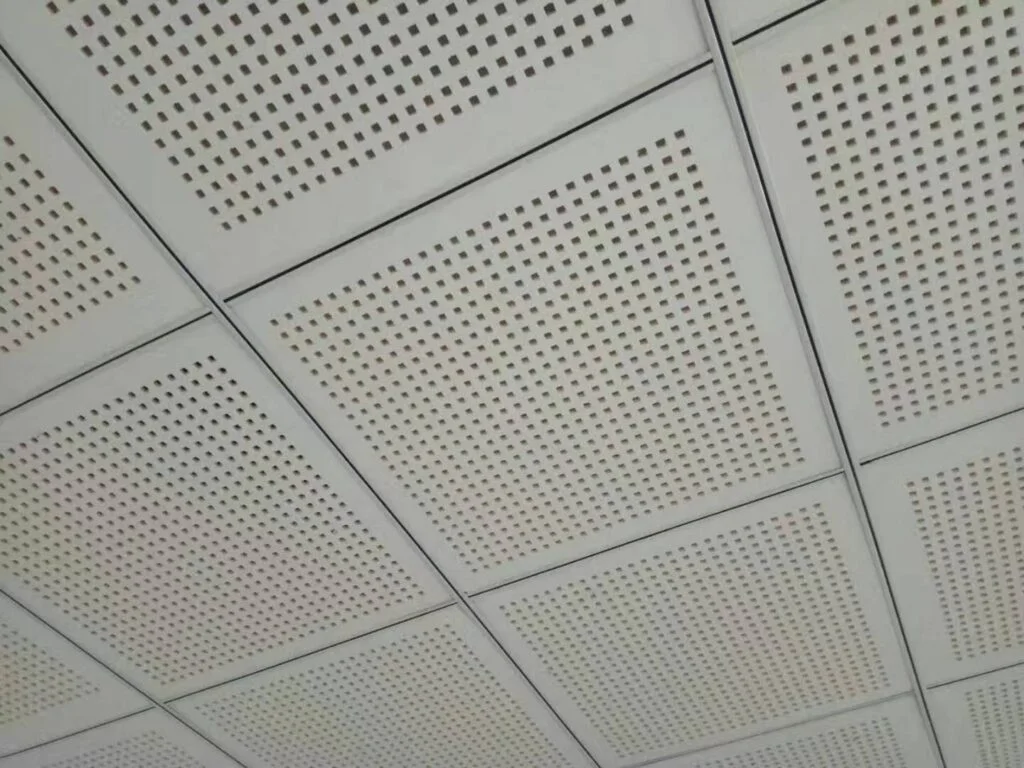
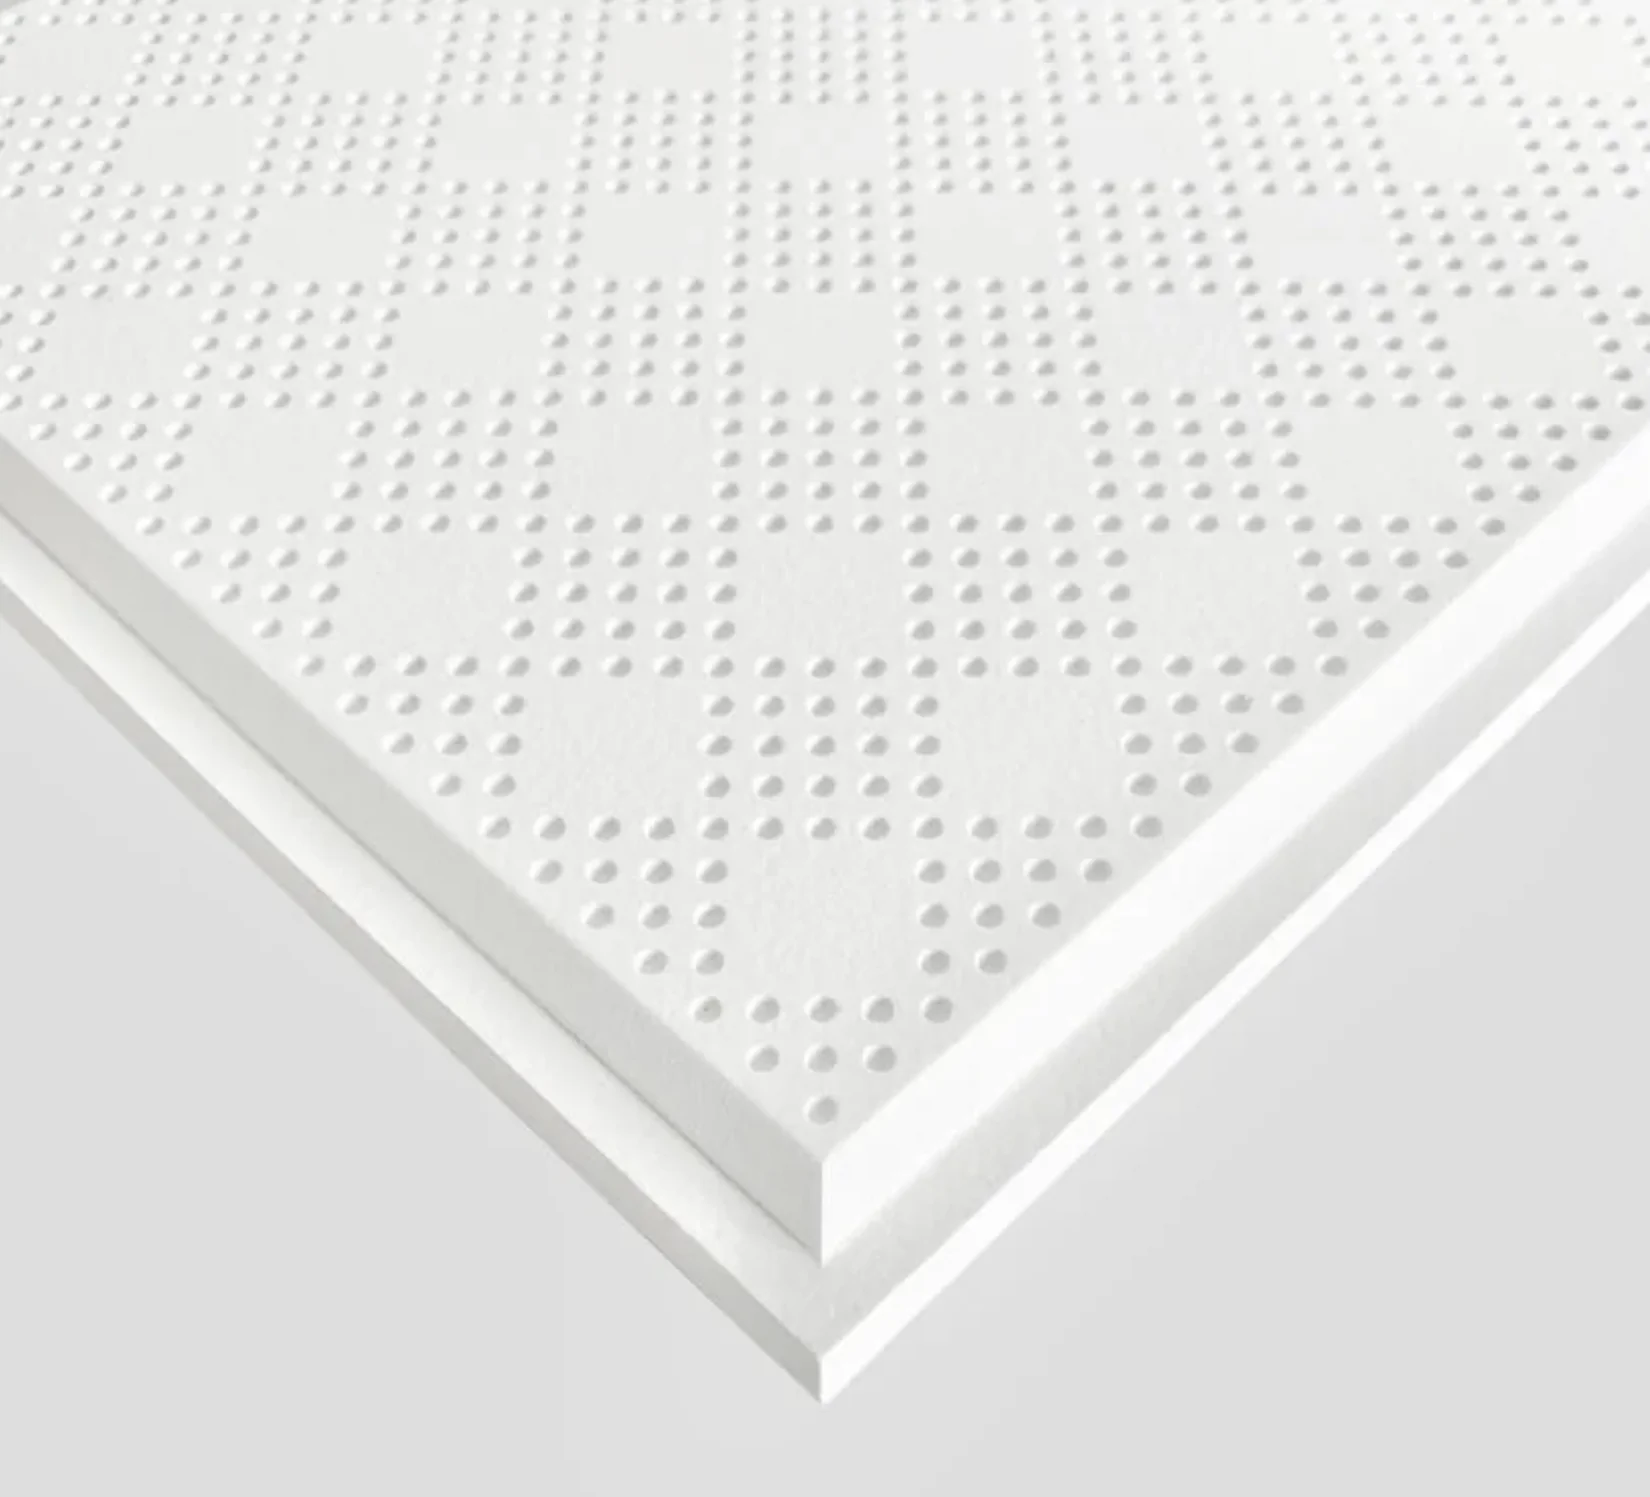
GRG Acoustic Wall & Ceiling Panels Production Line

10,000 to 18,000 cPsSlurry Viscosity
Gypsum, Glass Fiber, Polymer additivesMaterial Composition
50 to 90 SecCycle time
40 to 70 panelsOutput/Hour
Internal air voids eliminated
Uniform panel density held
Zero edge surface cracking
Precise panel thickness maintained
Crisp micro perforations formed
Production reject rates minimized
Mold service life extended
03 — Die / Mold System

Precision GRG Acoustic Wall & Ceiling Panels Die Mold Engineering

This precision GRG acoustic panel compression mold features CNC-machined aluminum cavities, integrated micro-perforation pin matrices, and vacuum de-airing channels. Engineered for 400-ton hydraulic pressing, it guarantees uniform slurry compaction, creates sharp acoustic perforations, and delivers dimensionally precise sound-absorbing panels.

Technical Specifications (Tooling)

Die Type

  • Multi cavity precision compression compaction mold assembly for Glass Fiber Reinforced Gypsum acoustic wall and ceiling panels
  • Matched upper floating compression platen and lower female textured mold set with integrated micro perforation pin matrices

Die Materials

  • Aircraft grade 7075 T6 billet aluminum alloy mold plates offering superior thermal conductivity and corrosion resistance against wet gypsum
  • Wear resistant chromium plated hardened SKD11 steel edge framing rails installed along high friction perimeter sealing margins

Tool Configuration & Construction

  • Precision CNC machined modular pattern insert carrier frames supporting fast interchangeable acoustic perforation design layouts
  • Rigid stress relieved cast aluminum base plates engineered to prevent mold flexing under full 400-ton hydraulic compaction loads

Key Tooling Features

  • Micro porous perimeter air venting and vacuum de airing channels for rapid evacuation of trapped air bubbles from dense acoustic slurries
  • High precision retractable stainless steel perforation pin networks ensuring clean acoustic hole formation without slurry bridging

Alignment Accuracy

  • Upper compression plate to lower pattern cavity guide pillar alignment deviation kept strictly under a limit of 0.010 mm
  • Platen parallelism variance across the active mold workspace restricted within a tolerance of 0.010 mm

Process Materials

  • High purity alpha and beta gypsum slurries blended with water reducing polymers and acoustic damping polymer additives
  • Chopped E glass fiber strands woven alkali resistant AR glass mesh layers and lightweight sound absorbing mineral filler compounds

Surface Finish

  • Interior decorative mold cavity surfaces polished and Teflon PTFE coated down to a surface roughness of Ra 0.15 microns
  • Hydrophobic non stick cavity surface treatment preventing gypsum slurry adhesion and reducing acoustic perforation pin clogging

Tool Life

  • Expected operational span of 120000 compression molding cycles before requiring mandatory surface coating re application and pin inspection
  • Total structural aluminum mold frame and base assembly lifespan capacity reaching 1000000 production cycles before major rebuilds
Case Study (Die Performance)

Precision GRG Acoustic Wall & Ceiling Panels Die Mold

7075-T6 Alu AlloyDie Steel
58–62 HRCHardness
Vacuum HardeningSurface Treatment
Internal air voids eliminated
Uniform panel density held
Zero edge surface cracking
Precise panel thickness maintained
Crisp micro perforations formed
Production reject rates minimized
Extended mold service life

04 — Product Application

Where GRG Acoustic Wall & Ceiling Panels Are Used

Precision-molded GRG acoustic wall and ceiling panels deliver exceptional sound absorption, noise reverberation control, and high-definition architectural aesthetics. Their fire-rated durability, uniform material density, and crisp acoustic perforations make them essential surface treatments across modern commercial, cultural, and institutional spaces.

Industry Applications

GRG acoustic wall and ceiling panels are widely specified across commercial real estate, cultural architecture, hospitality infrastructure, educational centers, and corporate facilities. High-tonnage hydraulic compaction ensures uniform slurry density, flat panel perimeters, and clean micro-perforations, allowing panels to mount directly onto acoustic framing systems or drop into ceiling grids to provide stable noise reduction coefficients across all sound frequency spectrums.

Auditoriums, Concert Halls, Performing Arts Centers, and Theaters

Controls ambient reverberation times and eliminates sound echoes to optimize speech intelligibility and acoustic clarity during live performances. Delivers precise geometric sound-diffusing surfaces and perforated acoustic panels that meet strict international fire and safety standards.

Corporate Head-Offices, Open-Plan Workspaces, and Executive Conference Rooms

Reduces background noise pollution and sound transmission across open office zones, meeting areas, and video conferencing rooms. Maintains precise dimensional stability and edge flatness for seamless integration with concealed wall framing and acoustic ceiling grids.

Commercial Shopping Malls, Grand Hotel Lobbies, and Airport Terminals

Provides high-density sound absorption across large public atrium spaces while withstanding high foot-traffic humidity and air circulation. Offers smooth, paintable plaster surfaces that accept custom decorative finishes, wood-grain laminates, and integrated lighting troughs.

Educational Institutions, Lecture Theaters, University Auditoriums, and Libraries

Enhances speech clarity and auditory comfort for students by absorbing unwanted low-frequency noise and high-pitch echoes. Features non-toxic, non-combustible GRG material properties that ensure zero-VOC indoor air quality compliance in educational buildings.

Finished Product Gallery

05 — Key Advantages

Why Choose the 400-Ton Sinter Hydraulic Press

The 400-Ton Sinter Hydraulic Press delivers high-density compaction force and precise parallel slide guidance for molding GRG acoustic panels. Its rigid four-column frame, multi-stage pressure ramping, and programmable dwell control eliminate air voids and guarantee flat, sound-absorbing panels with crisp micro-perforations.

Technical & Commercial Benefits

01

High-Tonnage 400-Ton Compression Eliminating Internal Slurry Air Voids

Applies uniform, high-density hydraulic pressure across large mold areas to thoroughly purge trapped air bubbles from dense gypsum slurries. Complete air removal produces solid, defect-free acoustic panels with consistent density and zero micro-porosity.

02

Multi-Stage Pressure Ramping Protecting Delicate Perforation Pin Matrices

Features gradual pressure control during initial tool engagement to prevent pin shearing, hole bridging, or slurry displacement around micro-perforations. Controlled compaction ensures clean, open sound-absorbing holes across the entire panel surface.

03

Heavy Four-Column Architecture Guaranteeing Absolute Thickness Uniformity

Engineered with pre-stressed forged steel columns that maintain strict upper and lower platen parallelism under full 400-ton hydraulic loads. Zero platen deflection prevents panel warping, ensuring predictable acoustic absorption coefficients and flat perimeter joins.

04

Programmable Hydraulic Dwell Setting Panel Density for Acoustic Consistency

Holds target pressure at bottom dead center to allow gypsum slurry setting and complete compaction of embedded glass fiber layers. Controlled dwell cycles eliminate internal material springback, maintaining exact acoustic performance standards across production batches.

05

Smooth Deceleration and Vibration-Free Slide Motion Preventing Green-State Cracking

Decelerates the upper platen prior to mold contact to prevent hydraulic shock, slurry washing, or edge fracturing during compaction. Vibration-free ram movement protects fragile green-state acoustic panels during critical forming and initial curing phases.

06

Automated De-Airing and Pin Ejection Systems Maximizing Production Efficiency

Integrates vacuum de-airing channels with multi-point hydraulic ejector pins for rapid, damage-free release of large acoustic panels. High cycle efficiency enables outputs of 40 to 70 panels per hour, significantly reducing per-unit labor costs and material scrap rates.