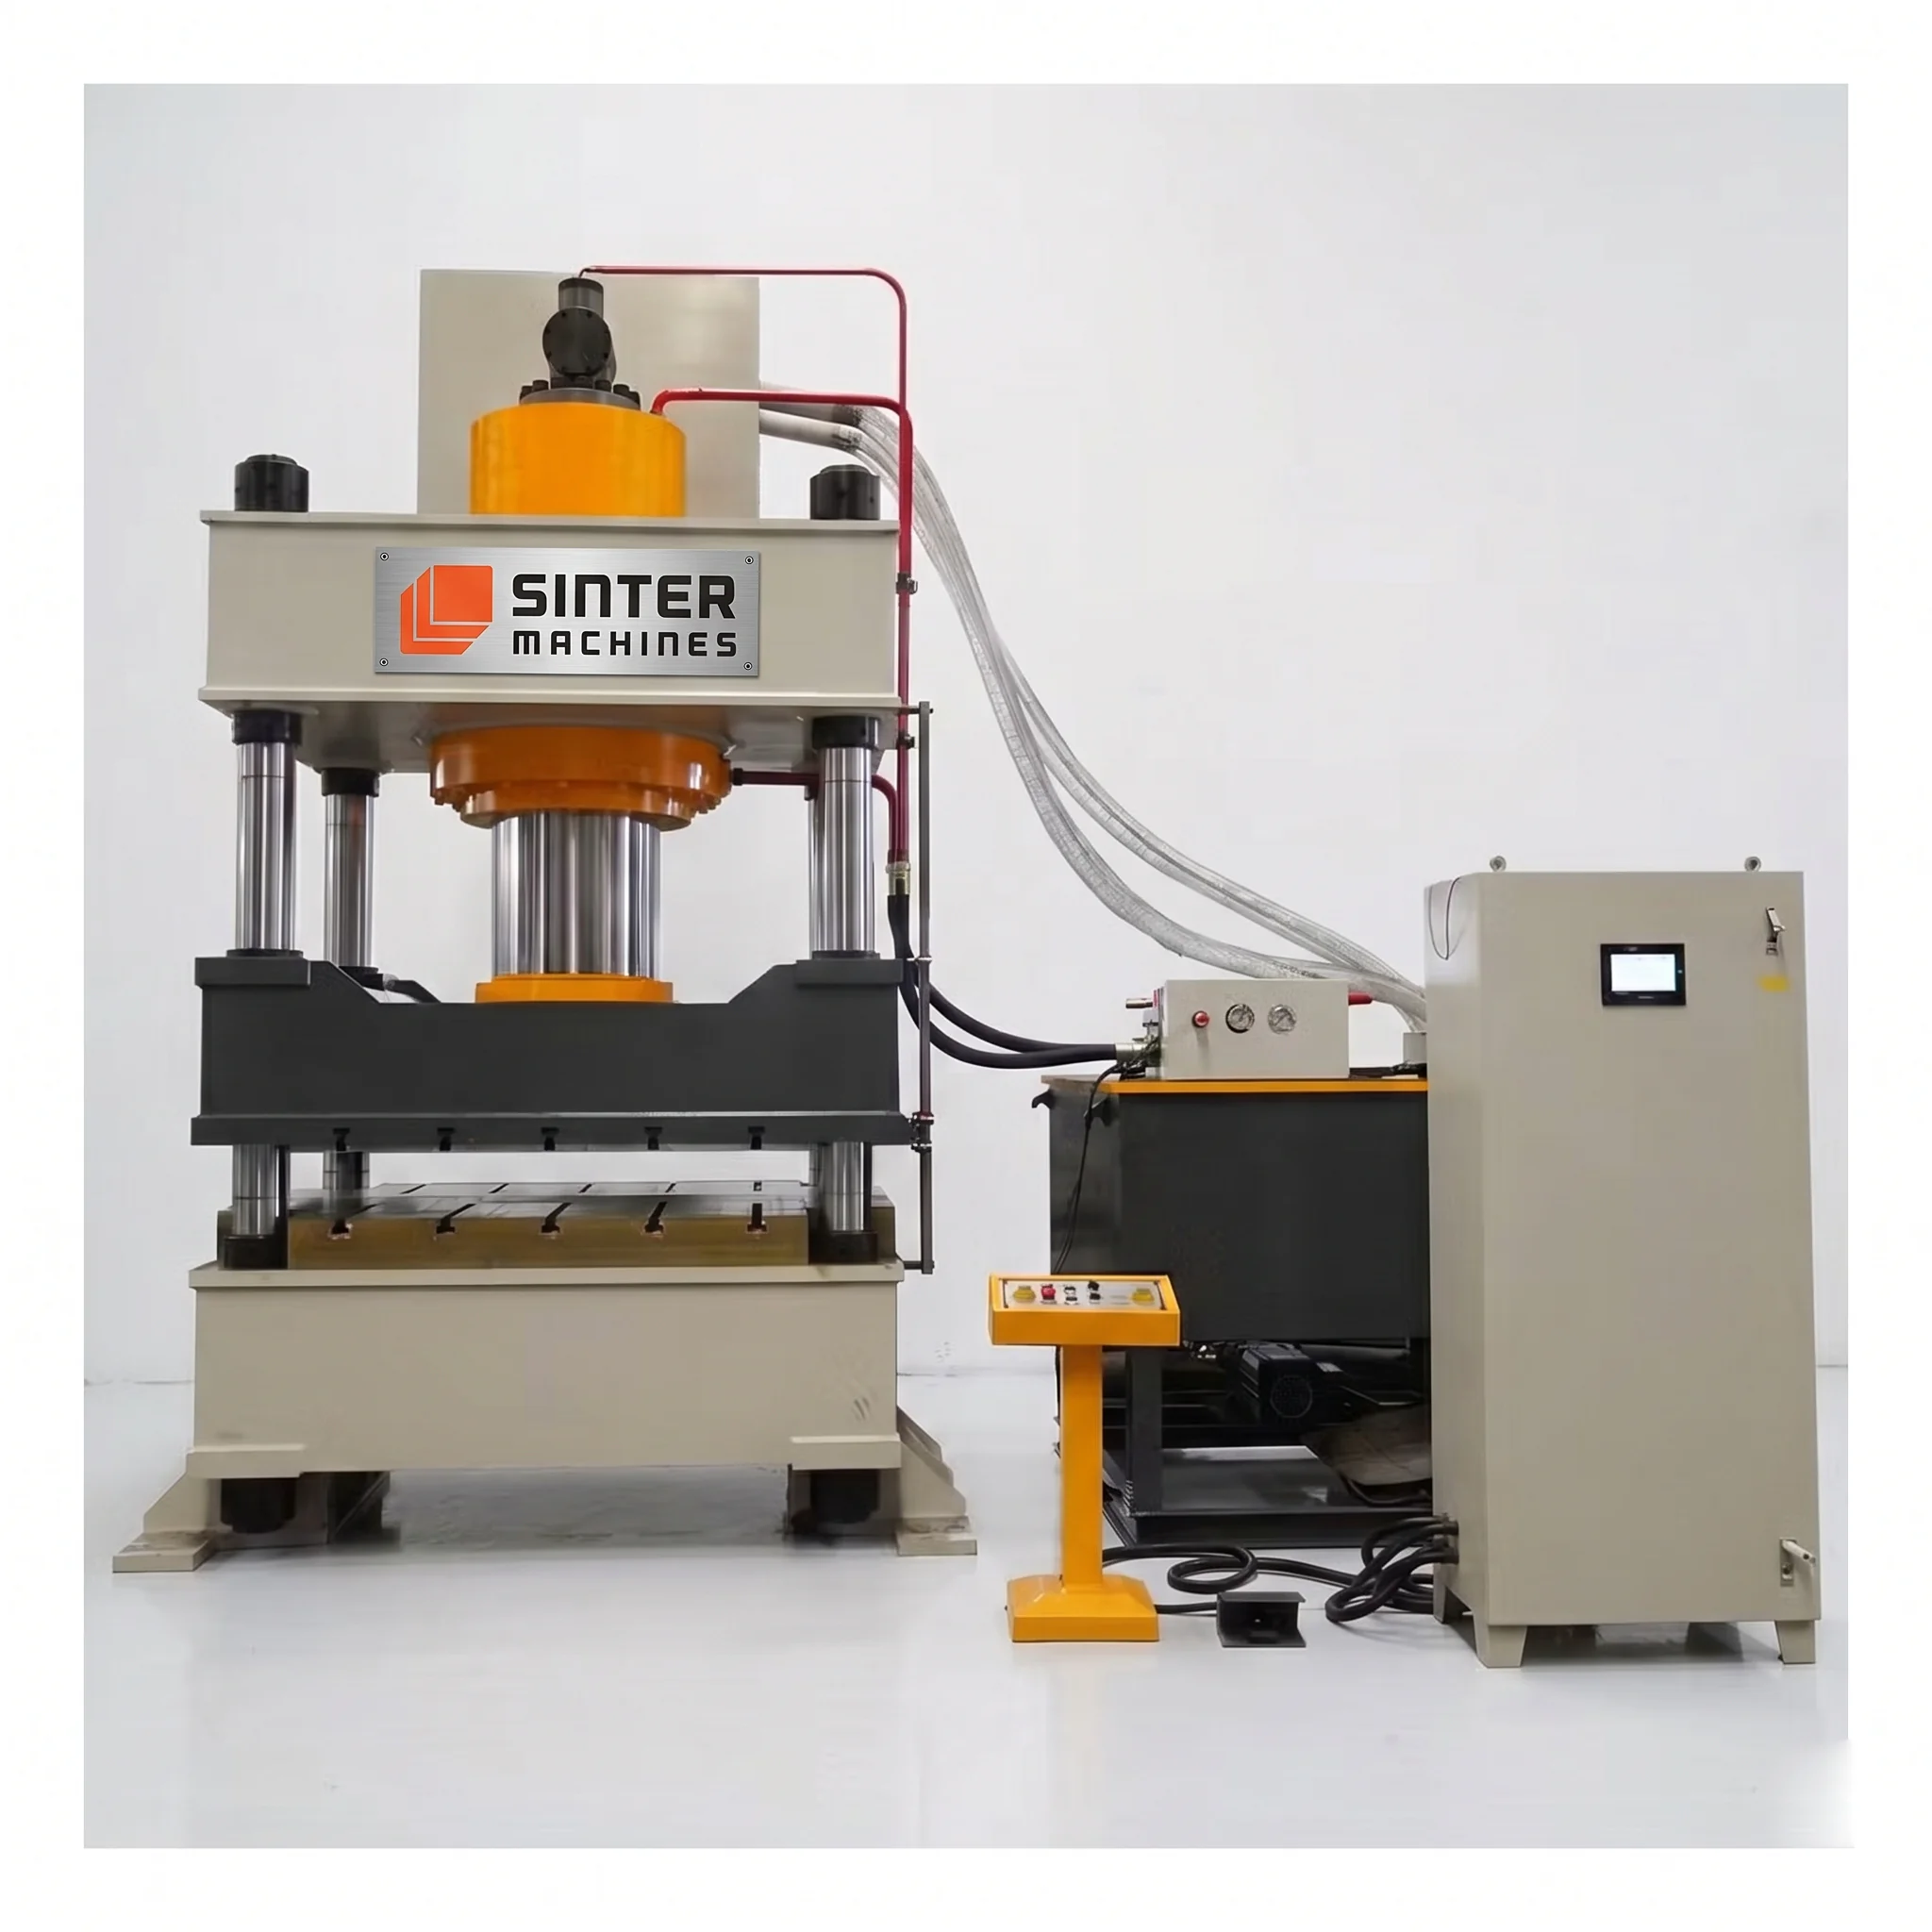
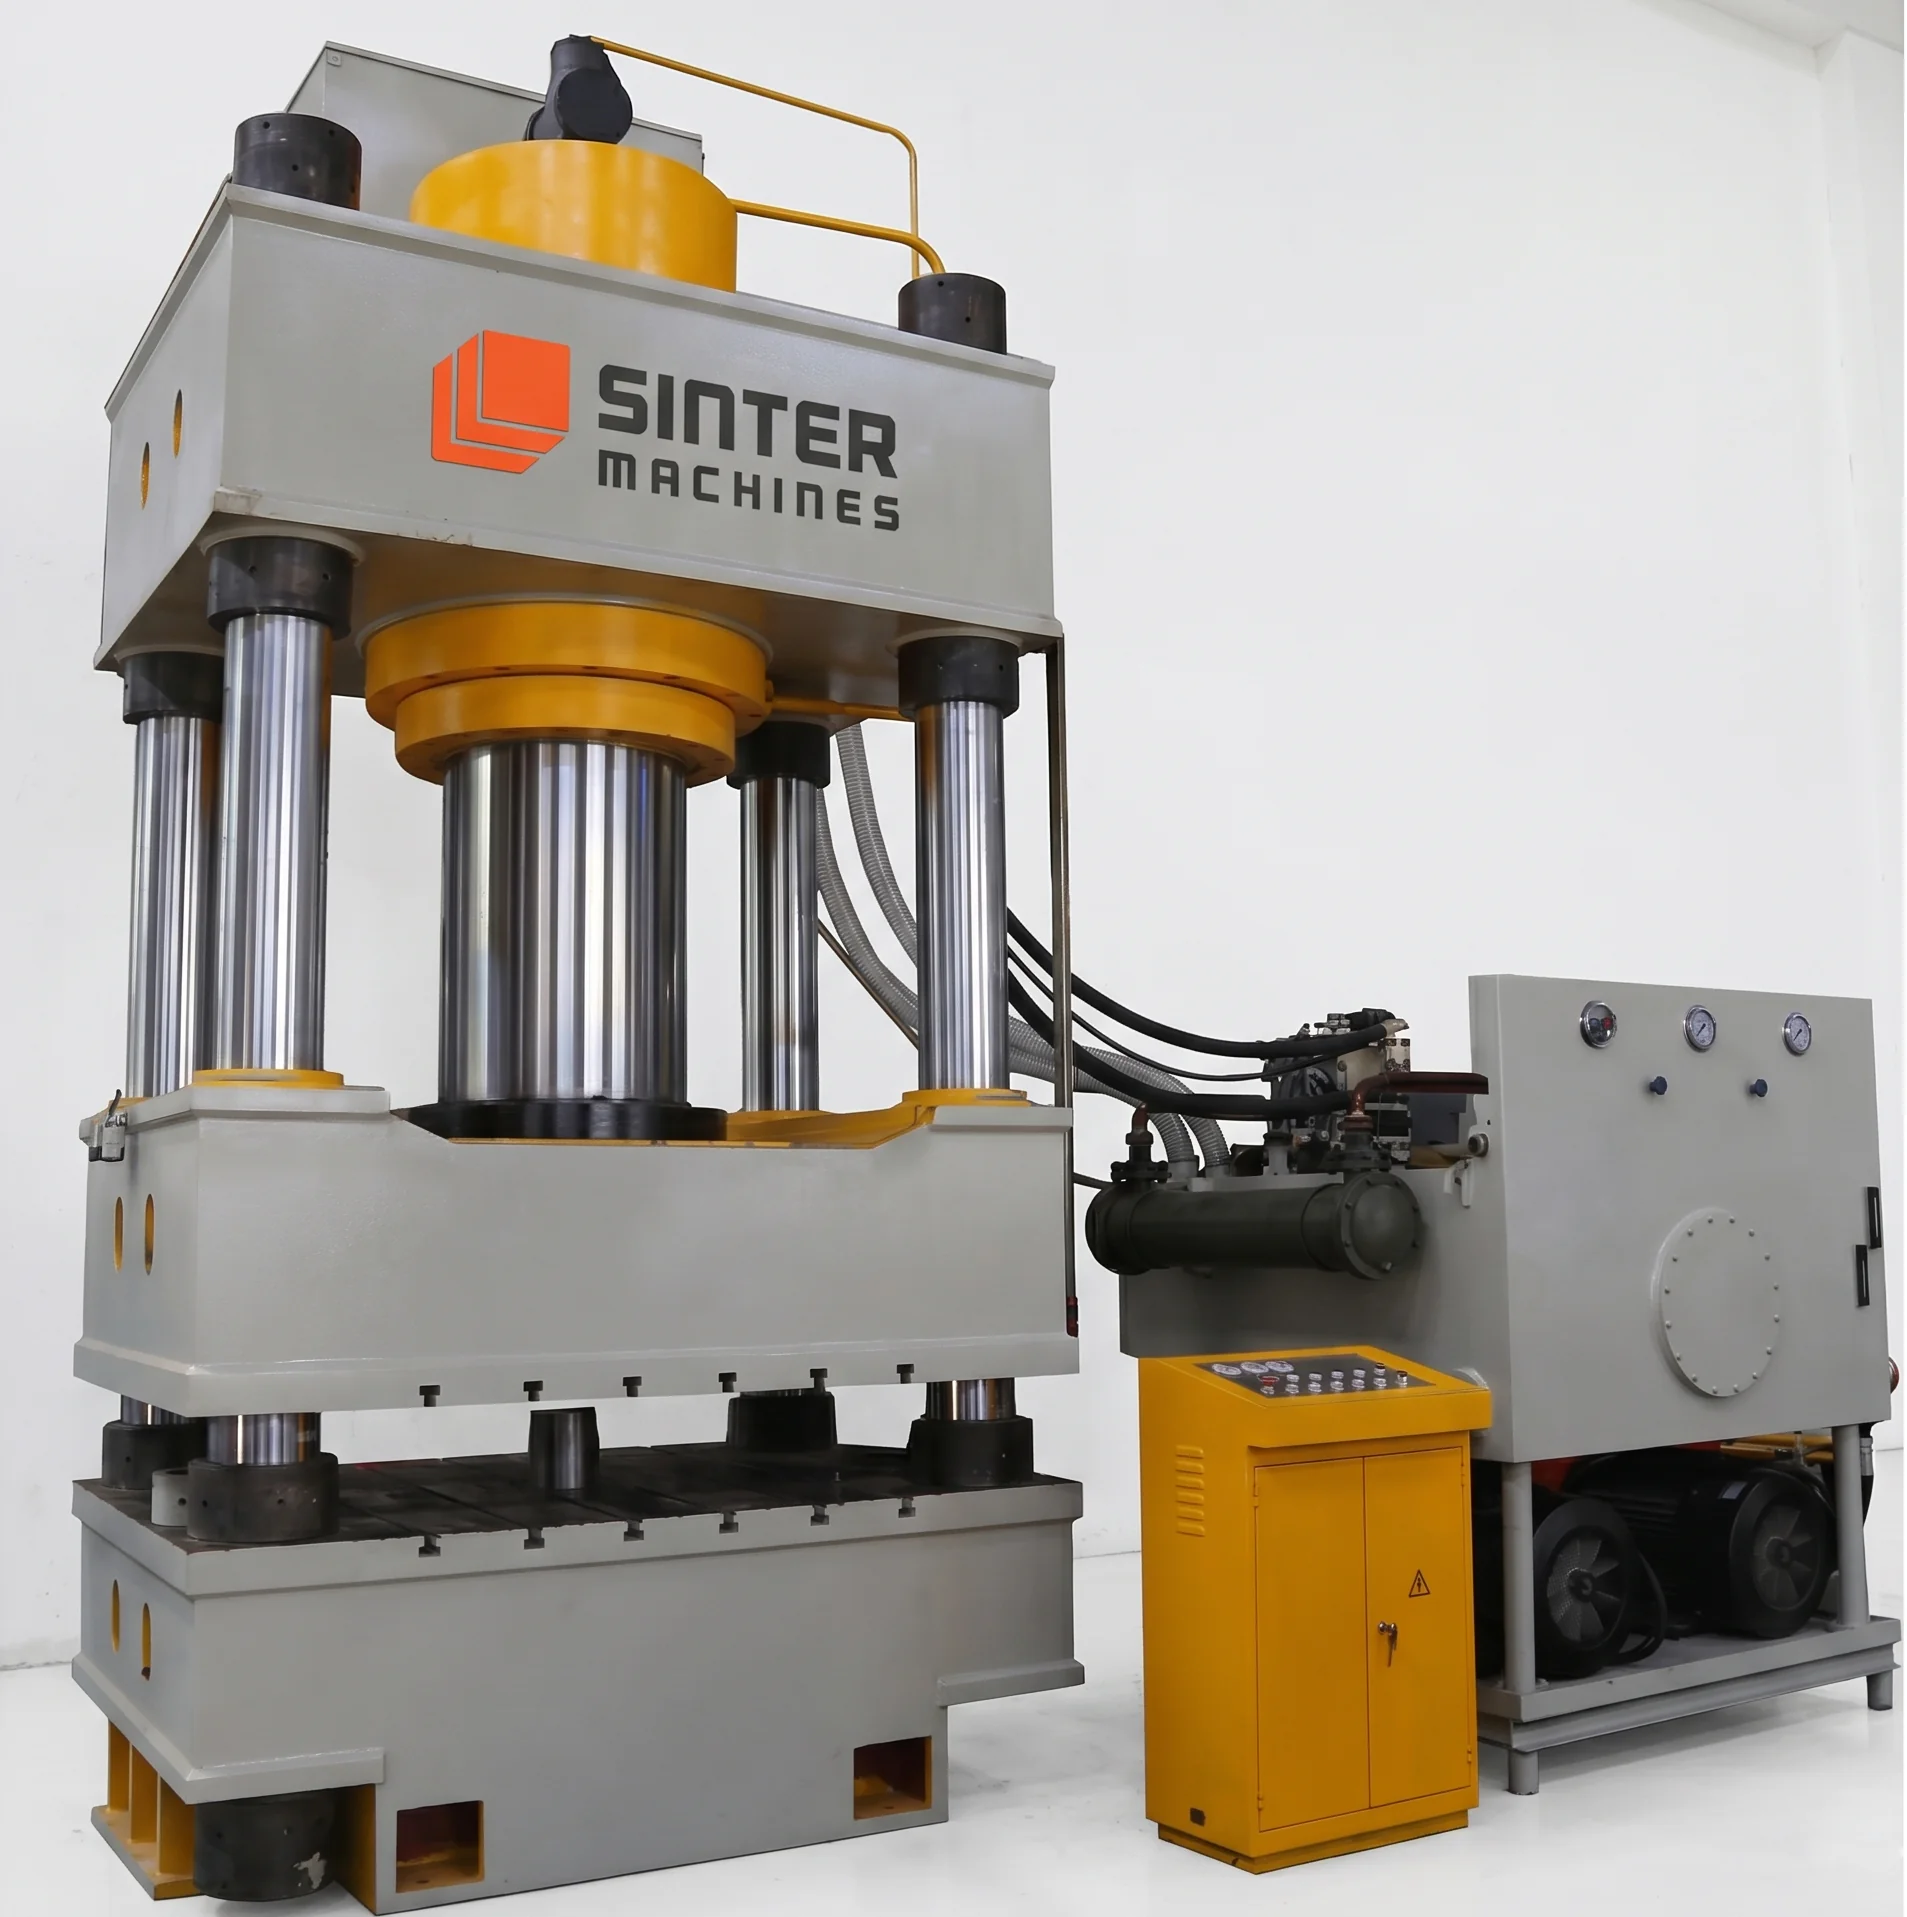
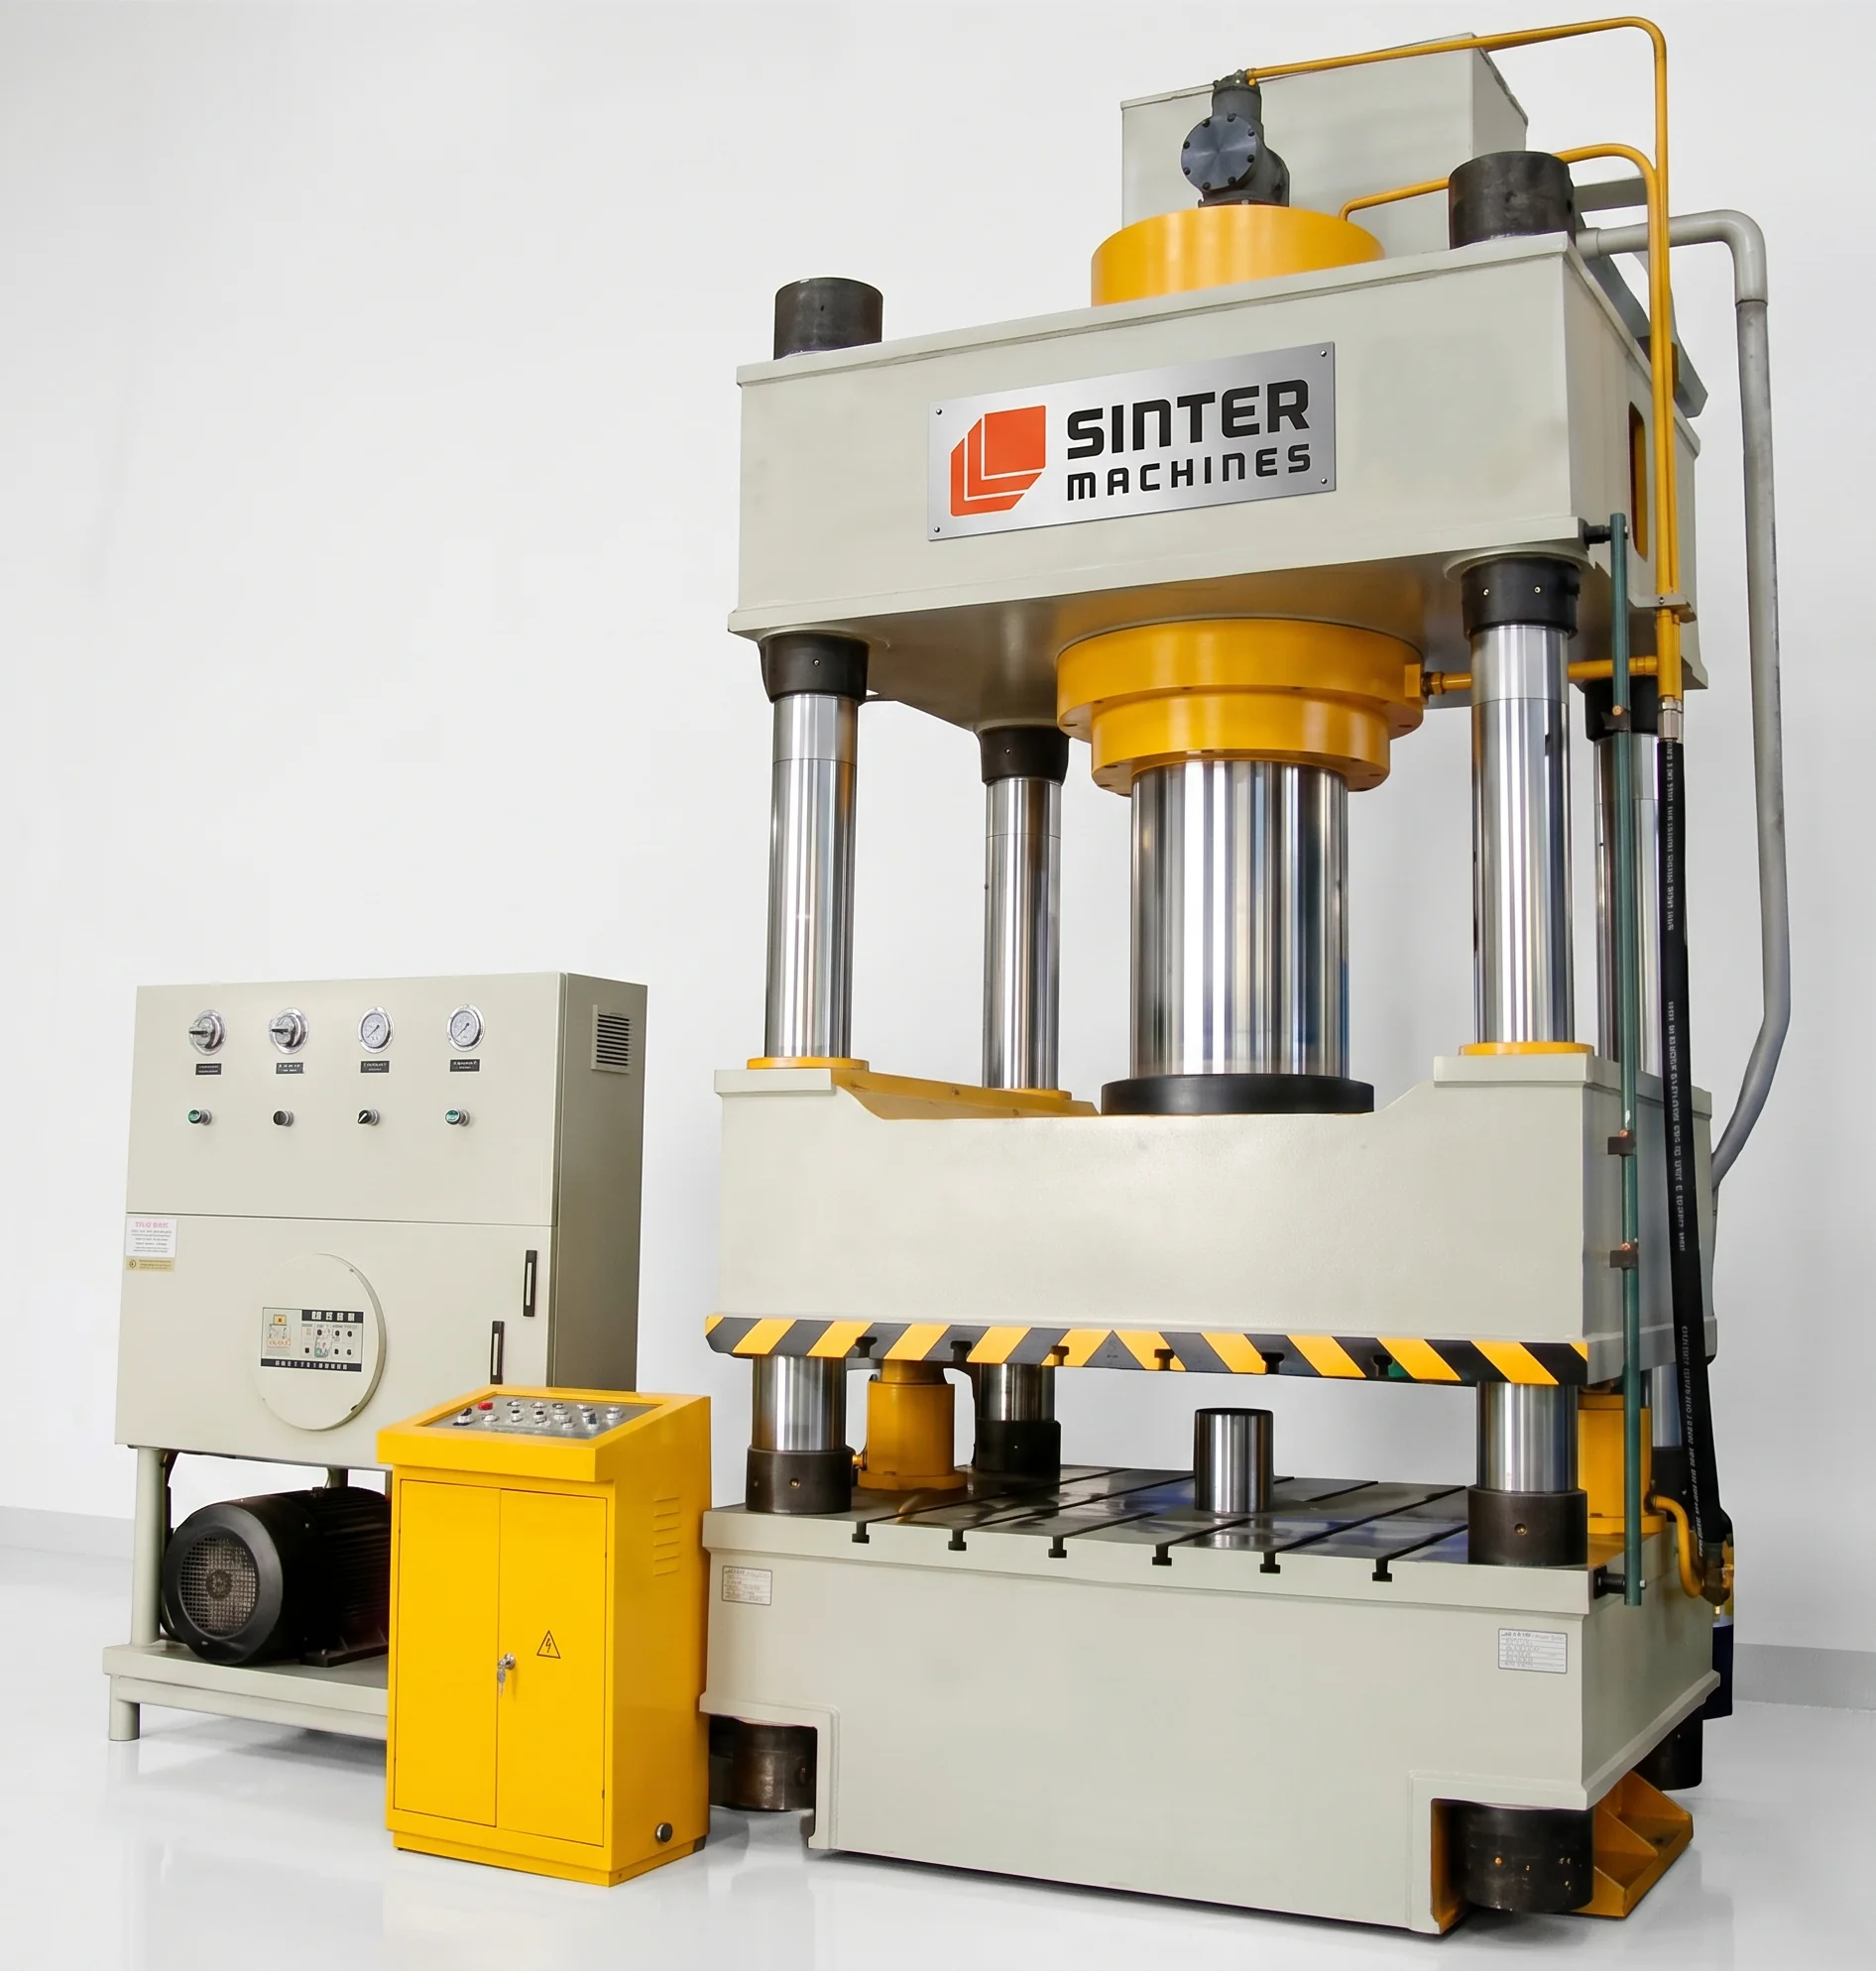
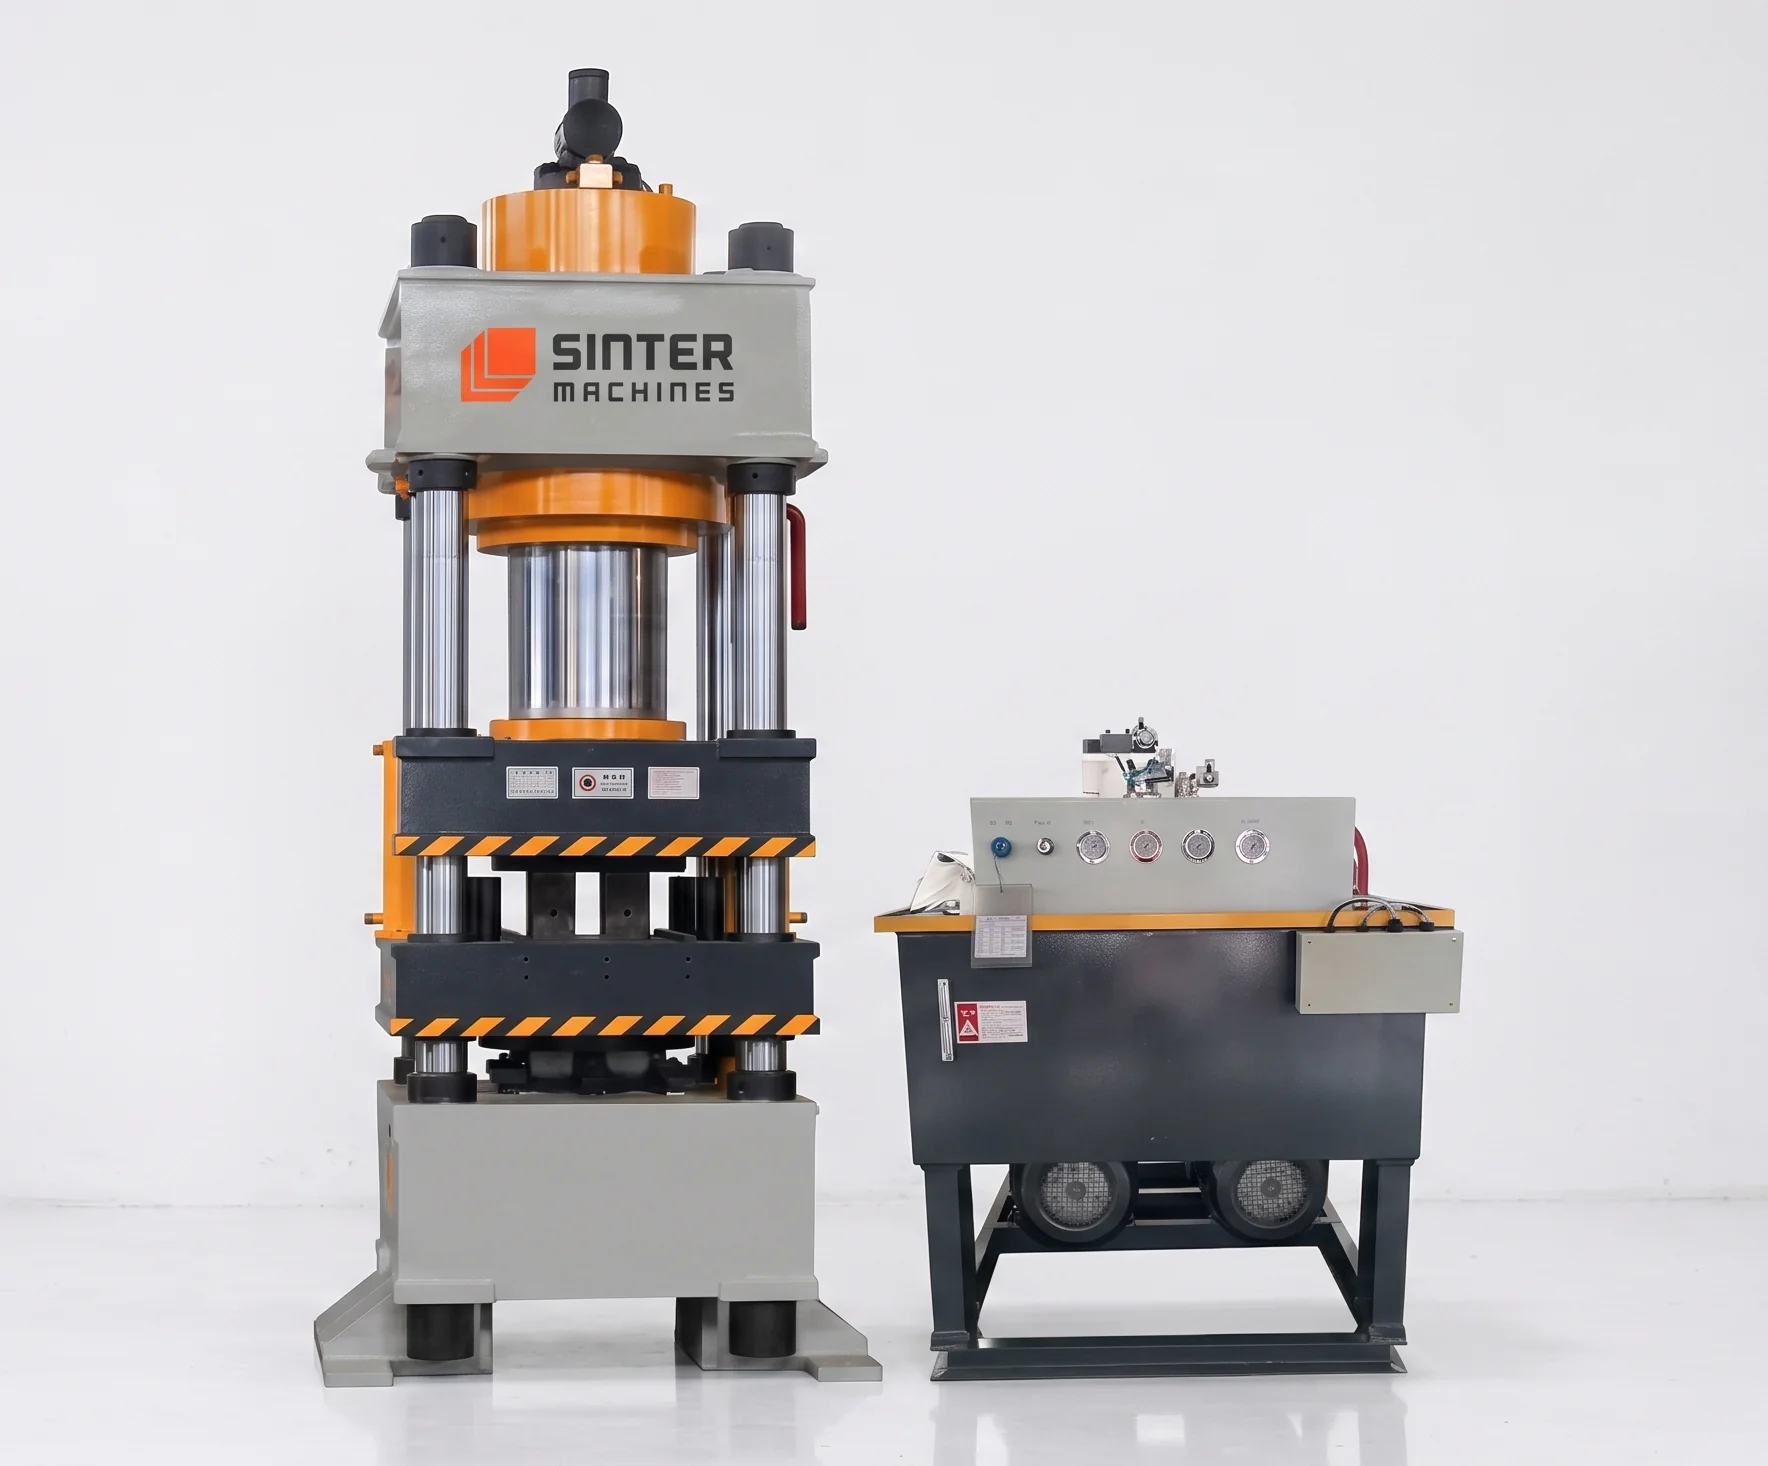
1600T Inserts & Tooling Press press view 1
Inserts and Heavy-Duty Tooling · Hydraulic Press Machine

1600 Ton Four Column Hydraulic Press for PM Large Inserts & HeavyDuty Tooling Components

1600T Rated Capacity
180 mm/s Slider Down Speed
9–18 mm/s Slider Pressing Speed
180 mm/s Slider Return Speed

01 — Press System

1600 Ton Four Column Hydraulic Press Machine

The 1600-ton four-column hydraulic press provides massive multi-axis force with exceptional structural rigidity for heavy-duty powder metallurgy tooling production. Its heavy-duty framework ensures precise column parallelism and minimum frame deflection under maximum compaction tonnage.

Use Case

Engineered for high-density compaction of large tungsten carbide inserts, high-speed steel dies, and heavy-duty wear-resistant PM tooling components. It delivers intense pressure to achieve uniform green density across thick-section tool blanks and complex cutting profiles.

  • Core Applications: Provides high-tonnage compaction for heavy industrial cutting inserts, mining equipment wear pads, oil and gas drilling bits, and high-performance metalworking tool preforms. It is ideal for producing high-durability PM parts that demand extreme hardness and high compressive strength.
  • Material: Processes tool steel, high-speed steel (HSS), tungsten carbide, iron-based PM alloys, and cobalt-based superalloys blended with organic binders and lubricants. This advanced material matrix enables excellent powder flow, high green strength, and minimal die wall friction.
  • Products Processed: Compacts heavy carbide indexable inserts, large tool blanks, cold-forming die inserts, punch tips, and wear plates. It yields uniform density throughout thick-walled preforms to prevent warping or micro-cracking during vacuum sintering.
  • Why 1600-Ton Hydraulic Press: The 1600-ton capacity delivers the force required to consolidate tough, hard-to-compact refractory powders into ultra-high target green densities. Hydraulic pressure control ensures consistent multi-stage compaction without density gradients or edge chipping across heavy tool geometries.

02 — Technical Specifications

SM 1600 HP – HYDRAULIC PRESS MACHINE COMPLETE TECHNICAL DATA

The SM 1600 HP Hydraulic Press Machine is a high-capacity Powder Metallurgy (PM) compaction platform engineered for the production of wear-resistant inserts, large die blocks, and heavy-duty tooling components. Featuring a robust four-column structure, precision hydraulic control, and a 1600-ton pressing force, it delivers exceptional density uniformity, dimensional accuracy, and repeatability for large and complex PM parts.

Capacity & Structural Design

  • Rated Press Capacity: 1600 metric tons (≈ 15,700 kN)
  • Press Configuration: Fourpillar / fourcolumn guided hydraulic press
  • Frame Construction: Extraheavy welded steel frame, stressrelieved
  • Design Duty: Continuous heavyindustrial PM production
  • Structural Safety Factor: ≥ 1.35
  • Elastic Deflection at Full Load: ≤ 0.12 mm
  • Load Distribution: Uniform across entire platen area (critical for tooling flatness)

Hydraulic System

Main Hydraulic Cylinder

  • Type: Doubleacting, precisionguided, heavywall construction
  • Bore Diameter: 700–820 mm
  • Stroke: 800–1,100 mm

Maximum Working Pressure: 30–32 MPa (300–320 bar)

Hydraulic Power Unit

  • Multiple synchronized variabledisplacement axialpiston pumps
  • Servo / proportional control valves
  • Closedloop pressure and position feedback

Pressing Modes

  • Constantpressure compaction
  • Positioncontrolled pressing
  • Multistage pressure profiles with programmable dwell
  • Pressure ramping for crackfree compaction of hard powders

Platen & Working Envelope

Upper / Lower Platen Size

  • Standard: 1,400 × 1,400 mm
  • Optional: up to 1,600 × 1,600 mm

Guide Columns

  • Quantity: 4
  • Diameter: 220–260 mm
  • Surface: Hardened, hardchromed & precisionground
  • Daylight Opening: 1,600–2,000 mm
  • Platen Parallelism Accuracy: ±0.02 mm / 300 mm

Controls, Monitoring & Safety

  • Control System: Highperformance PLC + industrial HMI

Process Monitoring

  • Force vs displacement curve (realtime)
  • Dwell pressure and time
  • Tool load distribution
  • Cycle logging, SPC, traceability

Safety Systems

  • Redundant safety PLC (SILrated)
  • Light curtains / safety scanners
  • Hydraulic overload & pressurerelief protection
  • Emergency stop circuits (CE / ISO compliant)

SM 1600 HP — Model Specifications

  • Nominal Force: 16000 KN
  • Maximum Hydraulic Pressure: 25 MPa
  • Max Opening Height of the Slider: 1500 mm
  • Max Stroke of the Slider: 900 mm
  • Effective Bed Size: 1600 × 1600 mm
  • Slider Down Speed: 180 mm/s
  • Slider Pressing Speed: 9–18 mm/s
  • Slider Return Speed: 180 mm/s
  • Ejector Cylinder Nominal Force: 800 KN
  • Stroke of the Ejection Cylinder: 300 mm
Production Case Study

Powder Metallurgy (PM) wear-resistant inserts, large die blocks, and heavy-duty tooling components Production Line

Carbide, HSS & Cobalt PowdersRaw Material
3000–18000 grmsProduct Weight
7.2–7.6 g/cm³Green Density
30–50 SecCycle Time
High wear and abrasion resistance
Exceptional hot hardness properties maintained
Uniform green density throughout core
Minimal shrinkage distortion during sintering
Extended tool life under stress
Superior edge toughness and strength
Reduced tooling replacement downtime

03 — Die / Mold System

Precision Powder Metallurgy (PM) Wear-Resistant Inserts, Heavy-Duty Tooling Components Die Mold Engineering

Precision Powder Metallurgy (PM) Wear-Resistant Inserts and Heavy-Duty Tooling Components rely on advanced die and mold engineering to achieve high density, dimensional accuracy, and consistent performance. Specialized PM tooling is designed to optimize powder flow, compaction pressure distribution, and part ejection, ensuring the reliable production of complex geometries and large components.

Technical Specifications (Tooling)

Tool Type

  • Heavy-duty multi-piece PM compaction tooling
  • Multi-level die system for large components

Tool Materials

  • Tool steels: H13 / D2 / PM-grade tool steel
  • Inserts: Carbide inserts for wear zones

Hardness: 60–64 HRC

Tool Construction

  • Upper punch: Slot/pole formation
  • Lower punch: Base and density control
  • Die cavity: Outer profile
  • Core rod: Inner bore

Multi-Level Tooling Design

Segmented punches for:

  • Outer ring
  • Slot region
  • Central hub

Floating die system

Critical Engineering Factors

  • Concentricity of rotor
  • Slot symmetry
  • Density distribution
  • Bore alignment

Alignment Accuracy: ±0.01–0.02 mm

Surface Finish

AreaFinish
BorePrecision polished
Outer ringSmooth
Slot regionsPrecision machined

Lubrication

  • Powder lubrication
  • Tool coatings (TiN/DLC optional)

Tool Life: 150,000 – 350,000 cycles

Case Study (Die Performance)

Powder Metallurgy (PM) Wear-Resistant Inserts, Heavy-Duty Tooling Components Die Mold Tooling

Micrograin Tungsten Carbide / CPM 15VDie Steel
62–65 HRCHardness
Vacuum HardeningHeat Treatment
High wear resistance under friction
Superior compressive strength for compaction
Minimal dimensional distortion during pressing
Extended mold operational life span
Smooth surface ejection without galling
Consistent precision for complex geometries
Reduced tooling maintenance downtime

04 — Product Application

Where Powder Metallurgy (PM) Wear-Resistant Inserts, Heavy-Duty Tooling Components Are Used

Powder Metallurgy (PM) wear-resistant inserts and heavy-duty tooling components are widely used in mining, aerospace, construction, agricultural, and heavy machinery industries where high strength, wear resistance, and durability are critical. They are commonly found in dies, punches, cutting tools, forming tools, ground equipment, and high-load industrial components that operate under severe abrasive and impact conditions.

Industry Applications

Construction Industry

In the construction industry, Powder Metallurgy (PM) wear-resistant tooling components are used in forging and compaction dies, heavy-duty punches for earth-moving equipment, and excavator and crusher tooling inserts. Their high hardness, strength, and abrasion resistance help extend service life, reduce maintenance requirements, and improve performance in demanding construction and material-handling environments.

Mining Industry

In the mining industry, Powder Metallurgy (PM) wear-resistant tooling components are extensively used in crusher, shredder, and press die blocks, rock-cutting and drilling punches, and wear-resistant press tooling. Their superior hardness, impact strength, and abrasion resistance enable longer service life, reduced downtime, and reliable performance in harsh mining environments characterized by heavy loads and highly abrasive materials.

Aerospace (Tooling & Ground Equipment)

In the aerospace tooling and ground equipment sector, Powder Metallurgy (PM) wear-resistant inserts and heavy-duty tooling components are used in large forming and stamping dies, aerospace machining and assembly tooling, and structural tooling inserts for non-flight hardware. Their high dimensional stability, wear resistance, and precision help ensure consistent manufacturing quality, extended tool life, and reliable performance during the production and assembly of aerospace components.

Heavy Machinery Industries

In the Heavy Machinery Industries, Powder Metallurgy (PM) wear-resistant inserts and heavy-duty tooling components are used in equipment such as excavators, crushers, earthmovers, drilling machines, and material-handling systems. These components withstand severe abrasion, impact, and high loads, improving equipment durability, reducing downtime, and lowering maintenance costs.

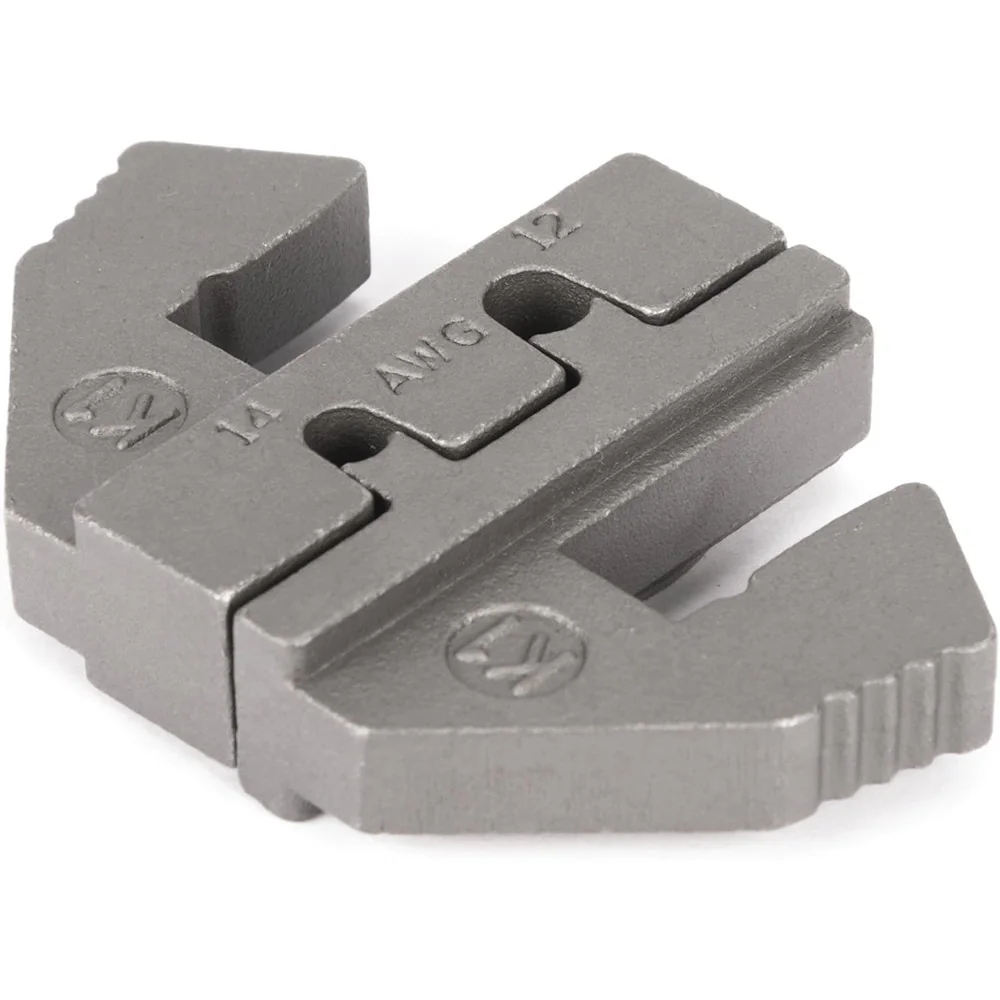
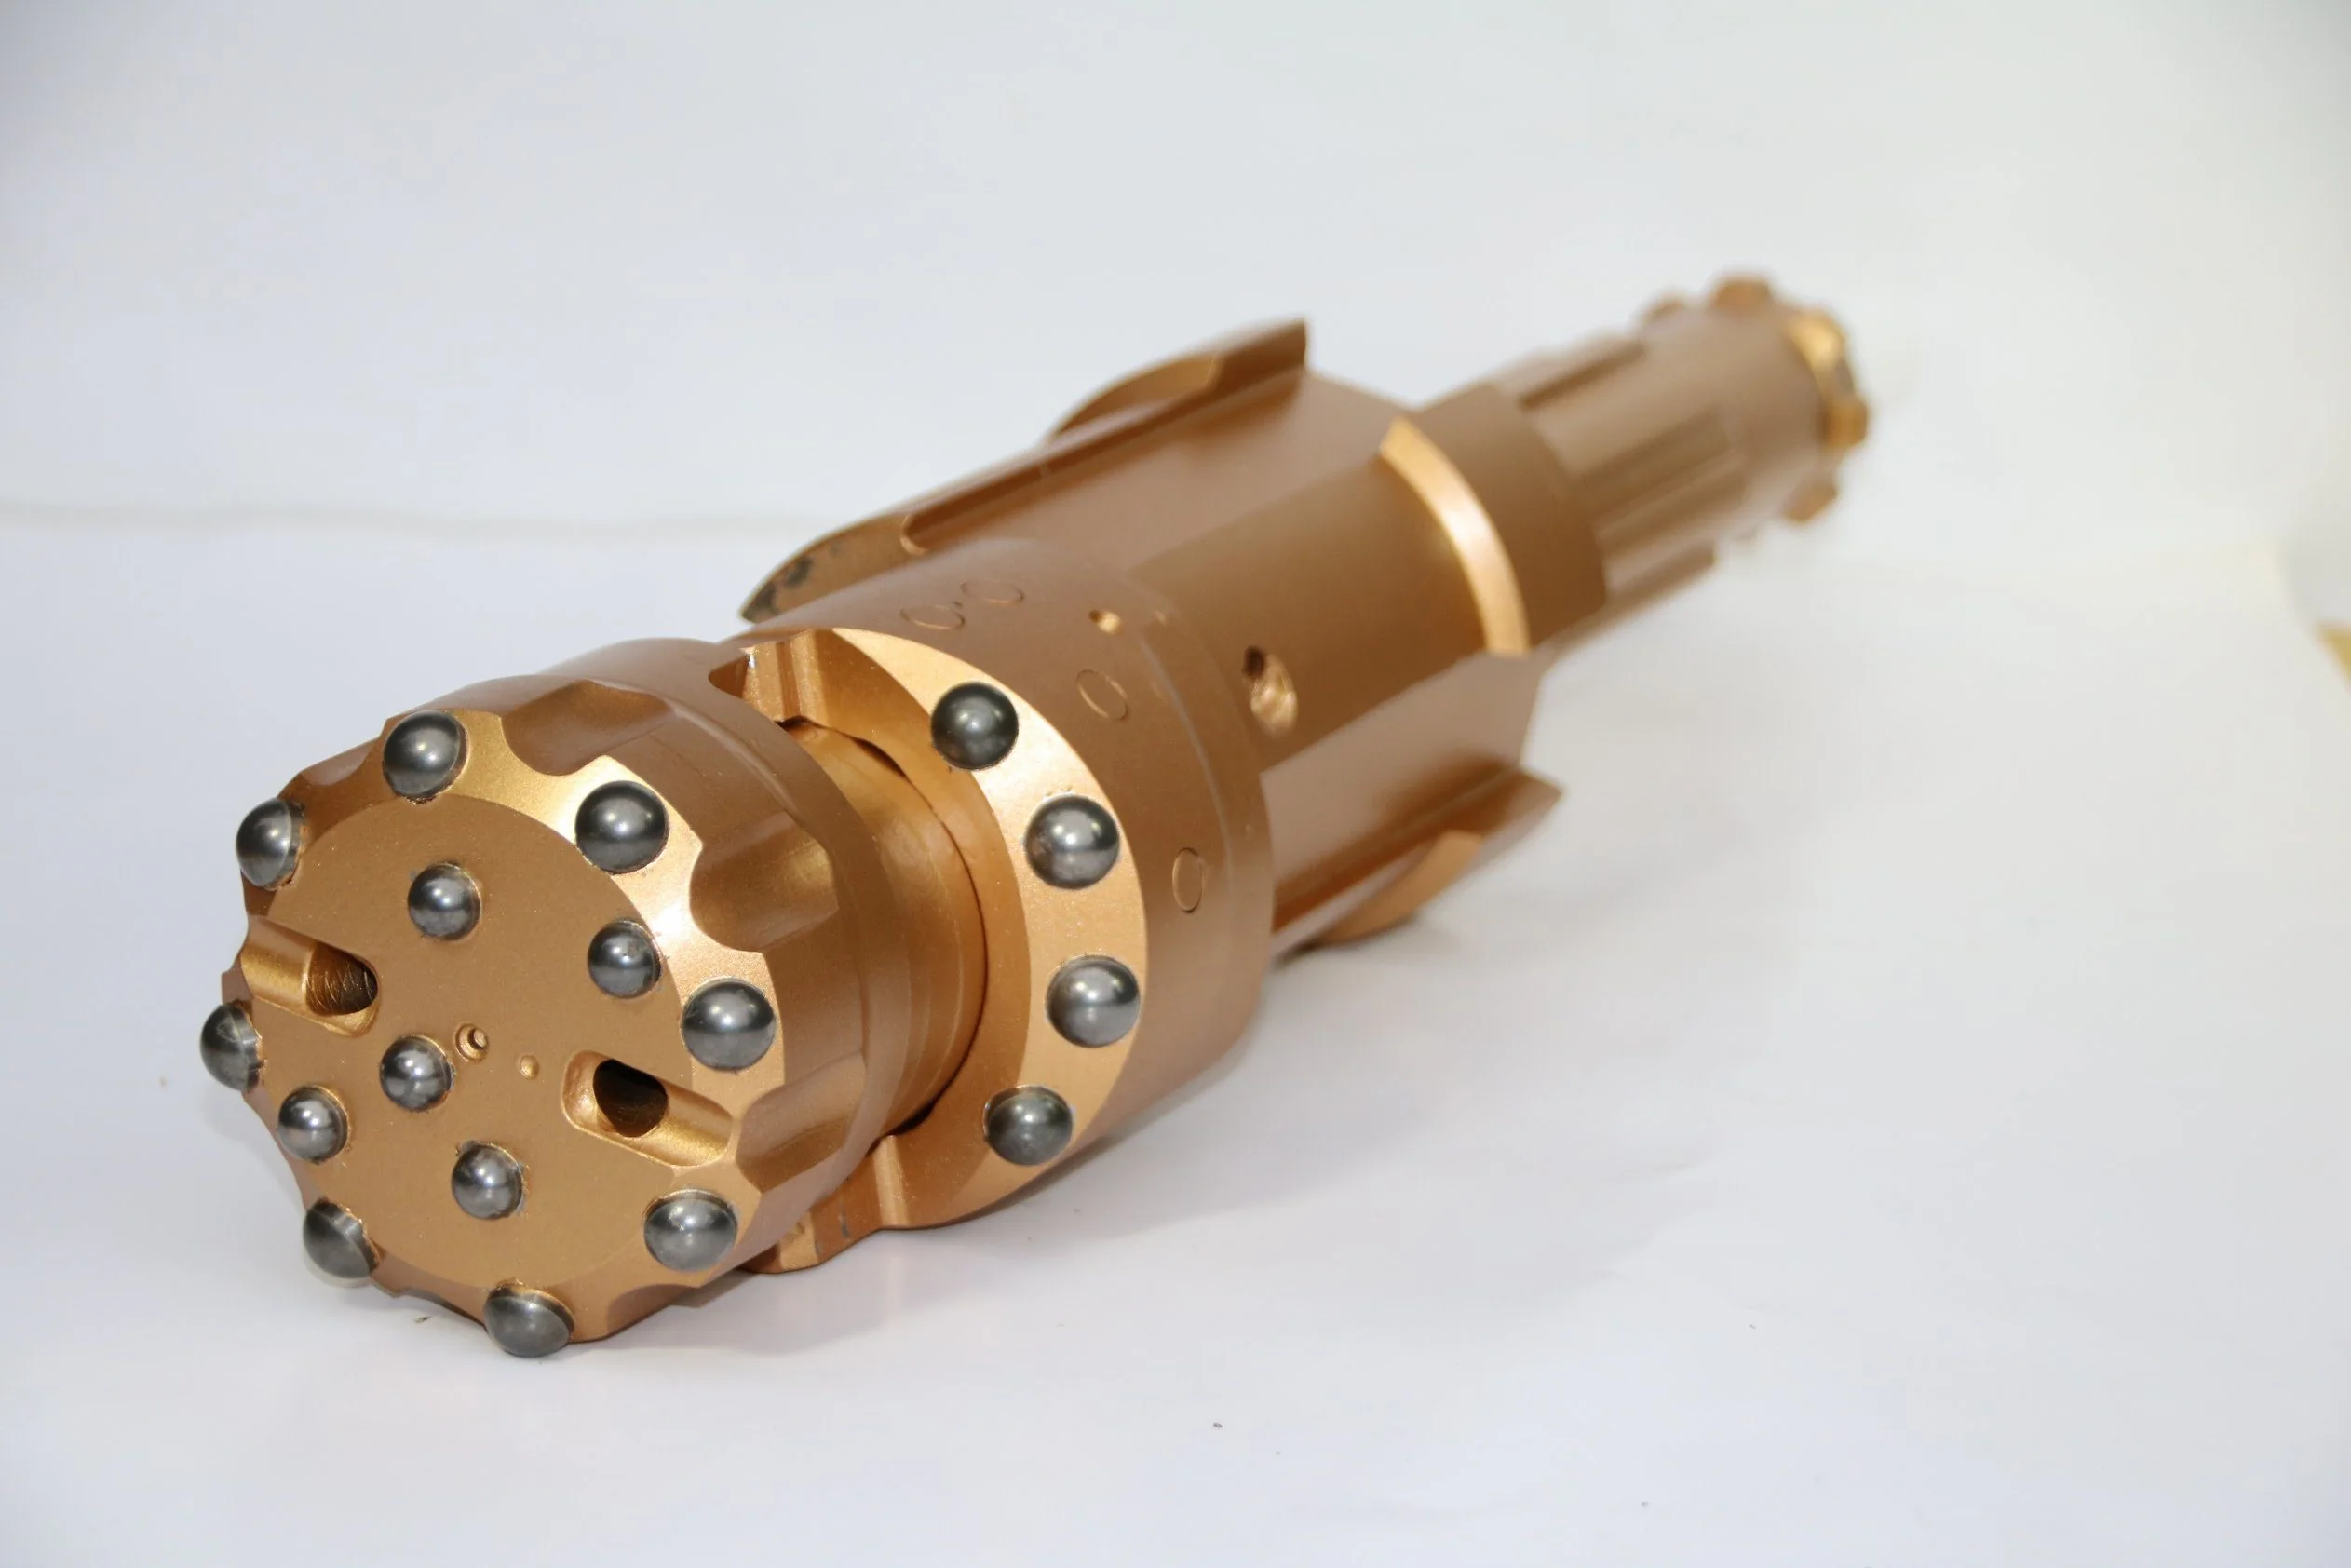
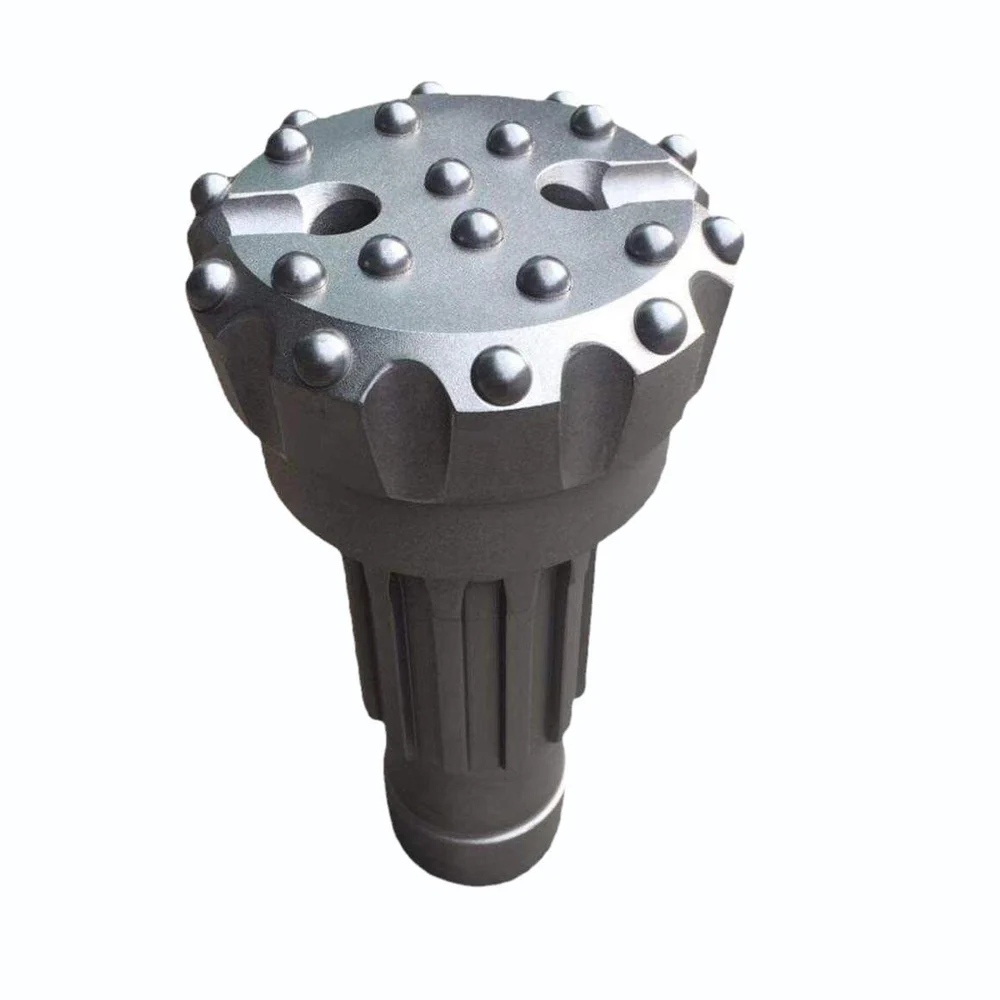
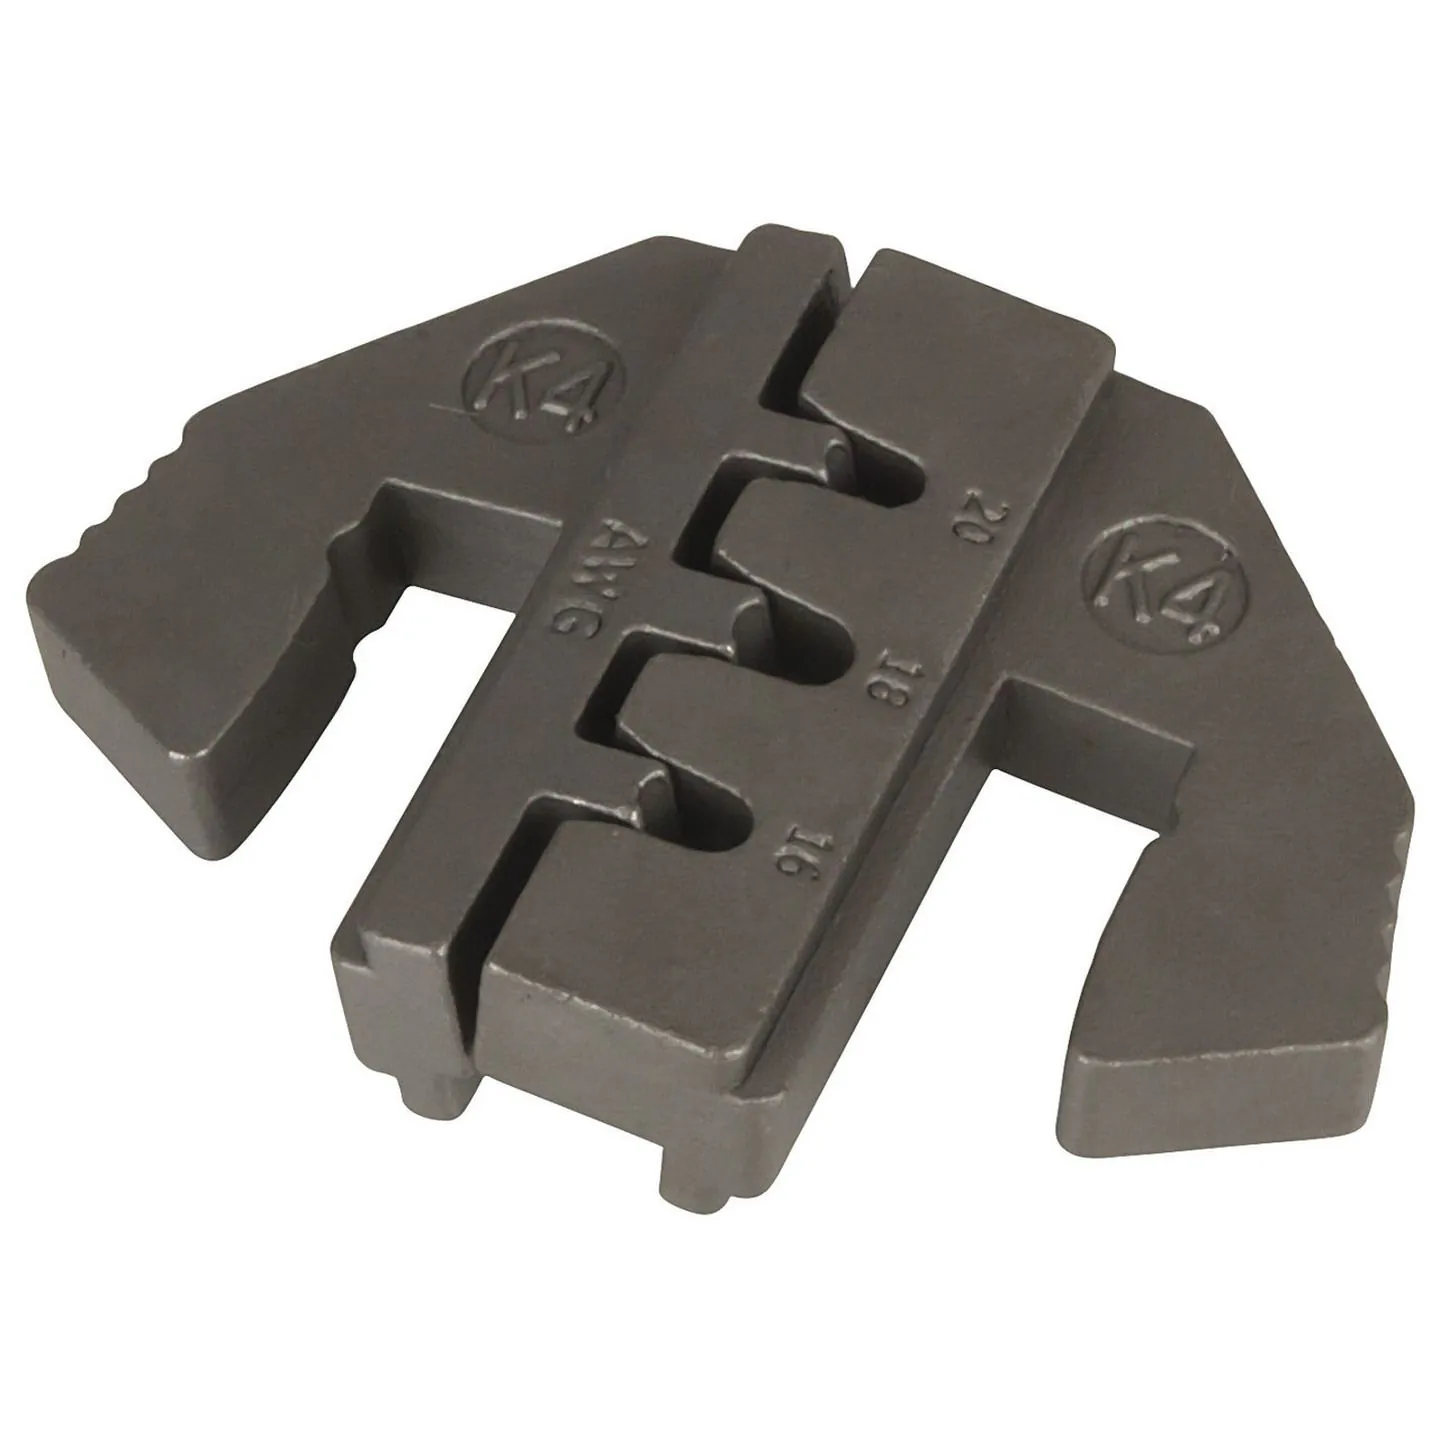
Finished Product Gallery

05 — Key Advantages

Why Choose the 1600-Ton Sinter Hydraulic Press

The 1600-Ton Sinter Hydraulic Press is an ideal solution for manufacturing Powder Metallurgy (PM) wear-resistant inserts and heavy-duty tooling components, delivering high compaction force for superior density, strength, and durability. Its precise hydraulic control ensures consistent quality, excellent dimensional accuracy, and reliable performance, making it well-suited for demanding industrial applications while reducing production costs and extending component life.

01

High Compaction Force

Delivers 1600 tons of pressing capacity, enabling the production of high-density PM components with superior mechanical strength and wear resistance.

02

Excellent Dimensional Accuracy

Ensures consistent part dimensions and tight tolerances, minimizing secondary machining and improving product quality.

03

Uniform Density Distribution

Advanced hydraulic control provides even compaction throughout the component, reducing defects and improving performance.

04

Enhanced Productivity

Supports large-volume production with stable operation, faster cycle times, and improved manufacturing efficiency.

05

Capability for Complex Components

Suitable for producing large, intricate, and heavy-duty tooling parts with reliable structural integrity.

06

Lower Manufacturing Costs

Reduces material waste, tooling wear, and rework requirements, resulting in lower overall production and maintenance costs.